Rubix in the UK is one of the most trusted single sources for industrial supplies and part of Europe’s largest industrial distribution business. Rubix works with a network of branches across the UK offering support 24 hours a day, 365 days a year.
A significant part of its business is involved in the supply of cutting tools and accessories for the engineering industry, representing several high-quality brands, some on an exclusive basis such as Cutline. Made to exact specifications, every tool in the Cutline range has been meticulously produced and tested, ensuring a high level of quality.
Testing, proving out and demonstrating are necessary services offered by Rubix Cutting & Machining, for which high performing machine tools are required. In selecting the right machine tool supplier for its needs, Rubix Cutting & Machining specified CNC vertical machining centres and lathes that could push the products it sells to the limits. At the same time, sufficient rigidity and accuracy were needed to get the best from the tooling.
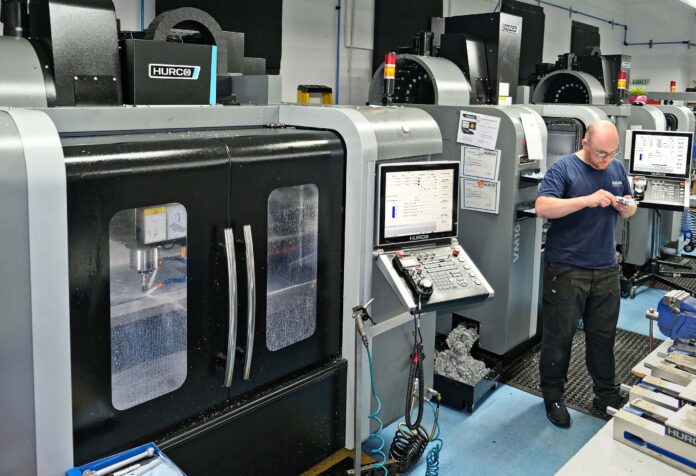
Hurco’s most popular 5 axis machining centre, the VMX42SRTi was chosen because of outstanding machine capacity compared to footprint size, along with its ability to work to the same standards for high-power 3 axis applications as for complex 5 axis 3D contouring. The VMX42SRTi has a 12,000 RPM, 37kW spindle and direct drives on all axes, plus a 40 station toolchanger as standard. Additionally, a TM8i CNC lathe with a bar capacity of 64.5mm and 12 station turret was chosen to demonstrate turning tools and workholding.
Both machines are placed at the Rubix Product Proving Technical Competence Centre Technical Centre in Wolverhampton. The Rubix Cutting & Machining nationwide engineered solutions team are all trained in the operation of Hurco machines and are competent with Hurco conversational programming after a couple of days in the Hurco classroom.
For more information, contact Hurco – Tel: (011) 012 259 1375
Installation of one Hurco vertical machining centre (VMC) per year between 2013 and 2017 plus the addition of a sixth in May 2021, partly to take advantage of the UK government’s 130% capital allowance, have coincided with a sustained improvement in the level of business at subcontract machining firm Kelvin Precision Products. Disregarding the first year, when the start-up firm’s income was relatively low and therefore unrepresentative, turnover has increased fivefold compared with the second year of trading.
Like many employees working at subcontracting firms, James Staniford dreamt of branching out on his own. After an eight-year stint at a company in nearby Horsham, he took the plunge in 2013 and started Kelvin Precision Products with Claire McGrath, now the Business Director, who invested capital and owned a suitable 4,000 sq ft unit within the Kelvin Business Centre in Crawley.
The enterprise had the help of his friend and mentor Alan Lamberth, who used his turning experience to help out at evenings and weekends. It boosted this side of the business at the time and allowed Kelvin to take on much more complex manual turning than would otherwise have been possible.
However it was prismatic machining that quickly took precedence and it now accounts for around 85% of turnover. An online auction on eBay secured the first contract to machine a range of small laboratory components from acetal and aluminium for a customer in the scientific industry, which was also a start-up. Soon afterwards a manufacturer of broadcasting equipment, another new company, discovered Kelvin via its website and placed an order for a range of milled components. Both companies are still regular customers, along with about a dozen others.
The contracts were fulfilled on a Hurco VM10 3-axis VMC, which was purchased new along with a manual lathe, a knee-type mill and a linisher when James started the business. A Hurco machine was chosen for the first major purchase due to the Windows-based conversational programming capability in the machine’s WinMax control.
James said, “At the outset we didn’t have a CAM system, so relied on WinMax and its menu-driven 3D graphics interface to prepare cycles for machining our customers’ components, some of which were quite complex.
“At that time, the other shortlisted machine had a G-code control and 2D graphics, so we regarded the Hurco offering as superior.
“As time went on and parts became even more complicated, we invested in Autodesk FeatureCAM Ultimate CAD/CAM software, but WinMax is quicker for programming simple components and we still use it about one-third of the time.”
Following the success of the first VMC, one year later another 3-axis machine was installed – a VM10i with more advanced control technology and diagnostics. Then the first 5-axis machine arrived, a VM10Ui, followed by a second in 2016. A larger VM20i 3-axis VMC with a 1,168 x 508 mm table was delivered a year later and then a third 5-axis VM10Ui in early 2021. Interspersed among these purchases were a sliding-head lathe in 2014 and a fixed-head lathe in 2018.
Having half of its prismatic metalcutting capacity able to produce components efficiently in fewer set-ups using three- plus two-axis cycles, with the rotary axes positioned and clamped, sets Kelvin apart from many of its competitors of similar size. It enables high quality work typically to tolerances of ± 0.05 mm to 0.10 mm to be turned around in short time scales. Normally, components are put on a 5-axis machine at Crawley for Op 1 and a 3-axis machine for Op 2 if it is relatively simple. Fully interpolative 5-axis milling and drilling on the Hurcos is available if suitable jobs come along.
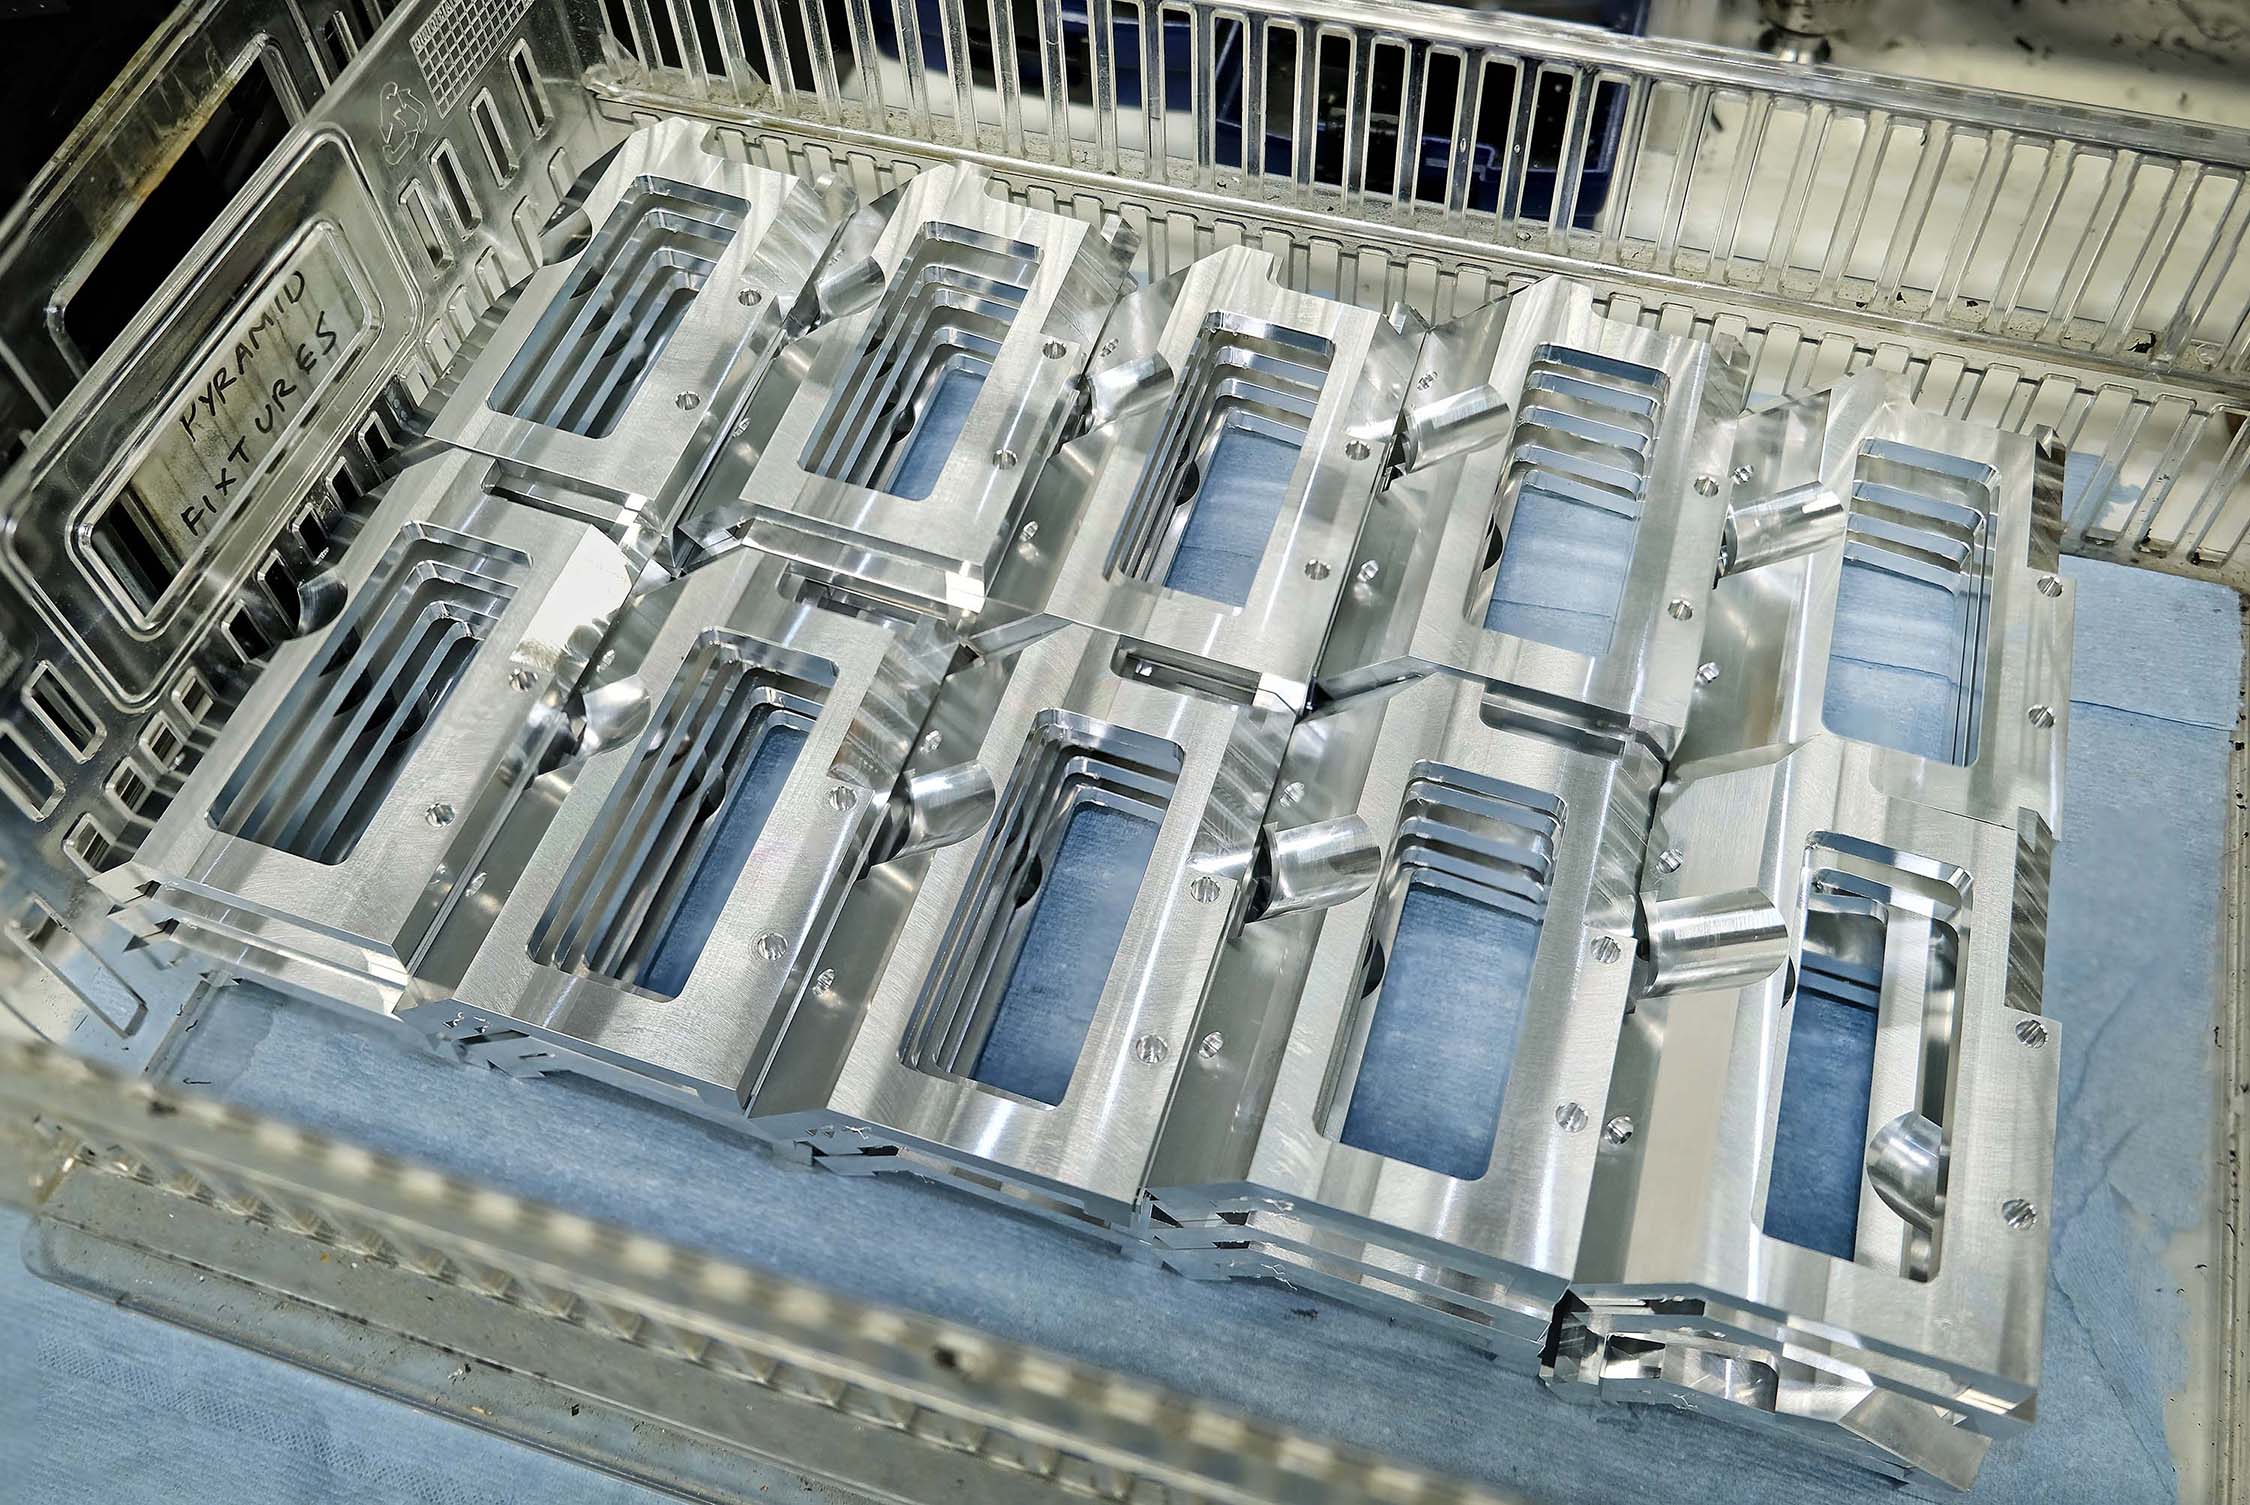
Aluminium base plate for a customer in the pharmaceutical industry
Based close to Gatwick airport, the subcontractor offers machining services with delivery to the south-east of England and to the rest of the UK and Europe via a mail order service, with customers emailing a drawing or CAD file. A regular part of the company’s activity is working for other contract machining firms that require more capacity to get an important job out on time.
Today, prismatic machining of a wide range of plastics and metals including stainless steel, mild steel, cast iron, aluminium, brass and copper are the mainstay of the company’s day-to-day work, some parts being over one metre in length. Sliding-and fixed-head turn-milling of components from 1 mm to 350 mm in diameter accounts for around 15% of turnover.
For more information, contact Hurco – Tel: (011) 012 259 1375
With the new Toplus premium chuck, Hainbuch always guarantees a runout of ≤ 5 μm without alignment.
With a new development in the hexagonal chuck series from Hainbuch, the clamping device manufacturer from Germany enters the next round. In 2006, the first Toplus chuck with hexagonal clamping geometry began its career. Just one year later, the Toplus IQ with integrated measuring technology followed, and in 2012, the mini version with a smaller interference contour and lower weight was born. Now Hainbuch presents its latest development. The highest precision Toplus premium chuck is available from stock and points with many additional advantages.
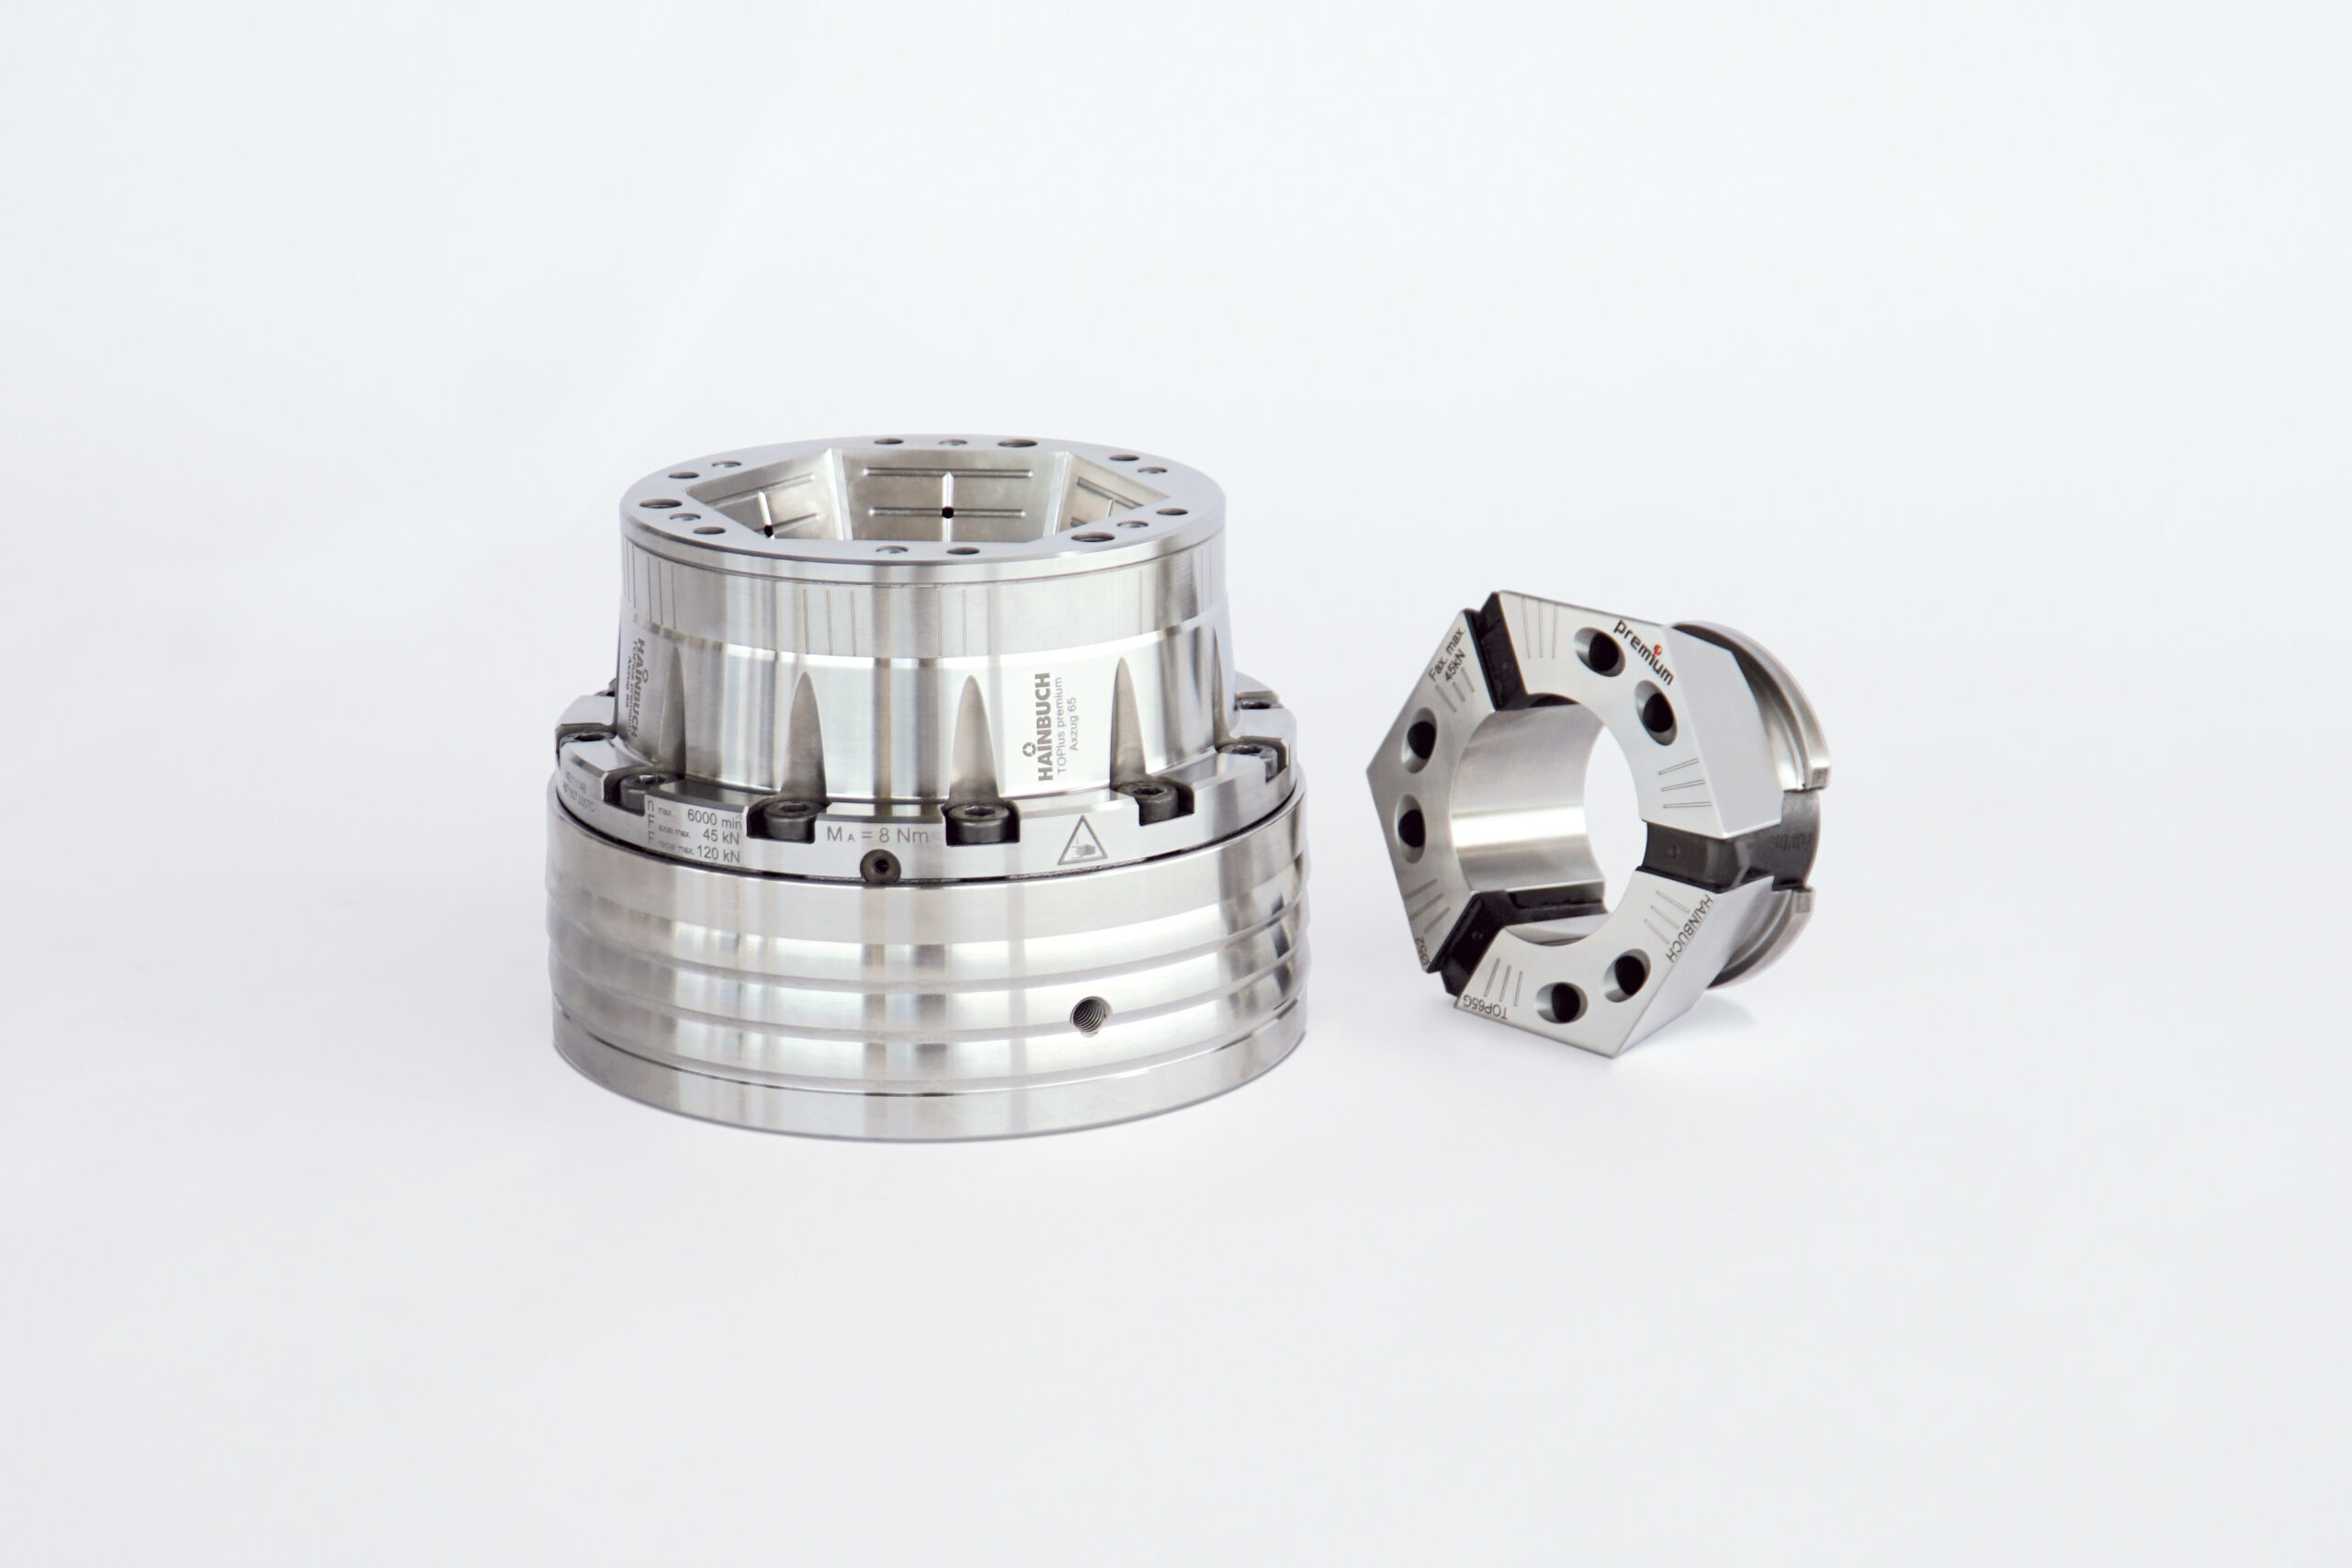
The ≤ 5 μm accurate Toplus premium chuck with premium clamping head.
Hainbuch’s chucks have always been very precise. Once the chucks are aligned, the runout is close to zero for repeat clamping. If the various chuck heads are then changed, the runout is usually between 3 to 7 μm without alignment. With the new Toplus premium chuck, Hainbuch always guarantees a runout of ≤ 5 μm without alignment – regardless of which clamping head is used. Until now, this was only possible with a high-priced hydraulic expansion or diaphragm chuck with the drawbacks entailed by their design. In many cases, a runout of ≤ 10 μm is perfectly sufficient. However, components or machining processes with a runout of ≤ 5 μm are increasingly becoming the standard. Using a Toplus premium chuck with the associated premium clamping heads and by clamping against the workpiece stop, this level of accuracy is always achieved. This means that manufacturers don´t lose time making alignments for small batch sizes and they can be highly flexible, because it is just as accurate as a chuck aligned for series production.
To save time and costs, a robot is often used to load the workpieces in the machine. This can become a problem if the clamping stroke is too small. With the Toplus premium chuck combined with a clamping head, the stroke is large enough, and makes loading easier, even if the robot works somewhat imprecisely. In addition, it is very robust and not as sensitive as some other clamping devices. A slight contact with the workpiece during loading has no effect on the chuck. The process remains stable. It is also sealed against contamination and vibration. With the Toplus premium, both thin-walled and solid parts are clamped securely with no centrifugal losses. And last but not least, the Toplus premium – like all chucks – is available in the Hainbuch system. This means that changing from external to internal or jaw clamping takes no more than two minutes.
For more information, please contact CNC Support – Cell: 083 627 8336.
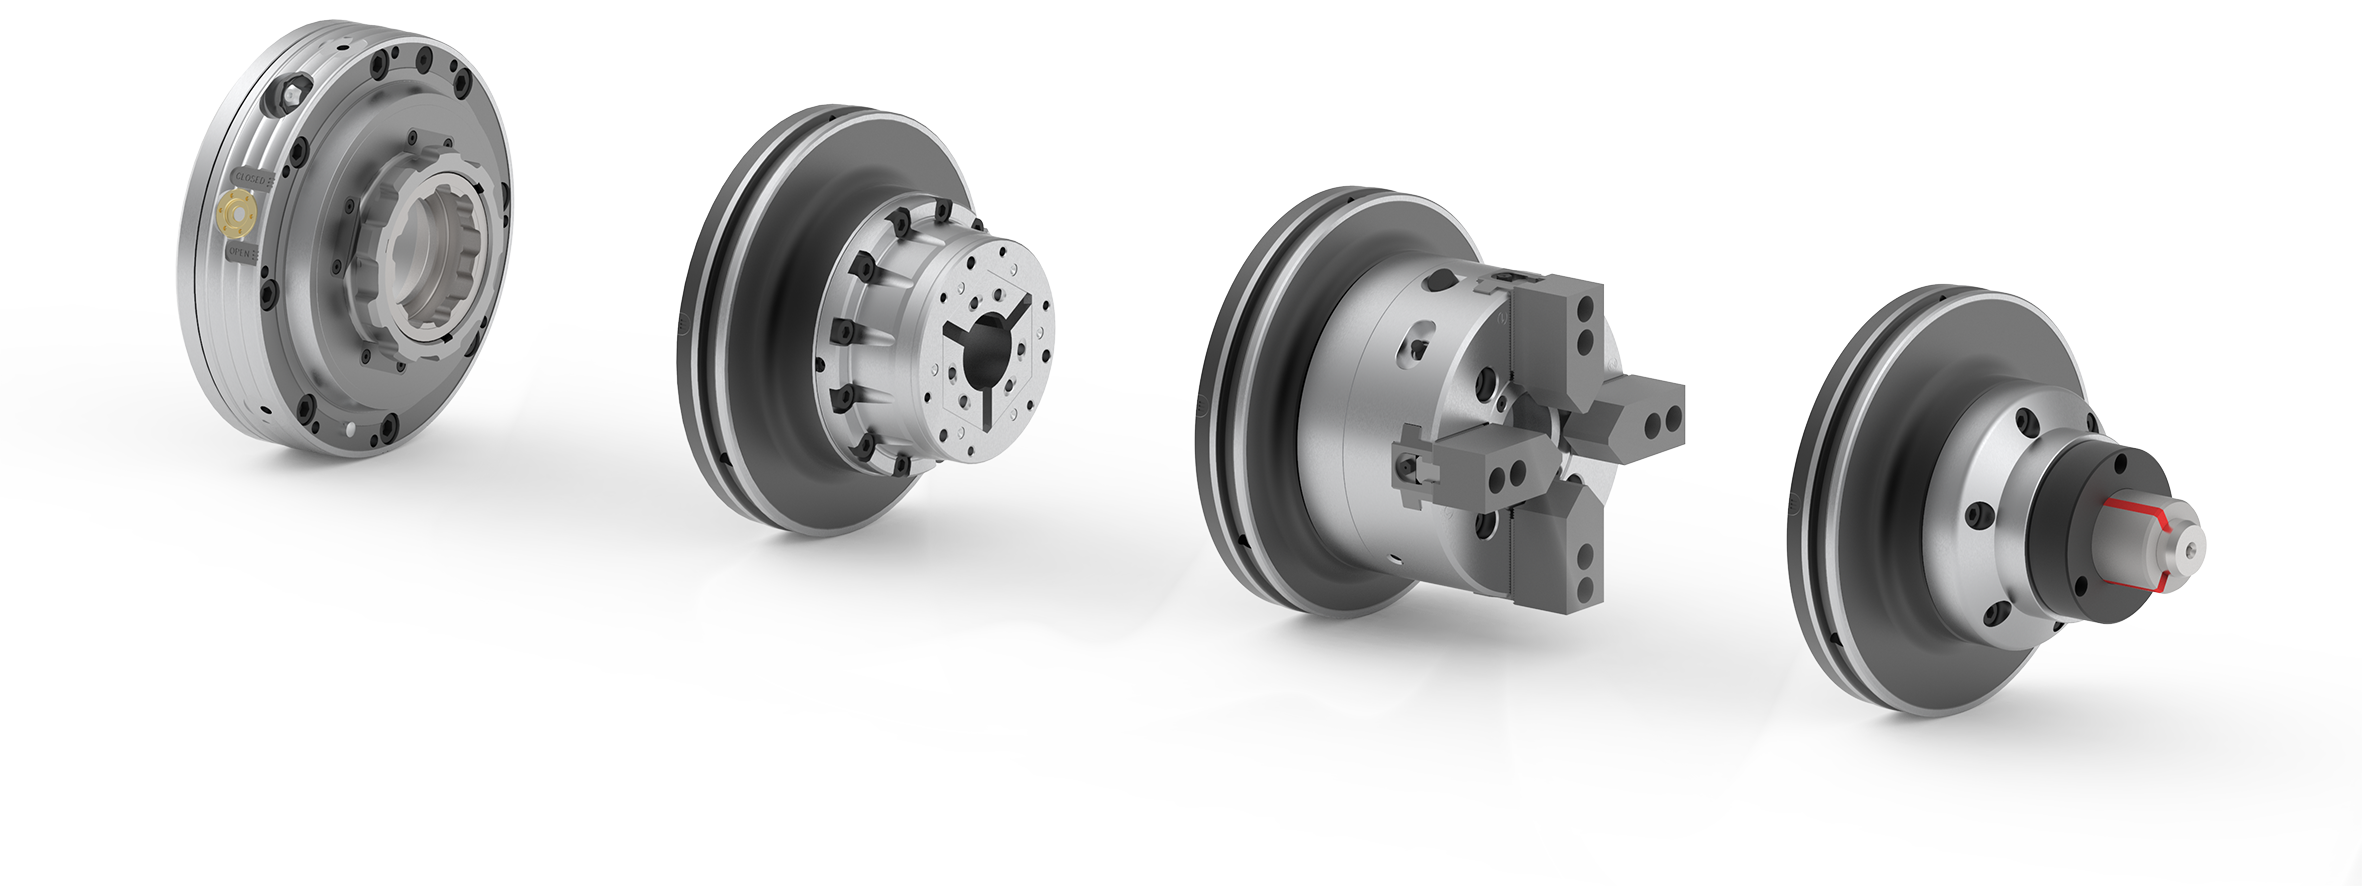
Hainbuch has set new standards with the Centrotex quick change-over interface. The proven system is now also available in a version for smaller spindles. Thus, today Centrotex S is the smallest system available on the market for setting up clamping devices in a matter of seconds. With its diameter of just 224 mm, it is the ideal quick change-over system for machines with a small work space.
Hainbuch Centrotex S
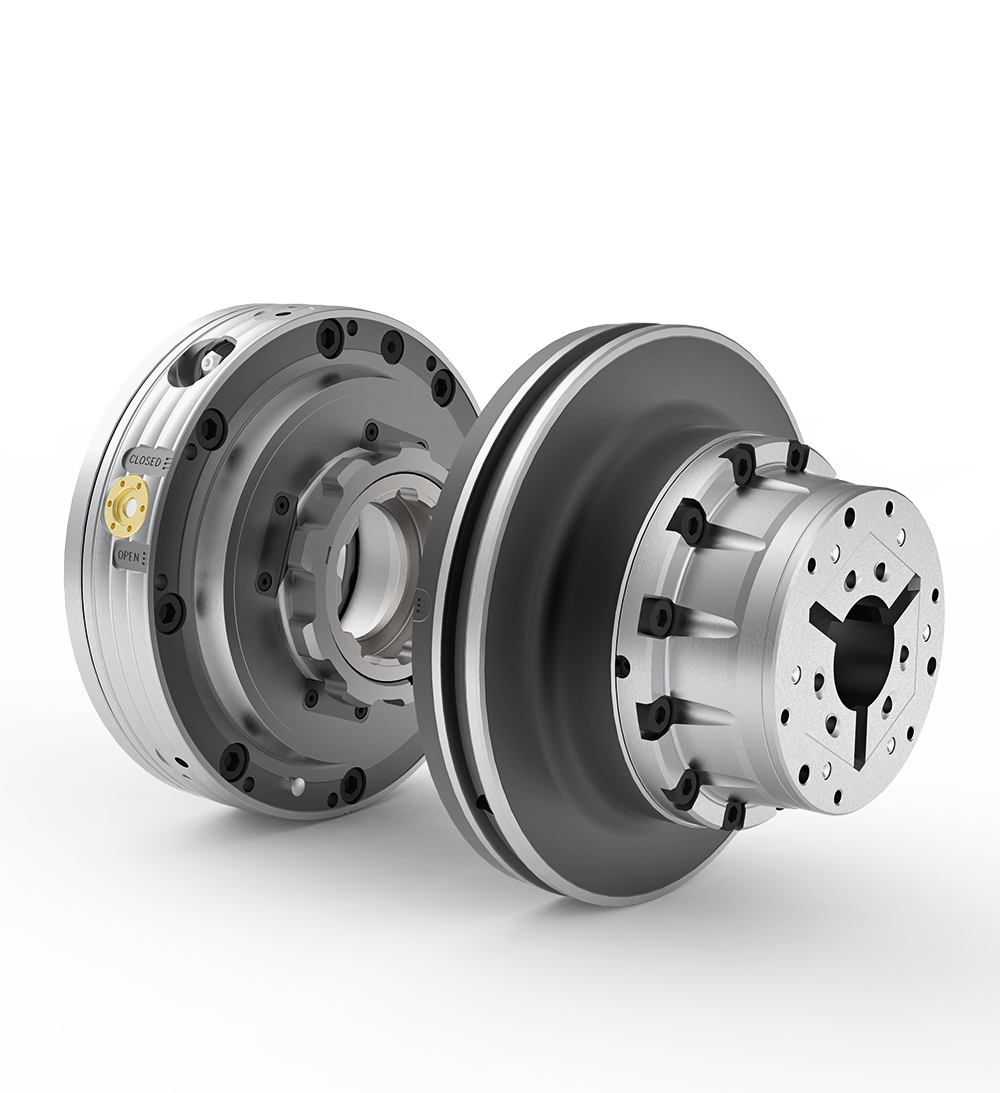
With repeatability to ≤ 0.003 mm on the interface – without having to align – the latest version of the Centrotex quick change-over system can also meet the most rigorous requirements. The machine adapter is mounted on the spindle, and the clamping device equipped with the adapter counterpart can be exchanged for another clamping device in less than a minute. Thus long set-up times are a thing of the past.
The smallest Centrotex version does indeed incorporate the proven technology of its big brother, however, it is clearly superior in terms of convenience. The Centrotex S is actuated via just one radial locking screw and ergonomic operation has been significantly improved, thanks to the fewer tightening turns required. In addition, the Monteq changing fixture offloads the machine operator and contributes to a faster clamping device set-up.
Key advantages include the interface between machine and clamping device, only one radial locking screw, while being suitable for spindle nose KK5, KK6, AP140, and AP170. Add to this repeatability to ≤ 0.003 mm on the interface – without having to align, ergonomic handling and resistance to contamination. For easier handling, the Monteq changing fixture can be implemented for heavy clamping devices
Machine adapter with different clamping device adapters. Quick change-over from OD clamping to jaw clamping or ID clamping.
For more information, please contact CNC Support – Cell: 083 627 8336.
Walter AG maximises process reliability and productivity with its new copy turning system
With the W1011-P, Walter is bringing a copy turning system to the market which will maximise process reliability and cost-efficiency compared to conventional systems. This is primarily thanks to its much greater stability when copy turning with relief grooves of up to 50°. Unlike VCMT and DCMT inserts, the system’s new three-edged WL25 indexable inserts are precisely secured in the toolholder by a prism in the insert seat and on the insert itself. This ensures that the insert cannot move in the toolholder. In addition to high process reliability and precision thanks to highly accurate indexing – both when turning the inserts to the next cutting edge and when replacing them – this provides over 50% greater accuracy when compared to ISO inserts. In addition, the system has an increased tool life thanks to the option to machine in both directions of movement, meaning that the two cutting edges can be used.
The copy turning system also uses WL25 indexable inserts, which further increases its cost-efficiency. Three cutting edges (rather than two cutting edges on VCMT inserts) with wear-resistant cutting tool materials in addition to precision cooling improve the tool life. The same also applies to the universal usability of the W1011-P system. Its four insert types (neutral, left-hand, right-hand and full-radius versions) for different profiling angles and applications fit into the same toolholder and mean that it can be used for all ISO materials (P, M, S and K). Potential areas of application include copy turning (for example, for drive shafts, ball bearings, valves, etc.) and dynamic turning – particularly for operations which use a different or alternating machining direction. This allows users to increase cost-efficiency by up to 75% in finishing up to medium machining operations.
For more information, please contact Spectra Carbide Tooling Technology – Tel: 021 555 4144.
Walter Tiger·tec® Gold grade with multi-layered, highly textured MT-TiCN coating
With the WPP10G, WPP20G and WPP30G grades, Walter presents the new Tiger·tec® Gold indexable inserts, specially designed for turning operations. The aim was to reduce flank face wear by 30 to 60%. In reality, the tool life increased by an average of 50% according to the results of over 130 customer tests. The primary application is steels with a tensile strength of 600 to 900 N/mm2. The lightweight components made of steels with a high tensile strength of 1000 to 1400 N/mm2, which are on trend at the moment, can also be machined with the new grade. The indexable inserts are sure to be of particular interest to mass producers in the automotive, energy and general mechanical engineering sectors, where the inserts significantly reduce the cost per component. Wherever a range of materials are used, such as in the mechanical engineering industry, users can benefit from their versatility: Walter is bringing the grades with nine geometries for optimised chip breaking on long-chipping, low-carbon materials (MP3) and for interrupted cuts (RP7) to the market.
Another key feature of the Tiger·tec® Gold inserts for turning is their outstanding process reliability. This, alongside their performance and tool life, is the result of their unique layer structure: A patent-pending, highly textured MT-TiCN layer reduces flank face wear and increases toughness due to its multi-layered structure, which optimises elasticity. The highly textured Al2O3 layer additionally increases the product’s resistance to crater wear. The gold-coloured top layer improves wear detection. The final multi-stage post-treatment of the inserts ensures a smooth rake face, less friction and high level of toughness. The individual alignment of the grades makes the indexable inserts outstandingly versatile: WPP10G for continuous cuts and light interrupted cuts, WPP20G as a universal grade for 50% of applications and the tough WPP30G grade interrupted cuts as well as unstable or unfavourable conditions.
For more information, please contact Spectra Carbide Tooling Technology – Tel: 021 555 4144.
Hyundai WIA, one of the largest machine tool makers in Korea, used its accumulated know-how and latest technology to develop the SE-SY Series, which delivers high-performance, high heavy cutting capability and maximum productivity.
Specializing in small-parts, the Y-axis CNC turning centre features a 30° slanted one-piece bed structure with high rigidity, while the stabilized unit structure is designed to minimize thermal displacement.
01 Optimal Structural Analysis
Structural analysis was applied when designing the machine enhancing the tool post body, while reducing the machine’s height in order to maintain the bed’s dynamic rigidity even during heavy-duty cutting.
02 High-speed Roller LM Guideway
Linear roller guideways are used in SE-SY Series reducing non-cutting time, while achieving high-rigidity. In order to eliminate thermal growth and increase accuracy, all axes are driven by high precision double anchored ballscrews. The rapid traverse rate for X/Y/Z/ZB is 30/10/36/15 m/ min with a travel distance of X/Y/Z/ZB of 210/110/560/560 mm.
03 Wedge Type Y-axis Structure
The SE-SY Series is designed with a wedge type Y-axis that is transferred by the simultaneous operation of the Ys-axis and the X-axis. In addition, excellent rigidity promotes superb quality when heavy-duty cutting. Y-axis rapids are 10 m/min with a Y-axis travel range of 110 (±55) mm.
04 High-precision main spindle for Heavy-duty Cutting and High Quality
The main spindle is designed with the same structure often found in larger sized machines. The combination of double cylindrical roller bearings and angular contact ball bearings leads to excellent heavy duty cutting performance.
05 Sub Spindle
The S-type sub spindle with 5″ chuck is designed to minimize thermal distortion caused by heavy cuts and highspeed machining.
For more information, contact Spectrum Africa – Tel: 011 865 4090.
The machining of long and several tons of heavy parts is particularly demanding when at the same time high precision and tightest tolerances are required. It is not only the technical competence of the machine operator that is important, the turning center must also be able to comply with the high demands of the machining process for large, accurate and heavy workpieces. In order to be able to produce even small and smallest batch sizes economically and precisely, Hyss Metallberarbeitung in Lennestadt, Germany, for many years has been counting on large turning centers from Hwacheon, a South Korean machine tool manufacturer.
Gerhard Hyss (right) and his son Steffen (left) invested in the extremely robust and precise turn-mill center Hi-TECH 850L YMCHyss Metallverarbeitung produces large and heavy turned parts in small batch sizes on its XL lathes
The contract manufacturer specializes in turning of large and heavy parts, up to 8 tons, 1,100 mm in diameter and 3,500 mm in length. These are often one-off productions or small series in small quantities.
While in 1982 Gerhard Hyss started his business with two partners and the production of small turned parts, they envisaged manufacturing larger parts and decided to invest in machines for processing maximum diameters of 550 mm and peak weights of 1.5 tons. “This allowed us to expand our range of services and gain new market segments,” explains Hyss.
“The concept worked, and more and more orders for large precision turned parts were received. Eventually, the previously available production area reached its capacity limits and subsequently a new production facility was built in 1999 at the current location. The new halls offered space for even larger machines and thus also for machining larger and heavier work-pieces.
FIRST LATHE FROM HWACHEON – Hi-TECH 700
With the rigid Hi-TECH 700 from Hwacheon, workpieces up to a diameter of 700 mm and a turning length of 2,000 mm can be processed.
At the Metav exhibition in Düsseldorf, Gerhard Hyss spotted the Hwacheon Hi-TECH 700, a horizontal turning center for heavy-duty machining, which offers an extremely rigid spindle design. The high-precision cylindrical roller bearings and the particularly impact-resistant angular roller bearings of the headstock are specially designed for tough and hard turning operations. Torques of up to 3,071 Nm at 115 rpm can be achieved via the integrated gearbox. Hyss was fascinated with this extremely stable and qualitatively well-processed lathe in XL format and decided to buy his first Korean machine: “With the Hi-TECH 700, new doors opened for us. Now we were able to machine parts up to a diameter of 700 mm and a turning length of 2,000 mm and achieve more flexibility and speed in production,“ he says.
With the new machine, more new orders came for even larger workpieces. The company had found its niche market and at the same time acquired a reputation as a specialist in the manufacture of large parts for the engineering industry. In the period that followed, the order backlog continued to grow, so another Hi-TECH 700 was purchased to adjust the production capacity.
NEW OPPORTUNITIES.
While space available for storing raw material was no longer sufficient, an additional hall was added. At the same time, the contract manufacturer received more and more inquiries for larger size turned parts with integrated milling work. Therefore, the procurement of a turning-milling center was planned
Steffen Hyss, son of the company founder and co-managing director, saw the Hi-TECH 850L YMC turning and milling center at the opening of the new Hwacheon European headquarters in Bochum. With this XXL machine, workpieces up to eight tons and diameters of up to 920 mm can be precisely machined up to a turning length of 3,500 mm. In addition to classic turning tasks, milling work can also be carried out in one setup in combination with an additional Y axis. This increases precision of machined parts, because clamping errors that can occur when changing from the turning to the milling machine are excluded. Hyss was so impressed with the Hi-TECH 850L YMC that the company decided to buy the machine.
EXTREMELY RIGID MACHINE BED AND FLAT GUIDE WAYS.
The spindle, tailstock and extremely rigid machine bed of the Hwacheon Hi-TECH 850L YMC are designed for large, heavy workpieces. The machine bed is bevelled by 45 degrees for optimal heat management. This prevents excessive heating of the workpiece and machine, while ensuring high precision.
The stable and robust machine has a particularly rigid monolithic machine bed with a weight of 23.5 tons, which is manufactured in Hwacheon’s own foundry. For optimal heat management, it is bevelled by 45 degrees so that hot chips can be reliably removed. This means that the machine and workpiece are not excessively heated, even during roughing operations with a large amount of chips. All flat guides of the machine are hand scraped and polished. Especially with this time-consuming work process, the manufacturer’s more than 75 years of mechanical engineering experience become clear. The flat guides have significantly lower vibrations even for heavy-duty machining tasks and thus ensure greater stability for greater precision and longer tool life.
Thanks to the massive design of the extra wide turret with a width of 250 mm, even large boring bars up to a diameter of 100 mm and a turning length of 1,000 mm can be clamped. The four-stage main spindle gear offers exceptionally high torque, especially in the lower speed range. The bearings are lubricated and cooled using the oil cooling system specially developed by Hwacheon. The temperature of the four-stage gear is continuously regulated in order to minimize thermal expansion, while ensuring accuracy during long operating times and heavy machining. With a drive power of 45 kW, the machine achieves a maximum torque of 6,873 Nm.
On the Hi-TECH 850, the company is able to machine all materials from structural steels, tempered steels, quenched and tempered steels, stainless steels, brass to plastics and super duplex steels.
For more information, contact Lead Machine Tools – Tel: 021 534-5351
By Paul Savides, Managing Director, PBS Machine Tools
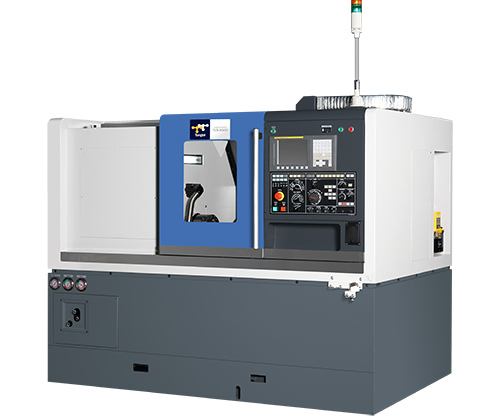
When a company makes a product like a CNC Lathe, that may be considered homogeneous i.e. with few differences from that of a competitor, it is very easy to offer some simple features or add-ons that give it a perception of value for money.
Adding value can be done in many ways but adding true Economic Value must be innovative. At Tongtai, we have spent many years improving our products so that we can match the high pace of today’s production requirements and at the same time meet the challenges of competitiveness that manufacturers face as they strive to survive.
The first step for Tongtai was to use available technology to keep costs contained and even use it to get prices marginally down without affecting quality. This has allowed us to keep the same reliability of our existing CNC lathe ranges that have been in 24/7 production in South Africa for more than 20 years. Enabling the upgraded ranges with technologies like Direct Torque Control have allowed Tongtai to improve the serviceability of all machines and at the same time, improve their overall efficiency resulting in major cost savings for the end-user.
This is done by extending tool life and reducing cycle time while at the same time maintaining accuracy of parts within very tight limits.
In a practical example at a user in South Africa we experienced the following:
Competitor
Part Cycle Time
Tool Wear
xxx
57 Sec/Pc
33 Parts/ Edge
Tongtai
19 Sec/Pc
100 Parts/Edge
This also means overtime and rework due to low output is avoided, eliminating late deliveries, unhappy customers and waste accordingly, driving down end-user costs.
Integrated Root Cause Analysis
To understand what a problem is, how to record it, how to analyse it, how to solve it and how to apply it, is truly what adding value really means.
The more refined machines become the more important it is for maintenance staff to keep them in production, this is why we have incorporated into the machines rudimentary systems that enhance end-user productivity and competitiveness. Enabling the many new technologies, developed by Tongtai, and incorporating them into our new machines takes care of all the SPC, Lean Six Sigma, Overall Equipment Effectiveness and Lean Manufacturing processes.
This is all achieved through a range of Intelligent Sensors and Software developed by Tongtai including:
Vibration sensors
Machine levelling sensors
Pressure sensors
Temperature sensors
Current sensors
Intelligent tool holders
Tool wear monitoring
Real-time cutting monitoring
RFID reader for tool identification
Integrated communication channel linking all sensors to an Industrial PC
By capturing and interpreting these parameters, we can check and diagnose the condition against the known machine and cutting tool characteristics to ensure the machine continues to produce and keep its quality of performance.
All this helps with process optimisation, improves machine operational performance and reduces unexpected or unplanned machine stoppages.
For more information please contact PBS Machine Tools – Tel: 011 914-3360.
With rising energy costs and strict international environmental laws, equipment efficiency is a key factor that can influence the production costs. By this trend, the latest machine tools not only need to satisfy the requirements of high speed and high precision, but also need to pursue the goals of high efficiency and environmental protection. In recent years, Tongtai has worked hard on developing products which are environmentally friendly. Furthermore, energy saving accessory products are a primary concern to this manufacturer.
Rigidity is better than the past
All components are made of high quality cast-iron, while due to its excellent design, the structure decreases the influences of distortion and vibration. In addition, by applying Finite Element Analysis (FEA) the structure is optimized satisfying the requirements of high dynamic rigidity and stability.
Inheriting the outstanding machine rigidity from TB series, the TD series is the brand new multi-tasking turning center with single power turret which is standard equipped with 12 tool stations and linear Y axis to process milling functions. In addition, the 16 tool stations turret and sub-spindle are also available for more complex machining processes, while helping to reduce labour costs and increasing floor utility.
Spindle/Sub-spindle CS axis with brake unit
The CS axis is fed back by a rotary encoder with multi-points positioning function. The minimum indexing increment of 0.001 degrees allows various machining needs with different angles.
With synchronous temperature control, the spindle cooler prevents sub-spindle from thermal distortion. This ensures high precision machining for long-term operation.
75 degree machine bed structure
Different from the 90 degree slant bed on TB series, the TD series features a 75 degree slant bed design. It not only keeps the advantages of excellent chip disposal and accessibility, but also lowers the machine’s gravity center, while enhancing the entire structure rigidity.
Linear Y axis structure
The TD series features a symmetrical saddle design, while the X/Y/Z axes are perpendicular to each other with a real linear Y axis. It allows servo compensation on each axis to optimize the positioning accuracy.
Different from the virtual Y axis, the real Y axis has excellent straightness and positioning accuracy which is able to ensure high machining quality. With a highly rigid sliding carrier design, the TD series has outstanding machining capability.
For more information please contact PBS Machine Tools – Tel: 011 914-3360.







 Linear roller guideways are used in SE-SY Series reducing non-cutting time, while achieving high-rigidity. In order to eliminate thermal growth and increase accuracy, all axes are driven by high precision double anchored ballscrews. The rapid traverse rate for X/Y/Z/ZB is 30/10/36/15 m/ min with a travel distance of X/Y/Z/ZB of 210/110/560/560 mm.
 The SE-SY Series is designed with a wedge type Y-axis that is transferred by the simultaneous operation of the Ys-axis and the X-axis. In addition, excellent rigidity promotes superb quality when heavy-duty cutting. Y-axis rapids are 10 m/min with a Y-axis travel range of 110 (±55) mm.
 The main spindle is designed with the same structure often found in larger sized machines. The combination of double cylindrical roller bearings and angular contact ball bearings leads to excellent heavy duty cutting performance.
 The S-type sub spindle with 5″ chuck is designed to minimize thermal distortion caused by heavy cuts and highspeed machining.