Home Blog

POWER UNDER PRESSURE – CUTTING COSTS IN SOUTH AFRICAN MACHINING

Across South Africa’s manufacturing sector, the pressure to produce more for less has never been greater. Rising electricity costs, volatile exchange rates and increasing global competition are forcing machine shops to focus on what truly drives profitability – efficiency at every level of production.

In this reality, success is no longer defined by output alone, but by how quickly and consistently that output is achieved. Every second of cycle time, every insert edge and every machine stop has a cost attached to it.

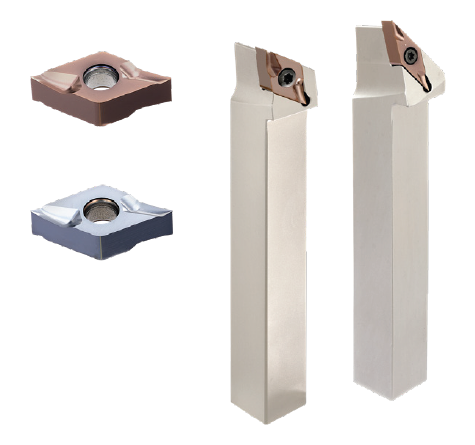
TaeguTec’s turning and grooving portfolio – RHINO-TURN, RHINO-M-TURN, RHINO-X-TURN, CUT-SFEED, RHINO-GROOVE and WIN-CUT – is designed precisely for this environment. The objective is simple, measurable gains in performance that deliver tangible cost savings.

Where Performance Meets Profit

On the shop floor, two metrics define operational success, cycle time and tool life. Reduce the first, extend the second and cost per component drops almost immediately.

TaeguTec’s solutions consistently push both in the right direction. Faster machining reduces energy consumption per part, an increasingly important factor locally, while longer tool life cuts down on insert spending and machine interruptions. The result is not incremental improvement, but a meaningful shift in productivity.

Built for Demanding Conditions

Heavy-duty applications remain central to South African industry, particularly in mining and energy. RHINO-TURN thrives in these conditions, offering the strength and stability required for aggressive cutting, while delivering excellent dimensional accuracy in a highly cost-effective solution. By enabling higher feed rates without sacrificing reliability, it shortens machining cycles, while extending tool life, two gains that directly reduce operating costs.

For workshops managing mixed materials, RHINO-M-TURN simplifies operations. Its versatility eliminates the need for constant tooling changes, keeping production flowing and reducing inefficiencies that quietly erode margins. With double the cutting edges for internal machining, it delivers stable performance and extended tool life.

When speed becomes the priority, RHINO-X-TURN delivers. Designed for high-speed applications, it allows manufacturers to increase output without compromising surface finish or stability. Its innovative 2-in-1 design combines roughing (CNMG) and finishing (DNMG) in a single insert, reducing machining time through high-feed machining. In an environment where energy costs continue to rise, faster cycles translate directly into lower cost per part.

Eliminating Weak Points in the Process

Parting and grooving are often where productivity is lost. Instability, tool breakage and scrap can disrupt even the most efficient operations.

CUT-SFEED addresses this with a stronger, more stable parting solution, featuring a robust clamping structure and a higher-rigidity insert for parting and deep grooving. This enables deeper cuts and smoother chip evacuation, resulting in a more reliable process with fewer interruptions and significantly improved tool life.

Similarly, RHINO-GROOVE enhances consistency in grooving applications. Its stability reduces vibration and ensures precise results, limiting rework and protecting valuable material, an essential advantage when raw material costs are high.

Efficiency without Excess Cost

Not every job requires premium tooling but every job demands efficiency. WIN-CUT provides a practical balance, offering reliable performance at a competitive cost. Featuring reinforced triangular blades, it ensures stable parting and deep grooving with low vibration, while maximizing productivity through high-feed machining. For general turning applications, it delivers steady improvements in both cycle time and tool life, helping manufacturers stay cost-competitive without over-investing.

A Practical Approach to Cost Reduction

What makes these solutions particularly relevant is how directly they respond to local challenges. Less machining time means reduced strain from high electricity tariffs. Longer tool life lowers exposure to exchange rate fluctuations. Increased throughput improves competitiveness in both domestic and export markets.

Individually, each improvement is valuable. Together, they create a clear and measurable reduction in cost per component.

Your Partner in Cost Reduction

In today’s manufacturing environment, efficiency is not an advantage, it is a requirement. TaeguTec’s turning solutions provide a focused, performance-driven approach to achieving it – faster cycles, longer tool life, lower costs. Not as promises, but as measurable outcomes on the shop floor with TaeguTec , your Partner in Cost Reduction.

For more information, please contact TaeguTec – Tel: 011 362-1500.

Visit TaeguTec

CUTTING CIRCLES FOR MILLING SLOTS


Modern Indexable Disc-Type Cutters and Exchangeable Heads for Efficient Slot and Groove Milling


“A circle is a round straight line with a hole in the middle” – Mark Twain

Disc type side and face milling cutters, often called slotting cutters and known as side mills in shop terminology, have long been an effective solution for slot and groove milling.

Compared with smaller diameter solid endmills, which are also used successfully for slotting operations, side and face cutters generally have a substantially larger diameter and can accommodate a greater number of cutting teeth. Consequently, even if the feed per tooth must be reduced somewhat, their higher tooth-pass frequency can permit a considerably higher table feed and metal-removal rate (MRR).

In the machining of deep slots and grooves, side and face cutters can also offer greater rigidity than long, small diameter end mills. This is another important factor in improving cutting efficiency and process reliability.

The effective cutting width of a side and face cutter determines the width of the slot. Therefore, a full-width slot can often be produced in a single pass.

Side and face cutters are available in non-indexable and indexable versions. In the latter, worn cutting edges can be renewed by indexing or replacing the inserts rather than by replacing the entire tool. Compared with solid carbide end mills, this can reduce tooling costs, particularly when carbide prices are high.

The principal advantages of side and face cutters are therefore high efficiency full-width slot milling, effective machining of deep and narrow slots, and, where indexable versions are used, the economic benefits of the exchangeable insert concept.

At the same time, the use of side and face cutters for milling slots and grooves involves several specific challenges.

In side and face milling cutters, teeth are provided on one or both side faces (“sides”) and on the outer periphery (“outer face”). Unlike cylindrical (plain) milling cutters, which remove material primarily with their peripheral teeth, side and face cutters combine peripheral cutting for producing the slot bottom with side cutting for forming one or both slot walls.

The cutting conditions of the peripheral and side teeth are not identical and their chip thicknesses and effective cutting speeds may differ. This can lead to unequal tooth loading and non-uniform wear of the cutting edges.

The peripheral teeth generate most of the tangential and radial cutting forces, while the side teeth produce axial forces. When teeth on both sides are engaged, the axial forces may partly oppose one another, however, they are not always balanced. The resulting cutting force distribution can deflect the cutter and shift the cutter laterally, causing it to be drawn toward one of the slot walls.

Side and face cutters are very sensitive to runout, especially in axial direction. Axial runout leads to unequal loading of the side teeth, may induce vibration and reduces tool life. Radial runout also contributes to irregular loading of the peripheral teeth. Together, these effects lower milling performance, worsen surface quality and diminish the dimensional accuracy of the machined slot.

Moreover, the tooth corners simultaneously participate in machining the slot bottom and walls. They therefore experience considerably higher mechanical and thermal loads than other parts of the cutting edge. These corners often become the cutter’s weakest points, its “Achilles’ heel,” limiting the cutting parameters. Chip evacuation is also difficult, especially in deep, narrow slots, where chips may be recut or may clog the cutting zone.

A similar situation is observed with slitting cutters (slitting saws) disc type milling cutters used for parting workpieces. These tools are typically made as thin as possible to produce narrow kerfs and, consequently, minimize material loss during slitting operations. However, this reduced thickness also lowers cutter rigidity. During parting, particularly of large workpieces, the tool remains engaged with the material for an extended period, which increases heat generation and makes chip evacuation more difficult, thereby accelerating tool wear. Insufficient coolant delivery further worsens these effects.

T-slot and angle cutters can, to some extent, be regarded as derivatives of side and face mills. In addition to the difficulties discussed above, the critical structural feature of a T-slot cutter is its neck, which largely determines the cutter’s relatively low rigidity. In angle cutters, particularly dovetail designs, the inclined geometry of the peripheral teeth increases radial loads, reducing both static and dynamic stiffness.

The need to overcome the identified limitations and improve the performance of slotting and slitting operations defines the main directions in the development of side and face milling cutters. Among the traditional approaches are the use of advanced cutting material grades and coating technologies, optimization of tooth geometry, improved dimensional accuracy and appropriate design of the chip spaces between the teeth to ensure efficient, unobstructed chip flow. In addition, manufacturers seek to increase tooth density, maximize service life and vibration resistance and provide effective coolant delivery.

In indexable milling cutter designs, particular emphasis is placed on the rigidity of insert clamping, economical use of cutting materials, especially tungsten carbide, rake-face geometry and internal coolant supply through the cutter body.

Over recent years, ISCAR’s range of side and face milling cutters has been expanded through the introduction of new products and the upgrading of existing designs. One of the examples is HELISLOT, a family of indexable slotting cutters that use cost effective, double sided square inserts with eight cutting edges – four right-hand and four left-hand. In addition to the existing 09 and 13 insert sizes, the range was expanded several years ago with the smaller 06 size for machining slots and grooves as narrow as 7 mm (0.275 in.). Subsequently, the insert portfolio has been supplemented with inserts specifically designed for machining aluminium and non-ferrous metals (ISO N application group). Compatible with the existing cutters, these inserts are available in all three sizes and feature ground insert side surfaces and polished rake faces to promote chip flow and eliminate the formation of built-up edge (BUE).
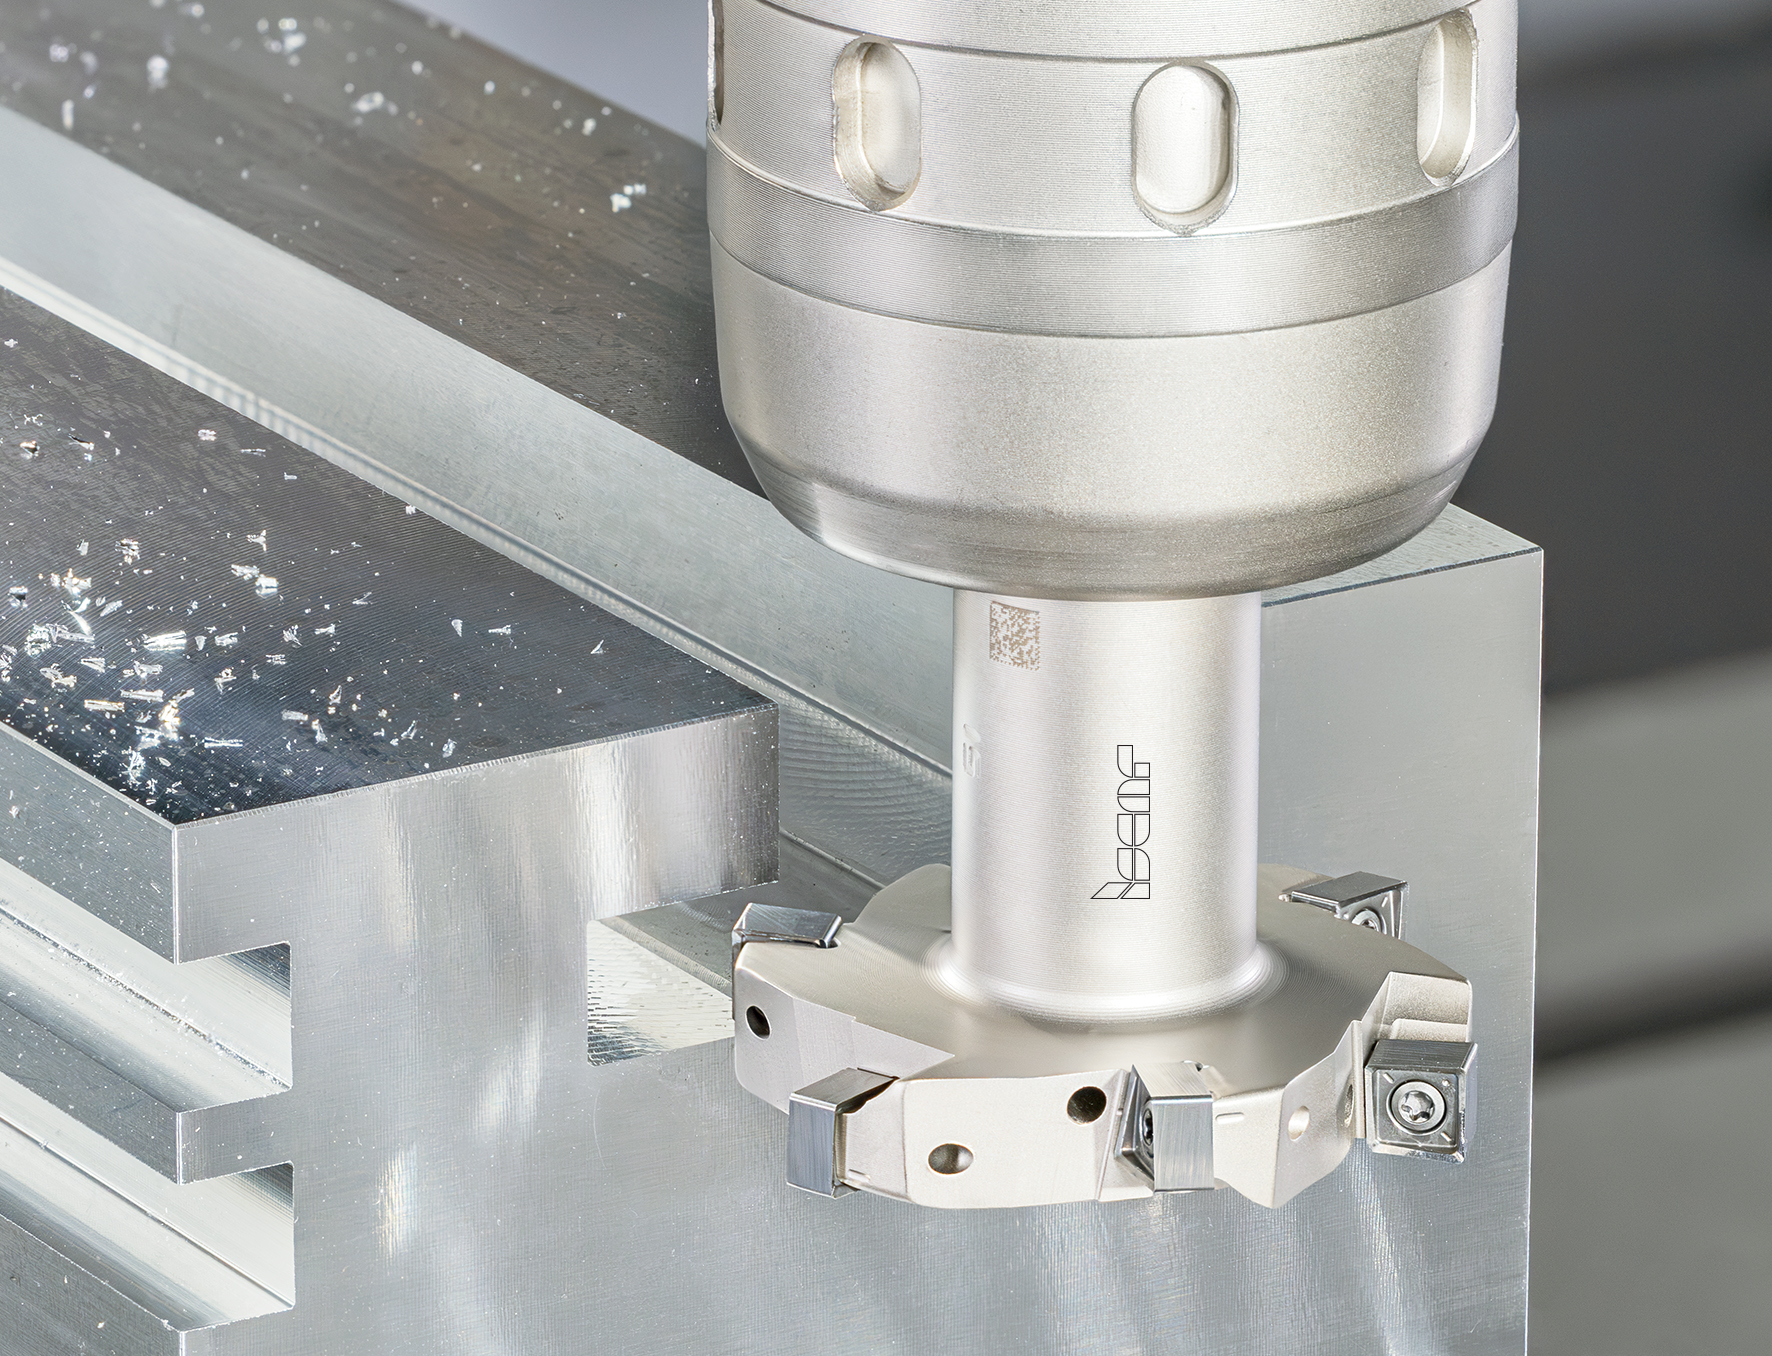

TANGSLOT is ISCAR’s well proven family of indexable slotting cutters, which employs a tangential insert concept. Cost effective TANGSLOT inserts provide four cutting edges and feature a unique rake face geometry that improves chip formation, reducing cutting forces and power consumption. Building on this development, the company has significantly expanded the range of insert corner radii to meet the requirements of slot milling applications.
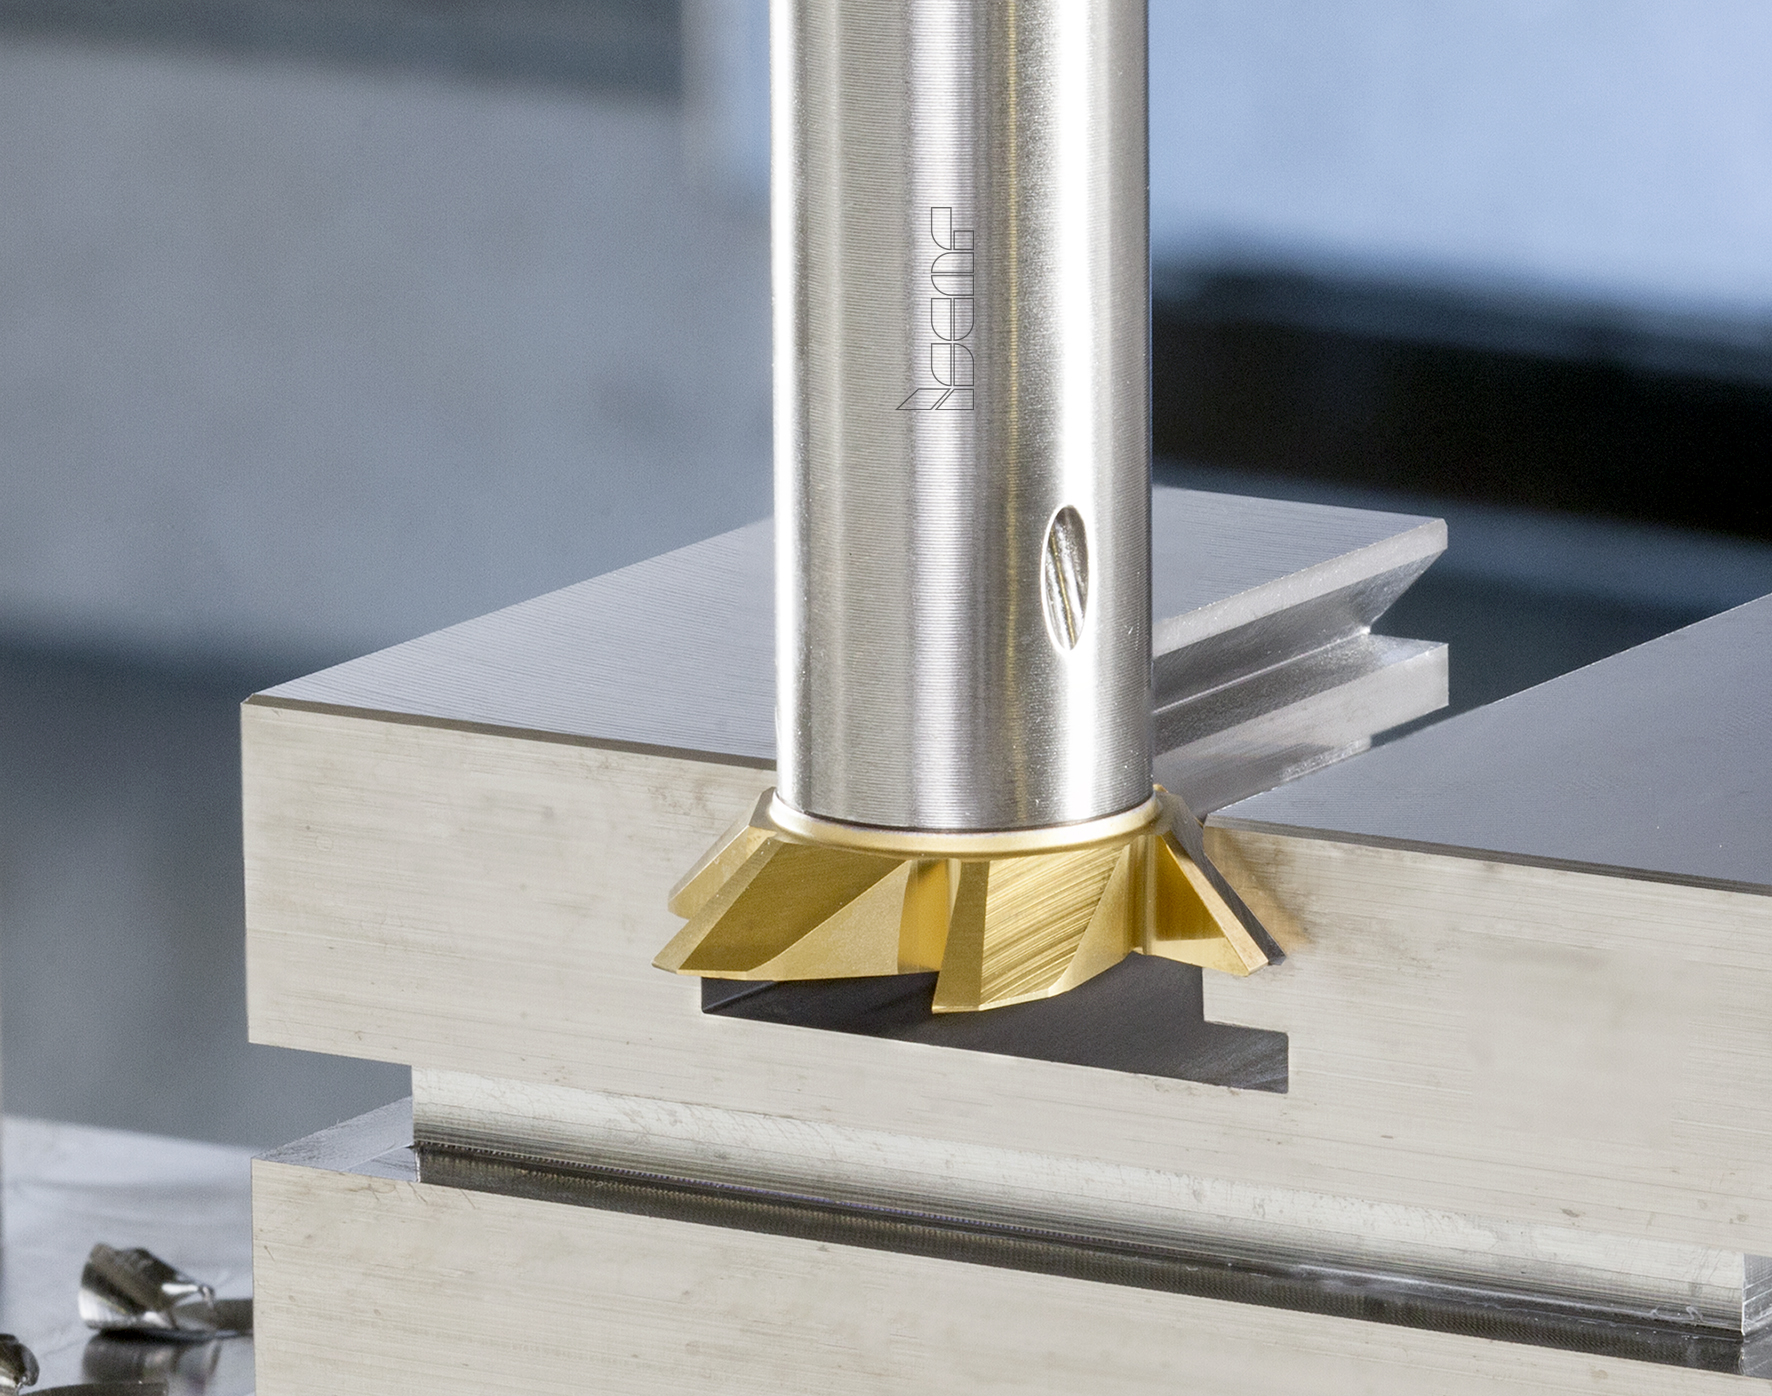

MULTI-MASTER is a versatile family of cutters with exchangeable heads and a true all-around solution for machining with relatively small diameter rotating tools has added new solid carbide dovetail milling heads in diameters ranging from 10.5 to 25 mm (0.413 to 0.984 in.). These precise multi-flute heads have six teeth, enabling higher feed rates and improved productivity. They are designed for milling dovetail slots with included angles of 90° and 120°, mainly in steel, stainless steel and cast-iron workpieces (ISO P, M and K application groups). The heads can also be used for back chamfering and deburring.

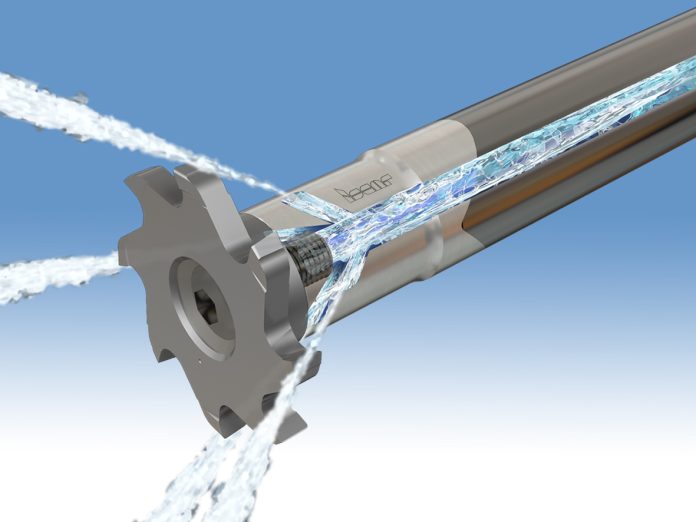
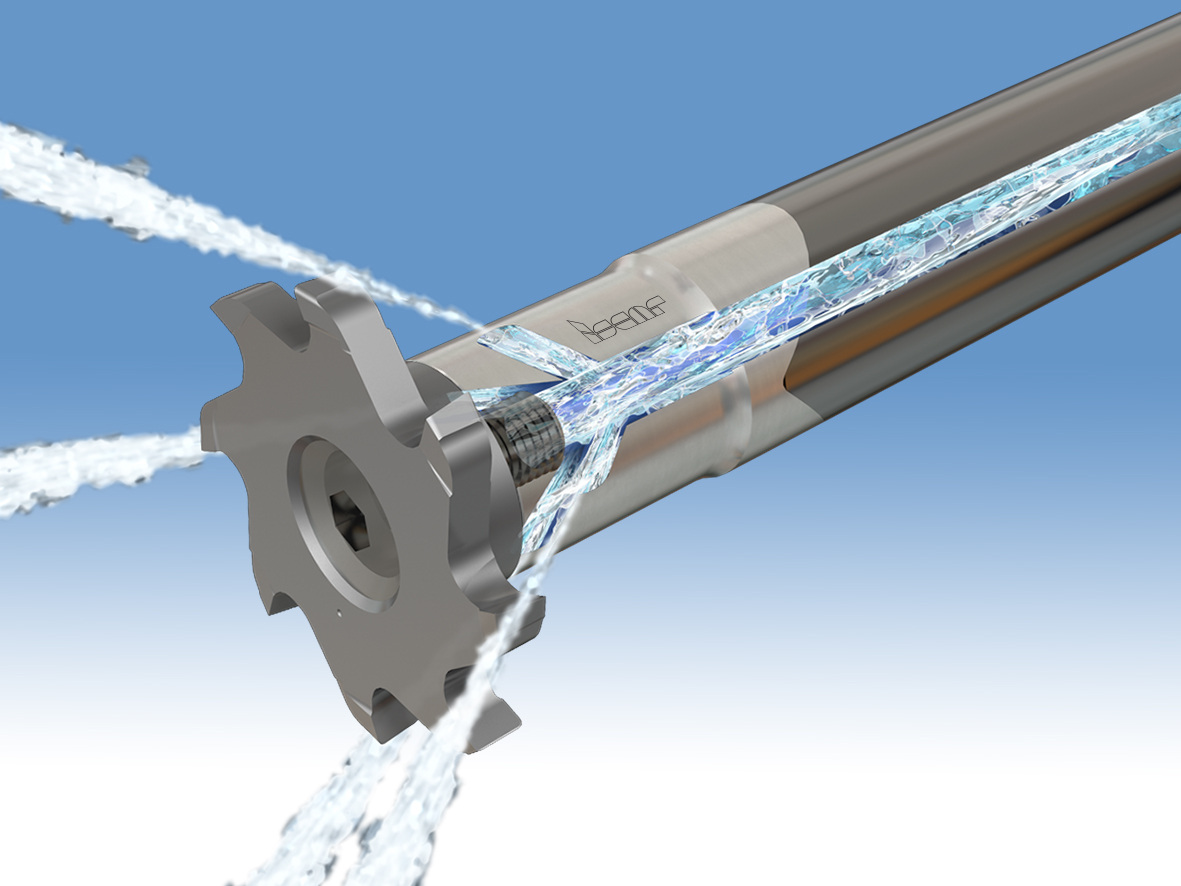
Another ISCAR system of assembled tools with exchangeable solid carbide milling heads is T-SLOT. In this system, the milling head is accurately centred by a cylindrical locating surface and secured with a screw, while torque is transmitted from the tool body to the head through a specially designed spline connection. Recently, carbide tool bodies (shanks) with an internal coolant option have been added to the range. A central coolant channel branches to each flute of the milling head, delivering coolant directly to the cutting zone. This arrangement improves cooling and chip evacuation and can significantly extend tool life.

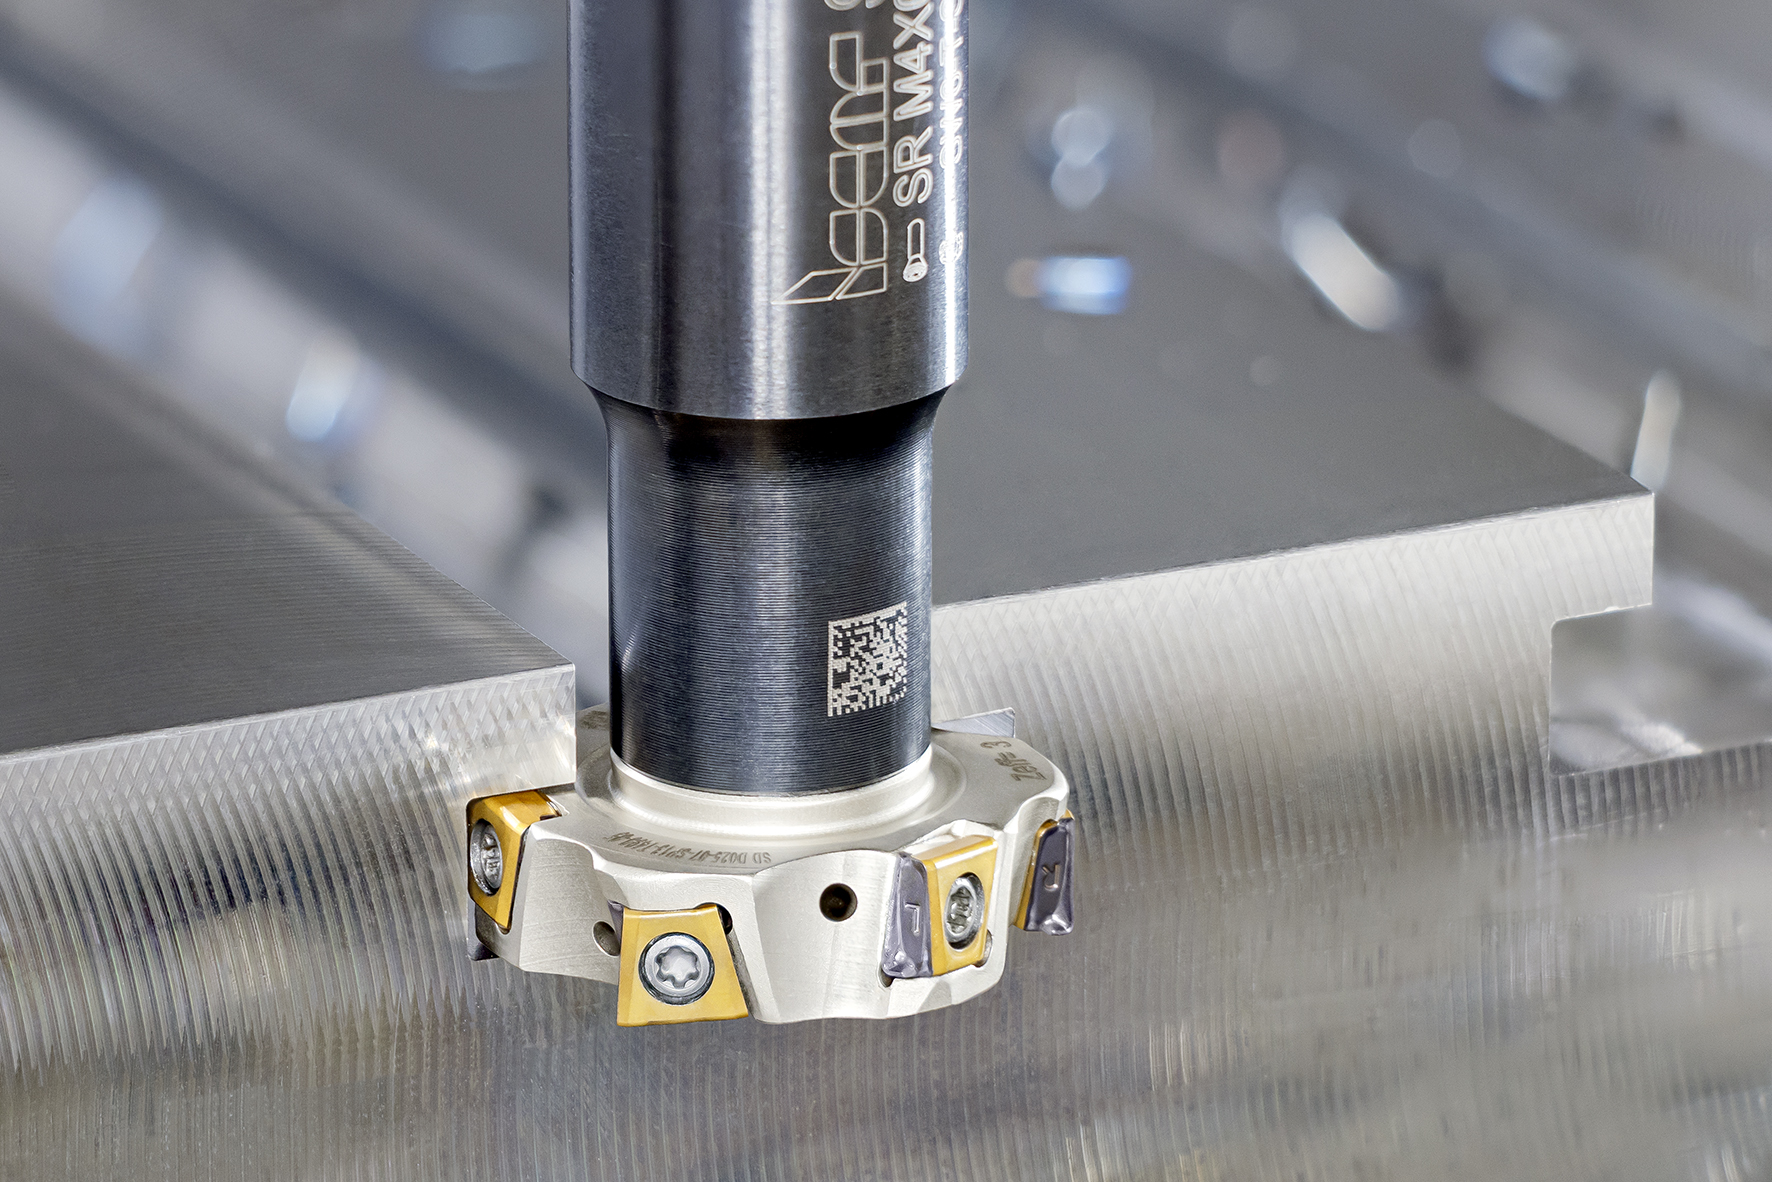
The robust spline connection concept used in T-SLOT, which enables the assembly to withstand the substantial loads and bending forces encountered in slot milling, has subsequently been extended to indexable tooling. TANG-DISC, a new family of assembled cutters, applies this principle to an indexable design. Its exchangeable heads carry compact, tangentially mounted inserts with a 5 mm (0.197 in.) inscribed circle diameter. Each insert provides four cutting edges, two right-hand and two left-hand. The new tools offer particularly effective performance in the machining of small industrial components and, through their economical miniature indexable insert approach, provide a practical means of reducing machining costs.

The continued development of slotting cutters demonstrates that productive slot and groove milling depends on more than increasing cutting speed or feed rate. Cutter rigidity, balanced cutting forces, reliable insert clamping, effective chip evacuation and precisely directed coolant supply are equally important. By combining these features with economical indexable and exchangeable-head concepts, modern side and face cutters enable manufacturers to machine slots, grooves, dovetails and perform parting operations with greater productivity, process reliability and cost efficiency.

For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997 2700.
Visit ISCAR

CRYSTA-Apex V – A PROVEN TRACK RECORD AND RELIABILITY COMBINED WITH SMART FACTORY FUNCTIONALITIES


Focused on Accuracy, Speed and Versatility


Proud to present our CRYSTA-Apex V Series, we deliver faster measurements without compromising the measuring machine’s inherent accuracy. It also supports the measurement of workpieces of many different shapes, such as castings or impellers.

High-speed optimal path scanning

The V Series is equipped with a measurement feature that allows users to specify scanning measurement paths (design values). This feature allows for high-speed, high-accuracy scanning by correcting dynamic errors that would otherwise be produced by acceleration and deceleration stresses. Measurement paths can be freely specified for three-dimensional forms as well, which enables intricate workpieces to be measured by tracking precisely along their curved surfaces and contours.

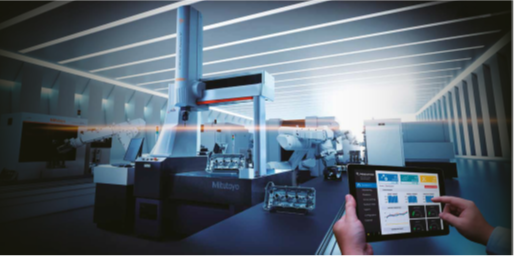
The CRYSTA-Apex V Series is a generation of CNC coordinate measuring machines that utilize IoT for the advanced management of production and quality information, making any factory, a smart factory.

From small to mid-sized workpieces, the CRYSTA-Apex V line-up covers it all and is available in many different sizes. The advances in accuracy, speed and versatility really shine through. With a chassis featuring bold colours, the design conveys cutting-edge capabilities and creativity befitting a precision measuring instrument of the IoT age.

The series provides accuracy that is unmatched by any previous general-purpose measuring machine, including real-time temperature compensation, high accuracy of 1.7 μm, repetitive accuracy and rapid measurement regardless of shape; add to this high-speed optimal path scanning, active scanning and a huge line-up of CMM probes, including scanning and non-contact probes.

For more information, please contact RGC Engineering – Tel: 011 887-0800.

Visit RGC Engineering

THE EVOLUTION OF AMADA BANDSAWS & BLADES

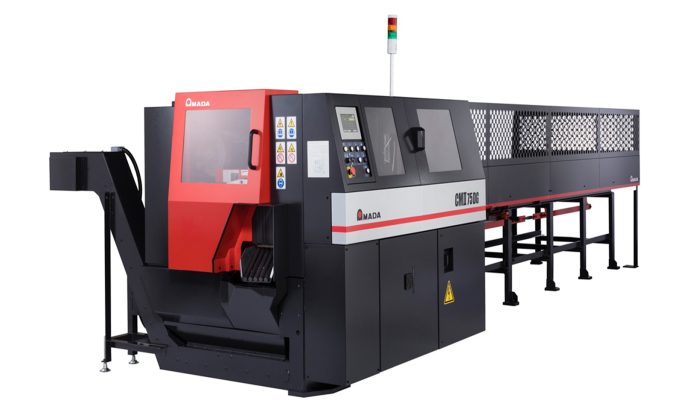
CMII 75-100 DG

By Donovan Hoole, Amada (UK) JHB Branch, Sales Engineer

The story of Amada bandsaw machines and blades is unique because Amada is one of the very few global manufacturers that design and produce both, the sawing machines and the blades themselves, ensuring perfect engineering synchronicity. This dual focus transforms their equipment from standalone industrial tools into highly optimized, harmonic cutting systems.

The Genesis of a Dual Approach

Decades ago, Amada recognized a critical limitation in the metalworking industry; a bandsaw machine is only as good as the blade being used. Instead of relying on third-party blade manufacturers, the Japanese engineering giant decided to develop its own metallurgy and tooth profiles. By matching the physical dynamics of the machine with the exact metallurgical properties of the blade, they unlocked unprecedented cutting speeds, precision and blade longevity.

The Evolution of the Machines

Amada’s machine line-up evolved from rugged, manual workshop saws into highly automated, CNC-controlled production workhorses.

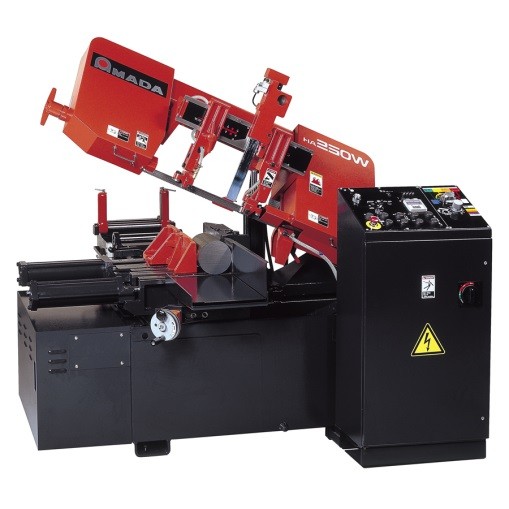
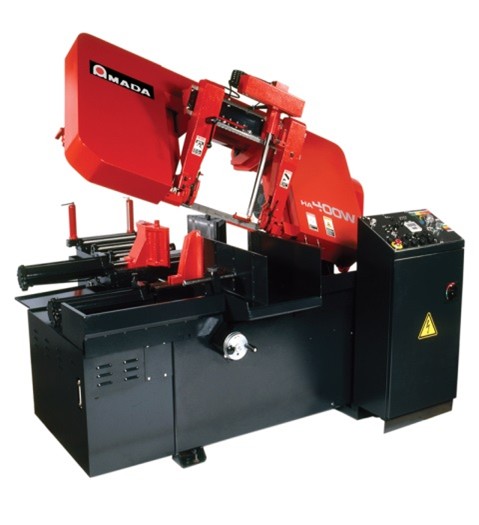
  • The HA Series Legacy: Models like the legendary Amada HA 250/HFA 400W Bandsaws became a standard fixture in manufacturing plants worldwide. Known for its fully automatic hydraulic operation and PLC controls, it allowed operators to program exact cut counts for continuous, unattended execution.
HA 250
HFA 400W
  • Pulse Cutting Innovation: To defeat the friction and resistance of cutting tough alloys, Amada introduced pulse cutting technology. These machines apply tiny, high-frequency vibrations to the blade as it cuts. This breakthrough dramatically reduces cutting resistance and prevents the blade from binding or wandering. All PC Saws are operated through the on-board operator friendly CNC control, while the models in the range are the PCSAW 330, PCSAW 430, PCSAW 530 and the PCSAW 720.


The Science of the Blades
While the machine provides the brute strength and rigid frame, the Amada blade is the high-tech edge that meets the metal. Manufactured to strict quality standards in Japan using advanced Electron Beam Welding, Amada blades are built for extreme durability.

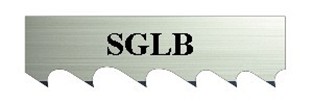
  • Bi-Metal Blades (SGLB & Protector): Built with high-speed M-42 steel teeth, these general-purpose workhorses cut through structural steel and varied shapes without stripping teeth.
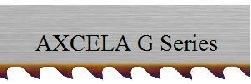
  • Carbide-Tipped Blades (Axcela Series): For difficult-to-cut metals like titanium, Inconel and large steel billets, the Axcela G and H Series utilize carbide tips. They deliver ultra-fast cutting speeds and perfectly straight finishes where standard blades would dull or warp.
  • Material-Specific Innovations: Expanding beyond metals, Amada now produces specialized diamond-tipped blades, designed specifically to cut delicate and abrasive materials like glass, silicon and ceramics.

BANDSAW BLADES

The Industry Benchmark
Today, the synergy of an Amada machine paired with an Amada blade remains an industry benchmark. By controlling both sides of the cutting equation, the company ensures that the blade vibration is suppressed, skew cuts are eliminated and industrial shops achieve the lowest possible cost-per-cut.

Amada SGLB – High Production M-42 Bi-Metal Blade for Metal Cutting Band Saw.


If you are researching this for a specific application, please tell me:

  • What specific materials or grades of steel are you planning to cut?
  • What are the typical dimensions or shapes of your workpieces?
  • Are you looking for advice on choosing a machine or troubleshooting a blade?

Amada AXCELA G Series – High-performance Carbide Tipped Blade for Metal Cutting Band Saw.

I can provide tailored technical details or recommendations based on your needs.

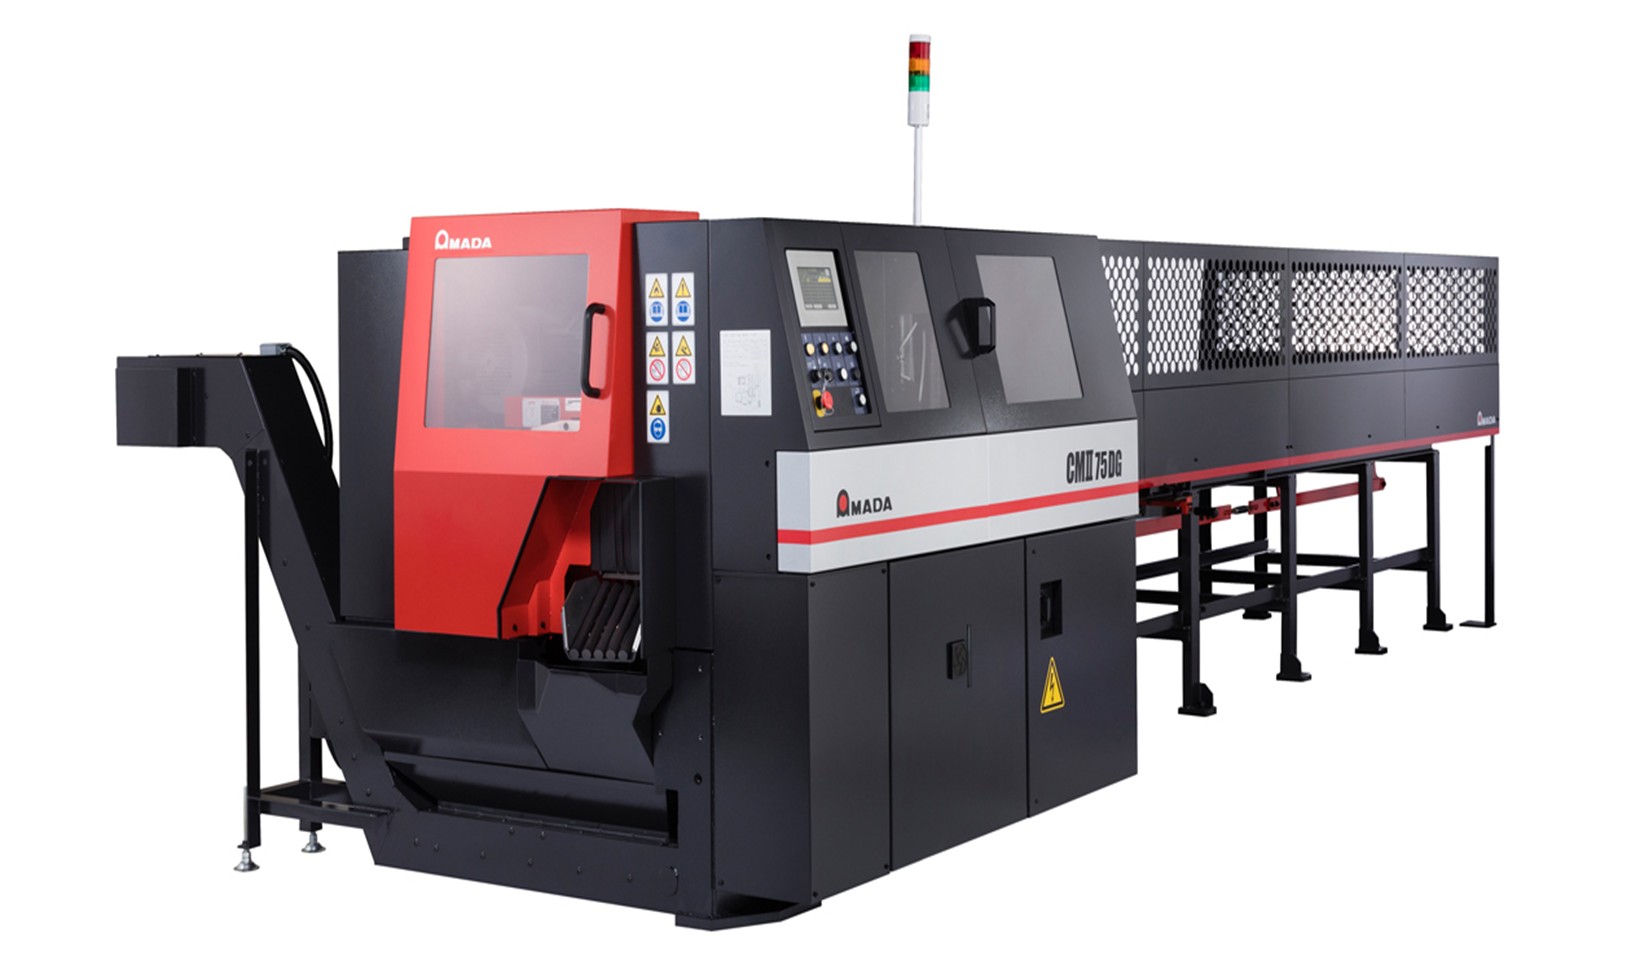
The Amada CMII-100DG is a high-performance, automatic carbide-tipped circular saw machine, designed by Amada Machinery for high-precision metal cutting and maximum productivity. Part of the CMII-DG series, it features an advanced horizontal linear guide saw head mechanism to optimize industrial manufacturing workflows.

CMII 75-100 DG


Key Features & Technology

  • Dyna Guide: Patented technology that positions a movable intermediate guide close to the initial cutting point. This increases rigidity, suppresses blade vibration and minimizes surface undulations for highly precise cuts.
  • CNC Control: Fully automatic CNC command system, allowing operators to predefine combinations of cutting lengths and quantities, making smaller production series highly cost-effective.
  • Space-Saving Design: A modern sliding door mechanism for the front cover significantly reduces required floor and work space.
  • Improved Work Environment: Features a round bar shooter that keeps metal chips from mixing into the finished product boxes.

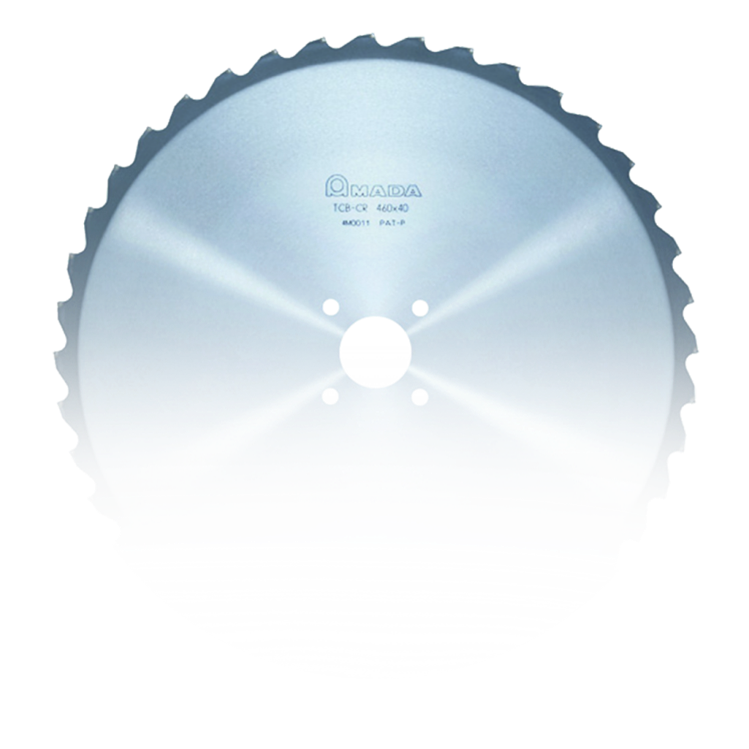
CIRCULAR SAW BLADES


For each application Amada offers the appropriate tool. Like the machines, the saw blades are permanently improved and advanced. By using Amada tools on Amada machines, always a perfect cutting result is given.

Through the dedicated backup of Amada, the robustness of their machinery, the longevity of their blades and the reputation built over many years, peace of mind is the most important part of owning an Amada.

For more information, please contact Amada – Tel: 011 453 5459.

Visit AMADA

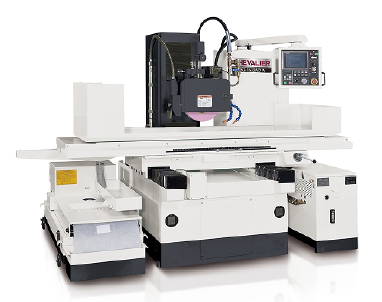
CHEVALIER FULLY AUTOMATIC PRECISION SURFACEGRINDERS – IDEAL FOR JOB SHOPS, AS WELL AS THE AEROSPACE AND CONSTRUCTION INDUSTRIES

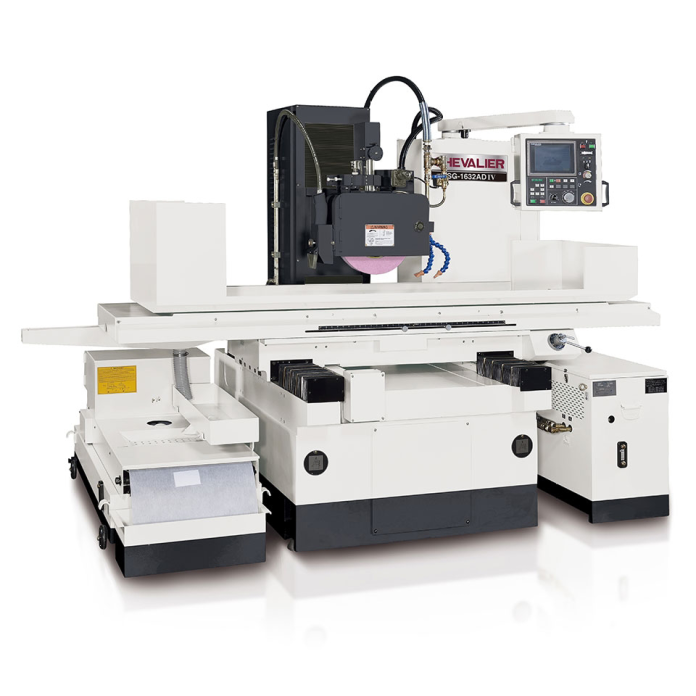
Chevalier’s FSG-ADIV Series of surface grinders have several design features to shorten processing and non-processing preparation, including iSurface control, a variable speed spindle, constant surface speed, load detection and in-machine manual dynamic balancing.

FSG-ADIV Series grinders also feature tools to secure Big Data with Chevalier’s exclusive iMachine Communications System TM (iMCS). This software package, combined with data analysis, enhances machine efficiency in the factory while enabling remote monitoring and diagnostics to track machine performance and identify potential problems before they begin. FSG-ADIV Series is ideal for job shops, as well as the aerospace and construction industries.

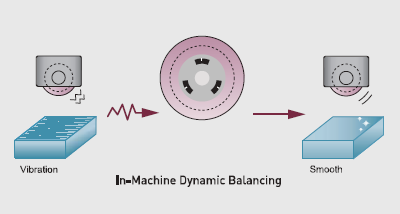
In-machine dynamic balancing

By manually adjusting the in-machine dynamic balancing function, operators can reduce grinding wheel vibration and eliminate the surface workpiece ripple to improve grinding quality.

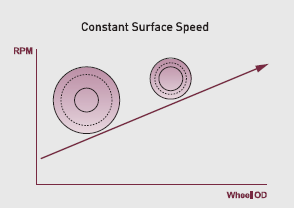
Constant service speed

Variable speed spindle

The built-in driver controls spindle speed. Combined with the automatic dressing function, the driver provides constant surface speed regardless of the grinding wheel’s changing diameter.

Load force detection

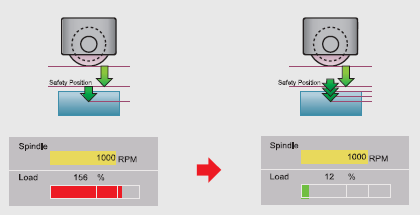
An operator can measure the spindle load during the machining cycle and then utilize this data to determine whether the wheel requires dressing. If an abnormal load is detected, the spindle automatically moves up to stop the cycle.


Enhanced control system

Unlike PLC control boards, the PC-based control’s powerful computing power enhances the HMI for more precise control. Combined with data analysis from network connectivity, it permits managers to improve production for higher output.

Wheelhead and column system

The FSG-ADIV Series wheelhead and column system is composed of hardened and ground steel guideways with inserted roller bearings. This system is preloaded which imparts zero clearance for precise straight movement, accurate feeds and precise linear movement without deviation, even during rapid traverse movement.

Completely supported guideways

The series includes extended base guideways for crossfeed and longitudinal travel to enhance rigidity and stability, upgrade accuracy and longevity and eliminate table overhang to completely support permissible loads.

The guideway rails are composed of (S55C) steel, normalized and hardened by high frequency induction. The heat treated roller bearings are preloaded between the linear guideways, ensuring accurate positioning.

AC servo motor

The AC motor provides high torque, speed and accurate positioning with minimum increments of 0.001 mm (0.00001″). A manual pulse generator (MPG) is included for ease of operation.

The cross-feed speed is controlled by the AC servo motor for better surface finish, precise movement and wheel dressing from the table.

For further information, please contact PUMA MACHINE TOOLS – Tel: (011) 976 8600.

Visit PUMA Machine Tools

TaeguTec  – NEXT-LEVEL HIGH FEED MILLING SOLUTION, THE SRMT INSERT

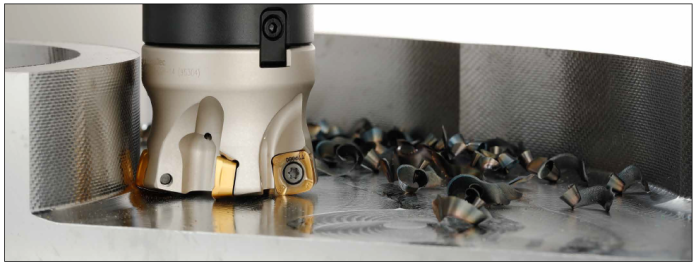
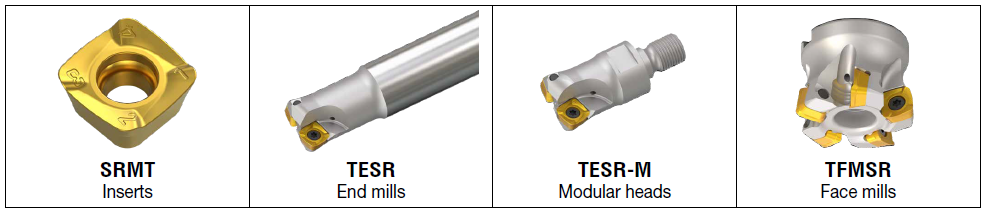
TaeguTec has launched a new 4-corner, single-sided high feed milling solution, the SRMT insert line. This high-performance insert addresses the limitations of conventional designs by delivering a premium-level solution for high feed milling applications.

Conventional four-corner, single-sided inserts often fail to utilize all cutting edges effectively. In contrast, the new SRMT insert line features an optimized cutting-edge design that enables full use of all four corners. The new line’s excellent chip evacuation significantly reduces the likelihood of chip-induced issues such as jamming, insert breakage, and surface scratches during high-performance machining operations. Moreover, despite being a high-feed milling insert, the SRMT line achieves superior surface roughness, making it ideal for high-efficiency finishing operations.

The new SRMT inserts are available in I.C. 07, 10, 14 size and come in M, MM, ML and MR chip formers across a variety of grades. The line is offered as standard in Ø16–42 mm end mills and Ø40–200 mm face mills.

For more information, please contact TaeguTec – Tel: 011 362-1500.

Visit TaeguTec

ISCAR SOUTH AFRICA – NEW MANAGING DIRECTOR APPOINTED

Gavin Adams stepped down as Managing Director of Iscar South Africa in June this year after having been with the company for 45 years.

Nico Duvenage, new Managing Director, joined Iscar 15 years ago. He started in the Tech Centre as Productivity Manager, doing Demos and customer seminars and for the last decade he was hole making product manager. During all this time he was able to build great business relationships with customers all over South Africa.

About three years ago Duvenage decided to add a business degree to his technical background in order to have the whole package, which one day could earn him a more senior position. As a result, in 2025, he acquired a Bachelor of Business Administration (BBA) NQF Level 7, graduating Cum Laude.

Duvenage says,“while  after all these years Iscar is in my blood, we got a young and dynamic team, excellent product – and sales managers, which make Iscar what it is today. Our team of application engineers and product specialists are well-trained and capable to apply the products and implement specially tailored cost saving solutions, designed to industry needs.

“In the almost 60 years of trading in the South African market, Iscar has established itself as the go-to company for the supply of innovative tooling coupled to reliable backup and superior service. Incorporated at our state-of-the-art facilities based at our head office, is a Technical Center and auditorium from where we are able to conduct product launches, industry-specific seminars as well as live demonstrations depicting the latest additions to our vast product portfolio, he concludes.”

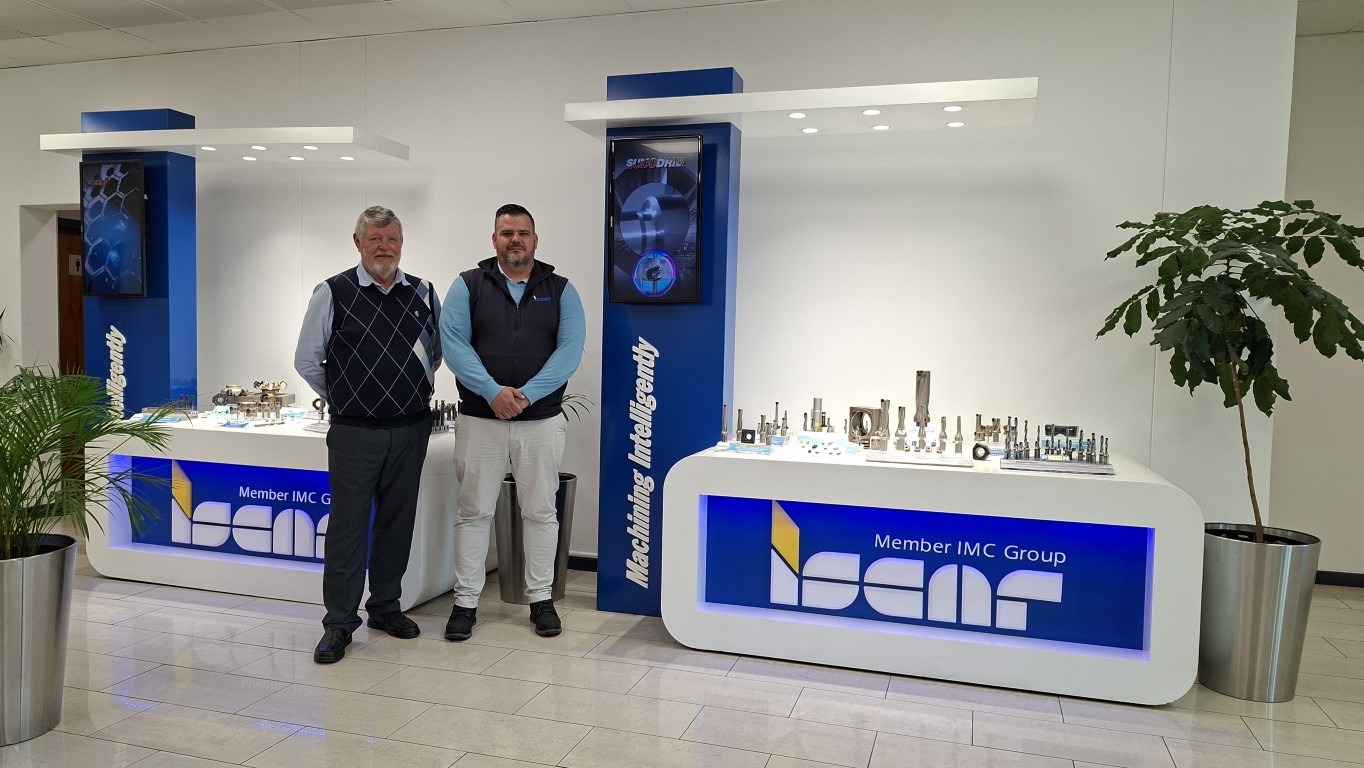
Gavin Adams (left) stepped down as Managing Director of Iscar South Africa handing over the position to Nico Duvenage (right)

For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997 2700.


Visit ISCAR

EFC ll LASER CUTTING MACHINE


A high-performance mid-price laser machine equipped with TruFiber Cut Laser up to 6 kW.Smart design and material flow ensure maximum productivity at minimal investment costs.


The EFC ll laser cutting machine from leading Chinese manufacturer JFY, a member of the Trumpf Group, is locally available from Puma Machine Tools.

The machine’s CNC control system is based on the Windows platform and has been proven to be extremely reliable and high-performing.

The cutting head is designed with built-in protective glasses, ensuring reliable and optimized cutting quality. These protective glasses safeguard the optics from potential debris or damage that may come from the process zone. Overall, this results in a significantly higher durability of the cutting head, as well as higher cutting precision.

TruFiber is the ultimate fiber laser solution for all cutting needs. In fact, TruFiber delivers excellent process stability and consistent process results. Furthermore, the technology requires a minimum of maintenance.

Using offline programming software can improve material utilization and process efficiency. On the one hand, programming software can optimize the nesting process to reduce material waste, and  on the other hand, it can simplify the programming process by converting simple and complex part drawings into processing programs, which results in faster production times. The Lantek programming software is a proven solution based on latest technology.

Visit PUMA Machine Tools

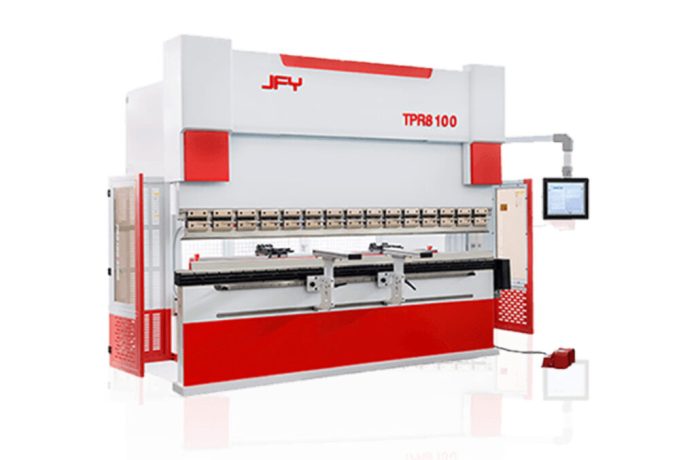
TPR8 CNC PRESS BRAKE


Cost-effective bending machine from JFY sold to more than 5.000 customers – Proven technology with high stability and reliability.


The machine body is optimized by finite element design to ensure high strength and high rigidity during operation. Compared with traditional CNC bending machines, the frequency of the Y-axis movement is 25% higher.

A broad range of options and bending tools allow the processing of large and complex workpieces, while the high-performance CNC control TJS-90 as standard configuration ensures maximum workflow efficiency and operating convenience.

The automatic mechanical crowning compensation system as standard configuration solves the influence of ram deformation on the workpiece during bending and Push-Pull Quick clamping as a standard configuration avoids part interference when bending at a small angle.

For further information, please contact PUMA MACHINE TOOLS – Tel: (011) 976 8600.

Visit PUMA Machine Tools