Home Blog Page 28

SHIFT FROM A MAKE-TO-STOCK STRATEGY TO A LEAN MAKE-TO-ORDER JUST-IN-TIME STRATEGY

Rapid industrial developments during recent years continue to set tough challenges. Because industry has changed, flexibility and efficiency are crucial requirements for managing increasingly smaller batches, rapid item turnover rate and tight lead times. And it is precisely in this context that automation is attracting more and more attention.

Automation according to Salvagnini

Salvagnini has been designing, producing and selling flexible systems for sheet metal working for over fifty years, and flexible automation has always been part of the company’s DNA. Flexible automation means transforming packs of sheet metal into a wide variety of products, in a lean environment and with no intervention by the operator, in a progressive production process, using proprietary punching, cutting, bending and panel bending technology. Automation therefore has an impact on three successive levels:

  • The first level is that of the individual production phase, which horizontally exploits the potential of extremely high-performing, autonomous and intelligent systems.
  • The second level is that of activities with low added value, which typically occur upstream and downstream of these individual systems, with preparatory and/or connection functions.
  • The third level is that of the process which, where appropriately organized, benefits exponentially from the sum of advantages offered by the previous two levels.

In practice, the result of an automated, organized process can exceed the sum of the benefits obtained in each individual activity and by eliminating any redundant intermediate activities. How? Let’s take a detailed look at the production process.

Optimizing individual production phases

We have already mentioned the progressive shift from a make-to-stock strategy, with large batches, towards a lean, make-to-order, just-in-time strategy based on medium and small batches and an increasingly variable production mix. The industrial scenario is moving increasingly towards a substantial reduction in work-in-progress, eliminating the intermediate storage of semi-finished parts.

To respond to this variability and uncertainty, the market is looking more and more to flexible production systems. While being competitive today does not merely mean having fast single part production, the challenge lies in production efficiency, the ability to move from one production code to the next with the shortest re-tooling time, whatever the geometric and mechanical characteristics of the metal sheet and the type and number of jobs. Flexible systems are a decisive factor for managing production today, but also for improving quality and reducing lead times and scrap.

All Salvagnini solutions are designed to increase the efficiency of the specific production phase. There is no need to remind anyone that, since 1977, the year in which Guido Salvagnini designed and produced the first P4 – Salvagnini has been a byword for panel bending. The panel bender is the machine which more than any other represents the spirit of the Group, precisely because it combines cutting-edge technology with productivity, autonomy, and flexibility.

With universal bending tools, the panel bender requires no re-tooling, and machines the whole range of thicknesses and materials, adapting automatically to the size and geometry of the part to be produced, in cycle, without machine downtimes or manual re-tooling. The panel bender adapts completely autonomously even to the varying mechanical and geometrical characteristics of the sheet metal being machined, as well as to the external environment. Similar characteristics also define the other Salvagnini technologies:

  • The laser requires no adjustments, thanks to the single-optic cutting head, the process sensors and a number of artificial vision systems.
  • The combined punching/shearing and punching/laser machines are equipped with a multi-press head that can hold up to 96 tools always available for use.
  • The press brake automatically adapts re-tooling and tool management according to what needs to be produced, with its ATA, MVM and AU-TO devices, thus extending its flexibility and autonomy.

Eliminating activities with low added value

Considering that our production capacity corresponds with the sum of work and waste, the second level at which automation impacts production is that of its ability to reduce, if not fully eliminate, redundant activities or those with low added value which typically occur upstream and downstream of individual systems for preparing, feeding and connecting.

   Automatic cutting, forming and panel bending systems have become extremely quick and productive, shifting the problem of efficiency to the loading and unloading phases which, increasingly often, risk becoming authentic bottlenecks. In production contexts marked by low volumes and rapid production changeovers, connecting automatic loading/unloading devices to the systems is a winning strategy for recovering efficiency.

Salvagnini responds to this need with a wide, modular range of automations, able to configure each system differently to meet different production needs.

  • Automatic loading/unloading and sorting devices, coupled to a store, which are an enabling factor for increasing the autonomy and efficiency of individual systems.
  • Automatic loading devices ensure that the machine is fed at a frequency consistent with the production speed.
  • Robotized unloading devices, which ensure that the panel bender is immediately available for the next job after completing the previous one, eliminating waiting times but also recovering efficiency in subsequent phases of the process which benefit from the precision offered by automatic bending and robotized stacking.
  • Intermediate automation devices that minimize and balance material transfer times from one workstation to the next.
  • Software solutions facilitating the production process even without large physical devices, lowering the entry barrier into the world of smart manufacturing.

Process management and optimization

Extending the vision to managing and optimizing the process as a whole, obliges us to talk of digital transformation and Industry 4.0. A widespread view often reduces Industry 4.0 to the mere integration of the ERP system and the receipt of machine feedback, when in fact this is a minimum requirement, the first step to be tackled, which must then become an enabling factor for solving real problems, simplifying everyday work and helping companies to grow.

Salvagnini has been concretely tackling this issue since 1993, when it launched the first OPS, the modular software for managing production. OPS receives the production list from the factory information management system in real-time and delivers an updated version to the programmer. It provides support for the programmer’s activities by defining the priorities, automatically generating the machine programs, and sending them to the workshop. It checks the availability of raw materials or semi-finished parts and generates feedback to the factory information management system, updating it in real time, part by part. It can make autonomous decisions according to production logic – or according to a multiple mix of production logics – designed to meet the needs of the customer and transformed into an algorithm. It integrates labelling, traceability, and store management upstream and downstream of the cutting, punching, and bending activities. It therefore increases the efficiency of the whole production process, extending its effects beyond the factory boundaries and throughout the whole supply chain.

For Salvagnini, that’s what digitalization is all about: making available solutions that are easy to use, in order to focus on control, production process optimization and the elimination of all those often invisible downtimes that undermine the efficiency and competitive performance of companies.

A vision of the future

There is no point in focusing on extremely high-performing technologies without managing the bottlenecks upstream and downstream of production. Investing to reduce the cycle times of an individual production phase by a few seconds offers no real advantage if the re-tooling times of these technologies cancel out the efficiency regained by the performance of the new system, if this regained efficiency is lost in the intermediate phases between the individual workstations, or if it is cancelled out by a burdensome process filled with redundancy, delay, and inefficiency.

Salvagnini proposes to replace this purely quantitative approach that focuses only on productivity with another that combines both quantity and quality, shifting from the idea of production capacity to that of production control, where efficiency – and therefore productivity – can be regained. To fully exploit the benefits assured by flexible automation.

For more information, contact PIM Machine Tools – Tel: 011 022 4648.

Visit PIM Machine Tools

RAPID BENDING OPERATIONS WITH FASTER BENDS SAFETY SYSTEM

Ermaksan is taking firm steps into the future by continuing to develop innovative technologies. The company has introduced the new Faster Bends Safety System to speed up the bending process and improve productivity.

Ermaksan’s new Faster Bends Safety System is ideal for small parts bending much faster and safer without using the foot pedal. Operators don’t need to press the foot pedal, except at the beginning, while the machine will move down automatically. This enables users to increase productivity and safety by bending all day without pressing the foot pedal repeatedly.

Various modes have been developed to suit customer’s needs, including the Single Break Mode, which allows the operator to initiate down movement by briefly obstructing the light guard protective field once, then taking the part, while putting in the new part at the same time. The Double Break Mode allows the operator to initiate down movement by briefly obstructing the light guard protective field twice, taking the part and thereafter placing the new one consecutively.

While safety is at maximum level and all protection devices are in line with CE regulations, press brake productivity is significantly increased.

For More information, contact WD Hearn – Tel: 021 534 5351

Visit W D Hearn Machine Tools

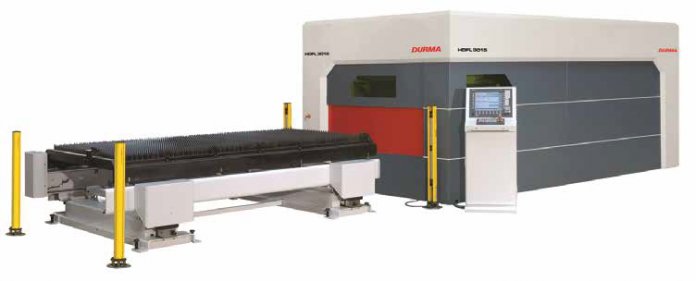
Durma HDF/HDFL 3015

Durma HDF-HDFL 3015 Fiber Laser

An integrated shuttle table maximizes productivity and minimizes material handling times. The shuttle table and pallet change system allows convenient loading of new sheets or unloading of finished parts, while the machine is cutting another sheet inside the working area.

The available shuttle table is fully electric and maintenance free; there are no hydraulic oils to handle and table changes are fast, smooth and energy-efficient.

An optional lateral automatic scrap conveyor allows the removal of scrap pieces from the working area without the need to interrupt the cutting process. The sideways operation of the short conveyors allow for easy maintenance and trouble-free running.

The Durma HDF/HDFL 3015 fiber machine achieves highest dynamics and fastest laser processing cycle times thanks to the combination of rigid mechanics and a state-of-the-art numerical control and drive system. Programmes can be loaded easily into the machine with a USB stick or over a fast Ethernet connection with the company network.

In the high-pressure auto-focus cutting head for the fiber laser the cutting lens is shielded from the laser process by an exchangeable low-cost protection window. The 1μm wavelength light is very sensitive to dust or other contamination produced in the cutting or piercing process, therefore the cutting head is being well protected in an additional cover to ensure that all critical parts remain as clean as possible.

The integrated capacitive distance sensor is capable of having the head follow height differences in the sheet even at the extreme high cutting speeds that can be achieved with the fiber laser technology, while state-of-the-art linear motors promote accuracy and increase productivity.

The CAD/CAM software provided has all the tools to import or draw parts, prepare and optimize automatically different geometries for the laser cutting process and make efficient nests.

The all-solid-state fiber laser technology reduces maintenance requirements, and offers the lowest possible running cost with a wall-plug efficiency of 30% and without the need of any laser gas. When the application requires a broader spectrum of material types to be cut and the maximum thickness range is limited, the fiber laser is the ideal solution and it will cut faster at lower cost than any CO2 laser at the same laser power.

For more information, please contact Spectrum Machine Tools – Tel: 011 865-4090

Visit Spectrum Africa

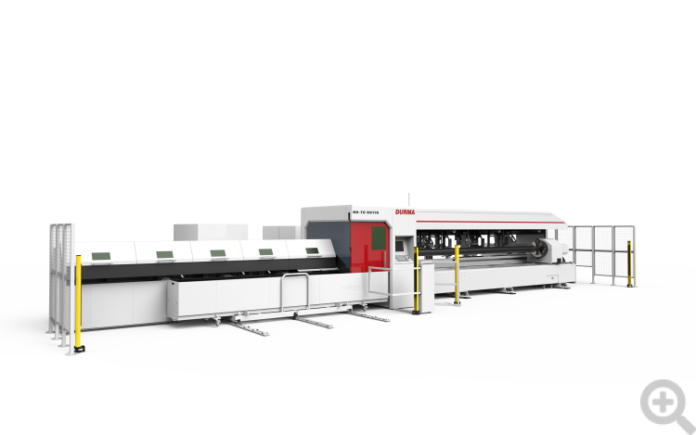
HD-TC PROFILE-PIPE CUTTING LASER

DURMA shortened process time by improving centering with the newly added laser sensor centering option added to the HDTC machines. It is possible to control the size and irregular structure of the profile during cutting or before cutting with the help of sensors to ensure that the internal contours to be cut are at the right point.

In existing HD-TC machines, the centering measurement is achieved by scanning the profile surface through capacitive sensors. The advantage of the laser sensor system is that it gives more precise results in a shorter time. The user can take measurements at the distance determined by the user, and precise results are obtained in a shorter period of time as the process of measuring by the sensor is shortened for parts requiring precise measurement with internal contours.

The advantage being fast set-up time, less problems during cutting, best solution in a short time and measurement frequency is dependent on operator request.

For more information, please contact Spectrum Machine Tools – Tel: 011 865-4090

Visit Spectrum Africa

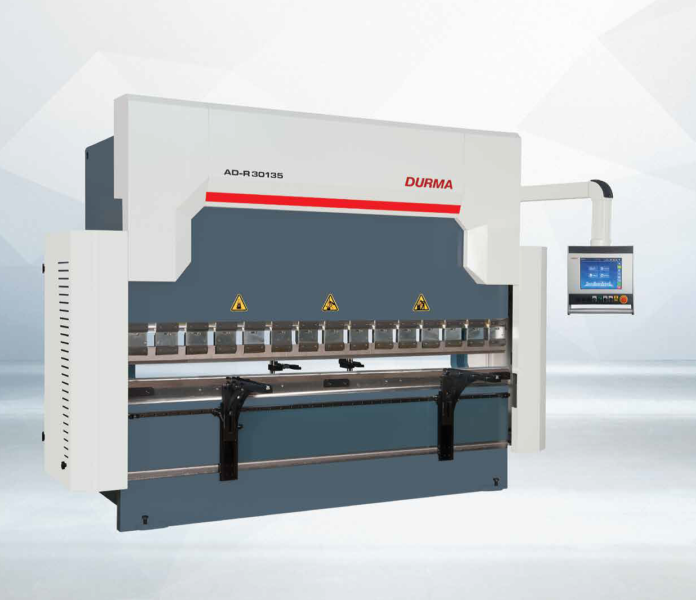
AD-R SERIES PRESS BRAKE

With its easy to use control unit, rigid body frame, perfect design, high efficiency, multiple tool usage solutions, top level CE safety standards and economical price range, AD-R is a world leader in its category. The machine is perfectly equipped for sensitive bending, energy efficient solutions.

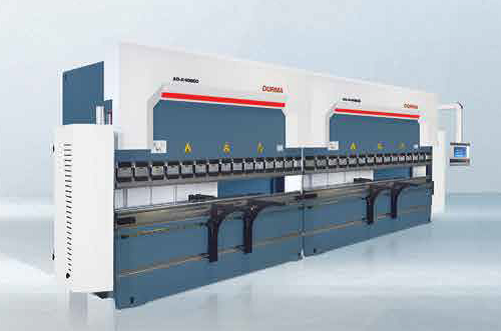
AD-R series press brakes are built in accordance with CE-Norms to ensure safety with hydraulic, electric, appropriate height covers and laser light curtains, while CE safety in tandem machines are also provided with light barriers and designed with high technology to increase efficiency on precise part bending.


With an easy to use control unit, stable body structure, perfect design, low operating cost, different tool usage options, maximum safety standards, Durma press brakes are amongst the best in the world. Bending performance is increased by using a high quality European clamping system to improve productivity.

Most important feature to achieve perfect bending is the stability and the design of the back gauge, which allows an impeccable and correct product to be produced.

The high speed ballscrew back gauge system movement is supported with linear guides, which helps the back gauge achieve long life and greater sensitivity, while strengthening against any collisions.

AD-R 30135

  • Capacity (Length x Ton) 3050×135
  • X=650mm X,R (AL)
  • CNC Controlled Motorized Crowning
  • Control Unit Sky 22 (Colour Graphic 22’ Screen)
  • DBEND 3D CAD/CAM Importing & Simulation Program
  • Non CE with Manual F.AKAS FPBS
  • Top Tool European P97.75.R08
  • Bottom Tool European M.46R.85
  • Quick Release clamping
  • 60mm Die Holder (For European Dies only)
  • Throat Depth 450mm
  • Back Gauge: Motorised & Linear Guide & Ballscrew System
  • Back Gauge Fingers Height Adjustable
  • Back Gauge Motor: Servo
  • Sliding Front Arms with Full Length Linear Guide
  • Safety Covers (Side)

Specially designed finger blocks with steps to achieve maximum stability can be supplied for every kind of bending solution.

With an impressive variety of tool options and types available, Durma is the ideal solution partner, while providing the best level of service and readily available spare parts.

For more information, please contact Spectrum Machine Tools – Tel: 011 865-4090.

Visit Spectrum Africa

FIBRE LASER WITH LBC TECHNOLOGY – NEW POSSIBILITIES IN LASER CUTTING

Higher Productivity & Quality with less power

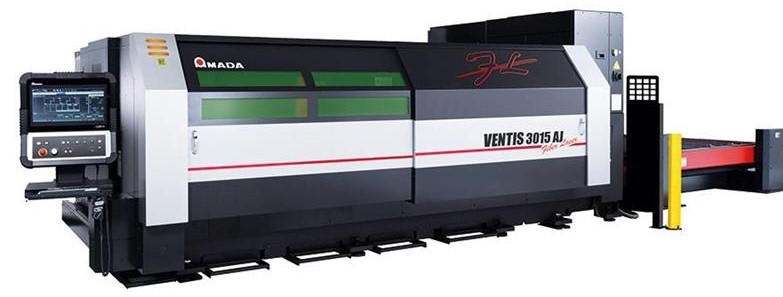
Following on the great success and longevity of the Amada range of in-house developed fibre laser engines, Amada has developed and released the revolutionary VENTIS fibre laser machine.

What sets this machine far apart from other fibre lasers is the incorporation of the Amada patented LBC technology (Locus Beam Control) and what makes this technology revolutionary is the innovative beam shaping system that allows for precise control of the laser beam motion.

This in-house developed single diode module 4kW fibre engine provides outstanding beam quality which allows the VENTIS 4kW-AJ to compete with other 6 – 8kW machines with less power requirements and unrivalled cutting quality.

LBC is a built-in automatic feature, allowing for the oscillation or vibration of the laser beam within the nozzle while cutting. The oscillation pattern differs according to the specific material type and thickness being processed. The LBC reduces the drag of the laser beam, while cutting and efficiently removes the material on the cutting front of the beam faster than standard fibre laser beams. LBC provides and ensures high beam energy density and produces high melting temperatures. In order for LBC technology to work at its optimum, a very high laser beam quality is required – Beam Parameter Product = 1 (BPP = 1).  While Amada’s AJ4000S high power oscillator ensures this beam quality permanently under all cutting conditions, the VENTIS offers three different cutting modes for steel processing, namely Productivity mode for maximum cutting speed, especially on thinner materials, Quality mode for burr free cutting on thicker materials like stainless steel and  Kerf control mode for increased cutting kerf width for easy thick part removal.

The VENTIS is equipped with all the operation friendly functions of automatic nozzle cleaning, automatic nozzle changing, shuttle table system with free roller bearings for easy sheet loading, user friendly 3i control, water assisted cutting, filtered air – air purge system, full side and front access, oil shot, tipped part avoidance as well as “intelligent head control” as an additional feature that also saves both time and money.

With a combined speed of 170 m/min and an accuracy of +-0,01mm, the VENTIS is a machine that has proven its capabilities with over 100 units sold in Europe alone within two years. This number of sold units is evidence of the markets looking for better, faster and more reliable laser cutting solutions at a drastically reduced operation cost.

All equipment is fully retro-fittable with the full range of Amada automation options, making uninterrupted and unmanned production possible 24/7.

HRB-ATC PRESS BRAKE WITH ADDITIONAL BENDING CAPACITY

Once the blanking of a product is done to the finest of detail and tolerance, the bending becomes the next process in most production runs.

With the outstanding success of the Amada HG-ATC range, the market realized how much downtime is spent on tool setting in the bending process. Most shops’ production will require approximately three or four tool changes per shift. These tool change processes can take anything up to around 20 to 30 minutes each, which means around two hours of production is lost each day only to tool changing.

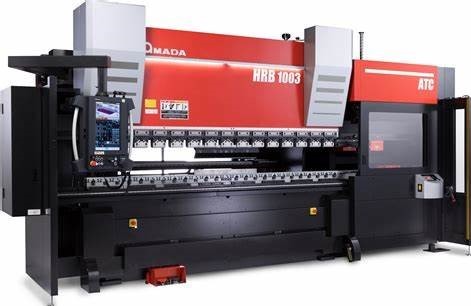
The new HRB-ATC press brake is a 100 ton x 3 meter or 220 ton x 4 meter – 7 axis CNC bender which loads and unloads the tooling as required for the specific job on hand. Production planning, programming, tool fitting and sequencing is done in the drawing office before all information is sent to the machine via network; the transfer takes place by scanning of a bar code.

Once downloaded, the operator can view the 3D model as well as a 2D flat layout of the part with or without dimensions. The press brake will automatically begin to set up its own tooling from the tool magazine situated to the right of the machine, while human hands do not touch the tooling. The machine picks and locates each tool as required along the top and bottom beams. Once positioning is completed, the operator takes over with the bending process according to pre-determined sequencing that was done in the planning stages. The interactive control shows the bend sequence in 3D throughout the process. An added advantage is that trial bending is no longer required as the full process has already been checked during the planning stages when it was programmed.

The HRB-ATC press brake is supplied with either the Bi-S mechanical or Bi-L laser angle measurement systems. These systems measure each bend angle according to the desired and programmed requirement, allowing the machine to make automatic angle adjustments where necessary on each bend. This process ensures superior accuracy as well as high quality repetition.

Tooling in the ATC system is of the standard AFH (Amada Fixed Height) design with a very small modification for the tool picker to locate. Standard Amada tooling can be loaded into the machine manually if the ATC does not have the required tool available in the magazine.

The advantage of the ATC system is that the downtime caused by tool changes is drastically reduced. The tool layout is always 100% as per requirements of the bends to be performed and tooling life is drastically extended as tools are stored correctly and not dropped or banged together during handling.

While a component is blanked 100% but not bent 100%, the finished product is automatically inferior and therefore, Amada will see to it that blanking and bending needs are fully taken care of and downtime eliminated.

For more information, please contact Amada – Tel: 011 453-5459.

Visit AMADA

ADVANCED LASER CUTTING IN THE FAST LANE – ByStar FIBER WITH 20 KILOWATTS OF LASER POWER

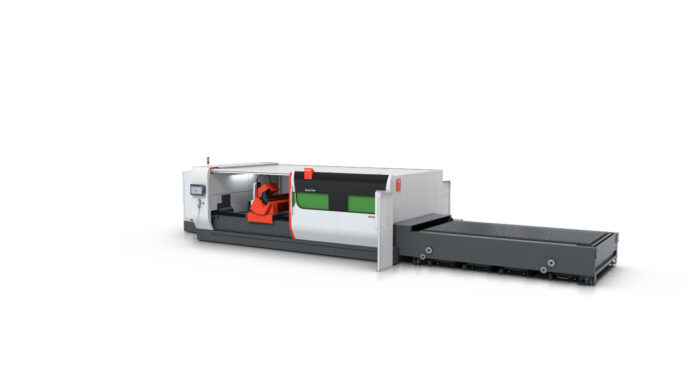
For ultra-fast speeds and extended cutting spectrum, the ByStar Fiber now cuts with 20 kilowatts of laser power.

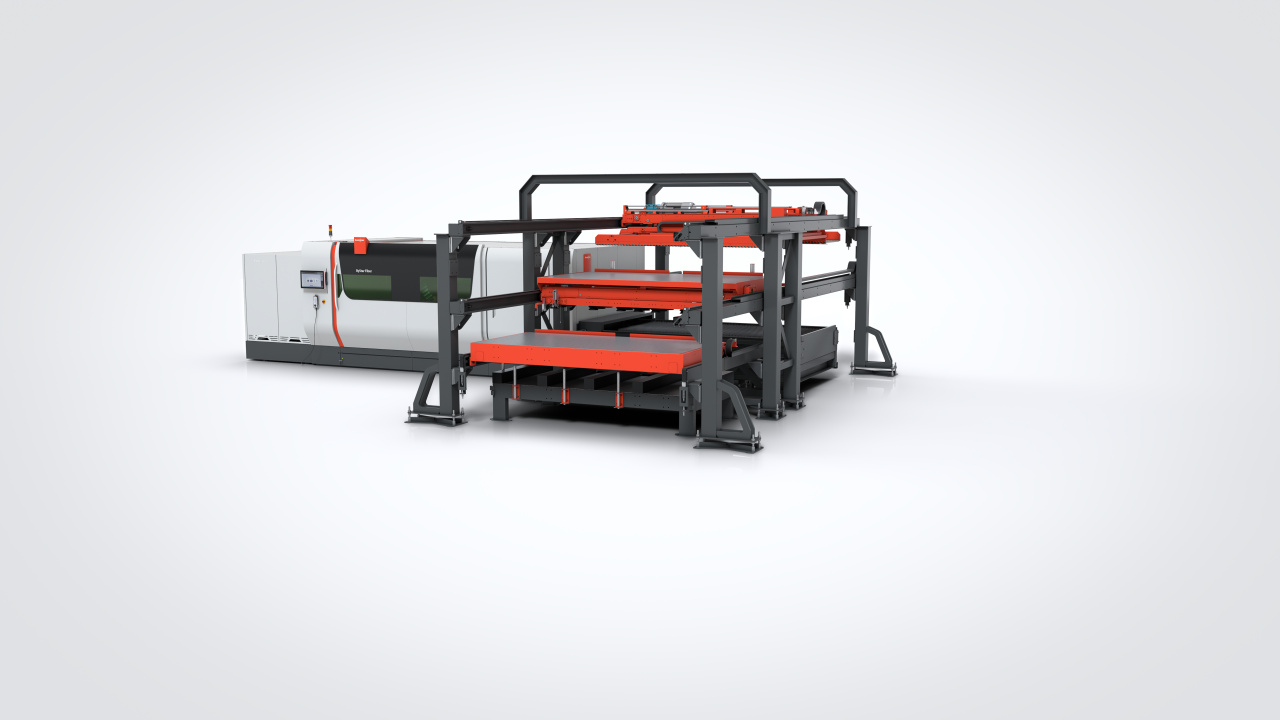
The flagship of Bystronic’s laser cutting systems is available with 20 kilowatts of laser power and optimized cutting process. Its latest-generation cutting head was developed to achieve consistently high quality with the highest laser outputs and for demanding cutting applications. This enables sheet metal processing companies to further optimize their production.

Enhanced cutting quality and productivity thanks to the new, even higher laser power

In order to offer sheet metal processing companies even more effective support in an increasingly competitive environment, Bystronic recently advanced into a new dimension of fiber laser cutting, the 20 kilowatt ByStar Fiber. The high-end fiber laser represents high-precision Bystronic technology, a reliable cutting process even with the highest laser outputs and a wide range of applications. This enables sheet metal processing companies to take another major step forward in terms of productivity and efficiency. The technological leap from the previously available 3 to 15 kilowatt laser output levels to the latest 20 kilowatt level is considerable and opens up new possibilities for Bystronic’s customers to optimize their production and thus remain one step ahead of the increasingly fierce competition.

Increased productivity thanks to outstanding laser technology for a broad spectrum of sheet metal processing applications.

Speed for an extended cutting spectrum

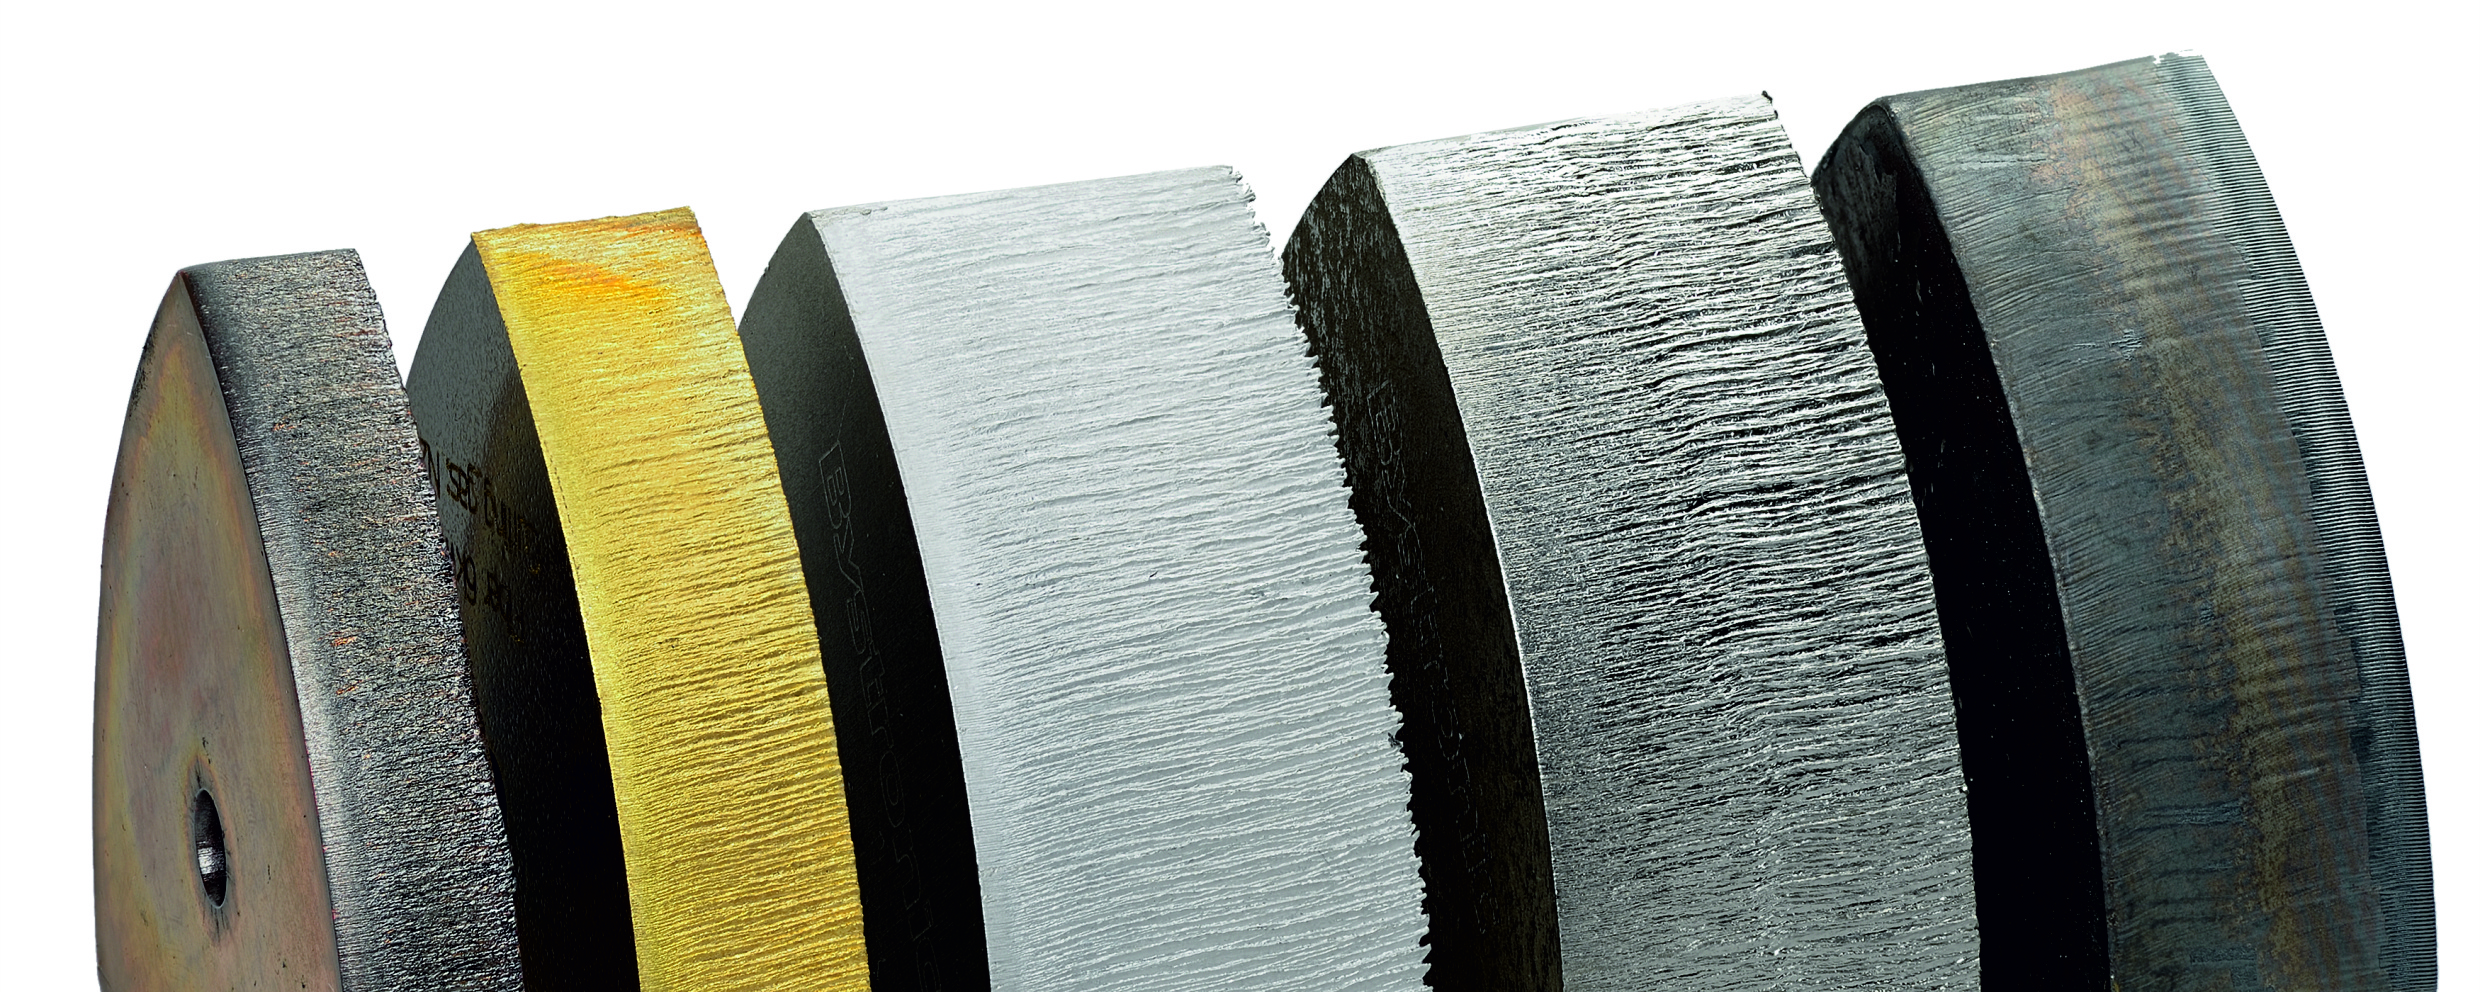
Compared to 15 kilowatts, the productivity of the 20 kilowatt ByStar Fiber are on average 40% in mild steel and stainless steel 4 mm to 20 mm. This means that sheet metal processing companies can benefit from higher productivity at low unit costs, because thanks to its 20 kilowatts, the ByStar Fiber cuts steel, aluminium and stainless steel precisely and reliably. The 20 kilowatts of laser power thus enable maximum flexibility for both large series and urgent customer orders. Regardless of whether cutting aluminium, non-ferrous metals or steel, the high-performance Bystronic cutting head excels with maximum precision in both, thin and thick sheets and profiles. In addition, the 20 kilowatts open up extended applications in steel and aluminium of up to 50 mm.

The optional «Parameter Wizard» ensures that the correct quality of cut parts is always selected by obtaining the perfect parameter within minutes.

The new power level is available for the ByStar 3015, 4020, 6225 and 8025.

Bystronic’s high-performance flagship is controlled using the ByVision Cutting software via a 21.5-inch touch screen. Operating the machine is as simple as using a smartphone.

Bystronic automation solutions optimize the material flow

Automation optimizes the material flow: Matching automation solutions increase machine utilization and process reliability.

A wide range of automation solutions guarantees maximum machine utilization and process reliability even during unmanned operation. In order to ensure an optimal material flow that makes full use of the high laser cutting speeds, Bystronic offers a wide range of automation solutions for the ByStar Fiber. These include loading and unloading systems, sorting solutions, and individually customizable storage systems. This makes it possible to create an automated laser cutting process that is seamlessly integrated and adapted to the existing production environment and available space.

For more information on the please see www.bystronic.co.za or contact Bystronic on 010 410 0200.

Visit Bystronic

FIRST CUT AND MESSER CUTTING SYSTEMS DISCUSS NEW STRATEGIES

First Cut, South African supplier of cutting, welding and grinding consumables and other equipment recently hosted a visit from the President and CEO Global of German company Messer Cutting Systems, John Emholz, in order to consolidate their existing relationship and discuss strategic new possibilities.

Emholz was joined by Martin Zeller, Division Manager Sales and Axel Vogelsang, Area Sales Manager, Oxyfuel Business Unit, who is also the main point of contact for First Cut and their customers regarding Oxyfuel Sales and Service.

In 2019 First Cut concluded an agreement with Messer Cutting Systems, which is a global supplier of cutting solutions for the metalworking industry, to take over the existing South African distribution agency.

Emholz explains: “The focus of this visit was largely at a strategic level, in order to understand how to bring in our cutting systems expertise and look at opportunities that we believed could be leveraged, including discussing market leads with First Cut for both the oxyfuel as well as the equipment side of our business.

“We believe that we have a viable opportunity to leverage some of the South African market developments on a global basis. We have a strong commitment to this market, and certainly this visit has clarified and strengthened our understanding of the significant long-term market potential in the South African market.”

Andrew Poole, Managing Director of First Cut adds: “Messer Cutting System’s participation in our local distribution and sales strategy development has really been demonstrated by John as their President and global CEO, visiting in person.

“This shows an invaluable and highly-appreciated long-term commitment on their part. Messer Cutting Systems is a large, global organisation which has given us great flexibility in the local distribution of their products. Having held joint discussions on how to position ourselves in the South African market, we have some very exciting new directions unfolding. In this regard, our safety offering has been very important, Poole says.”

John Emholz, President and CEO Global, Messer Cutting Systems, Germany

Safety is of paramount importance in First Cut’s key target cutting and welding market sectors, as reflected by its recent merger of interests with Gas Safety International (GSI), which provides certified gas safety training and quality gas equipment to a wide range of industrial sectors, while ensuring a safe and efficient working environment.

Andrew Poole, Managing Director, First Cut

This relationship has strengthened First Cut’s service offering, particularly due to the outstanding training experience and expertise offered by GSI’s Managing Director Peter Rohlssen, with regards to gas safety training, consulting and auditing.

“This holistic safety offering and the passion and experience demonstrated by First Cut and GSI are very attractive,” observes Messer’s Martin Zeller. “It immediately inspired us upon our arrival and it has only added to the overall relationship of trust which Messer Cutting Systems and First Cut share.”

Another key First Cut relationship involves its agreement with the Bolt and Engineering Distributors (B.E.D.) Group, whereby First Cut is a primary distributor to the fabrication – and other sectors, while B.E.D. focuses on the mining industry, where they are already well-established.

“We truly appreciate these initiatives which First Cut has engaged in – and how they work to strengthen the overall market offering and distribution of our products in South Africa,” Emholz enthuses. GSI’s safety knowledge, together with First Cut and Messer Cutting System’s own expertise, has resulted in the development of a trio of new products.

We are very pleased to play our part in this collaboration, which will be rolled out globally, yet with a ‘proudly South African’ flavour. This is indeed an illustration of the seriousness with which both First Cut as well as Messer Cutting Systems have approached this relationship.”

Zeller adds: “We are very enthusiastic about the features and potential uptake of these new products in the market. This demonstrates that First Cut and B.E.D. are truly value-adding partners, helping us to find solutions for the mining and industrial sectors. This is a pivotal development for Messer Cutting Systems and First Cut,” he says.

In conclusion Emholz adds: “Having seen the opportunities here in South Africa, Messer Cutting Systems is very keen to promote our footprint and traction accordingly. Furthermore, the excellent, value-adding collaboration between Messer, First Cut and its partners is a significant opportunity for us to learn from the local market.”

Visit First Cut

HYUNDAI WIA XF6300 5-AXIS VMC

The XF6300 5-axis vertical machining center provides high speed, simultaneous 5-axis precision and optimal rigidity combined with outstanding user convenience.

The XF6300 comes with a 19″ large monitor for enhanced visibility and the SIEMENS ShopMill customized technology package as standard. ShopMill provides simple operation, supporting all operator actions with graphic help displays and functions for quick and practical machine setup, including calculating the workpiece position in the machine. The control panel has the same configuration as a computer keyboard for easy usage. Mold Package is provided as standard for a highly efficient mold process with the aid of various NC options and automatic tool measurement.

While the integrated bed and column have been designed by using HYUNDAI WIA’s unique analysis method, the XF6300 features a 4-way structure box type saddle inside the cross-beam to increase stiffness and minimize thermal displacement. The Box-in-Box structure design accomplishes thermal equilibrium, while minimizing thermal deformation. The direction of the main axis’ center of gravity and z-axis moving direction are in the same line, providing more precise machining.

The XF6300 features X-axis 650mm, Y-axis 600mm and Z-axis 500mm with 60 m/min rapid traverse and 1G of X/Z-axis acceleration and deceleration and a linear scale to all linear axes plus rotary scale to rotating axes as standard.

XF6300 is a 5-axis vertical type machining center designed by European R&D center in Germany

Various multipurpose built-in spindles are available, providing 15,000 rpm or optionally 24,000 rpm and 40,000 rpm for high quality mold machining. The main spindles produce almost no noise and vibration even at high speed machining, while ensuring highly stable machining performance.

The XF6300 main spindle features an oil cooling device as standard promoting high accuracy for long periods of time and a HSK tool holder for high positioning accuracy and precision.

The XF6300 is designed with a 5-axis rotary table which can be moved 30 degrees to the front side of the machine and 120 degrees to the rear side of machine based on A-axis and C-axis and can rotate 360 degrees. A-axis and C-axis achieve 70rpm and 110rpm, respectively.

The rack-type magazine providing various options equipped with 34 tools and has a single layer as a standard. Tool magazines can be upgraded to accommodate 68 tools and 102 tools, respectively.

For more information, contact Spectrum Africa – Tel: 011 865 4090.

Visit Spectrum Africa

THE SAFANDARLEY E-BRAKE ERGONOMIC

With the Ergonomic design of the E-Brake, SafanDarley enables the operator and the press brake to work as a unit. The operator is partially seated inside the machine, surrounded by an edging table with his legs in a spacious cut-away below the lower beam, where the foot pedal is located.

Ergonomic ease of operation is assured as the seating position as well as the height and angle of the footrest can be adjusted. The SafanDarley E-Brake Ergonomic can easily be adapted to changing work situations, such as a different product or a different operator. The edging table can be adjusted enabling users to achieve perfect pick-up height, working height and cast-off height every time. In addition, the edging table can be fully or partially collapsed, enabling the operator to bend whilst standing up. Finally, the entire edging table can easily be removed from the machine to make the front freely accessible.

While the height of the rotating 17″ Touch Screen is adjustable, the unit can be placed to both the left and right of the operator, meaning that left-handed operators can use the machine with the same level of ease as right-handed operators.

The double-function safety light screen, integrated into the control panel secures the bending zone and allows the axis to move, while the operator turns, picks up or removes the product. These simultaneous actions of operator and machine lead to very fast cycle times.

While the innovative back gauge can be used across the full working length, it has a maximum depth of 1000mm and a height adjustment of 150mm. Combined with the possibility of setting the upper beam at a 5° angle, this means unparalleled flexibility. The back gauge comes with an X axis and an R axis as standard features, but can be expanded, depending on the model, with 5 optional axes.

For more information, please contact CML Machine Tools – tel: 083 232 9470.

Visit CML Machine Tools