With the Ergonomic design of the E-Brake, SafanDarley enables the operator and the press brake to work as a unit. The operator is partially seated inside the machine, surrounded by an edging table with his legs in a spacious cut-away below the lower beam, where the foot pedal is located.
Ergonomic ease of operation is assured as the seating position as well as the height and angle of the footrest can be adjusted. The SafanDarley E-Brake Ergonomic can easily be adapted to changing work situations, such as a different product or a different operator. The edging table can be adjusted enabling users to achieve perfect pick-up height, working height and cast-off height every time. In addition, the edging table can be fully or partially collapsed, enabling the operator to bend whilst standing up. Finally, the entire edging table can easily be removed from the machine to make the front freely accessible.
While the height of the rotating 17″ Touch Screen is adjustable, the unit can be placed to both the left and right of the operator, meaning that left-handed operators can use the machine with the same level of ease as right-handed operators.
The double-function safety light screen, integrated into the control panel secures the bending zone and allows the axis to move, while the operator turns, picks up or removes the product. These simultaneous actions of operator and machine lead to very fast cycle times.
While the innovative back gauge can be used across the full working length, it has a maximum depth of 1000mm and a height adjustment of 150mm. Combined with the possibility of setting the upper beam at a 5° angle, this means unparalleled flexibility. The back gauge comes with an X axis and an R axis as standard features, but can be expanded, depending on the model, with 5 optional axes.
For more information, please contact CML Machine Tools – tel: 083 232 9470.
In 2019, Bolt and Engineering entered into an agreement with First Cut, distributor in South Africa for Messer Cutting Systems, a global supplier of cutting solutions for the metalworking industry. According to the agreement, B.E.D. and First Cut, South African provider of cutting, welding and grinding consumables and equipment, would jointly distribute Messer’s products and solutions in South Africa.
B.E.D. CEO Mike Giltrow explains: “While we are very pleased to be part of this collaboration, B.E.D. will focus on Messer Cutting Systems solutions for the mining industry, where we are particularly well-established and First Cut will remain the primary distributor to the metal fabrication and other sectors. We both have decades-long experience and faced many similar challenges, so our relationship is built on strong foundations.
Andrew Poole, Managing Director of First Cut, concurs: “B.E.D. was an excellent choice of collaborative partner, with many benefits for Messer customers. These include their strong local presence in the mining sector and nationwide footprint of nine branches, two of which feature dedicated welding and cutting repair centres. In addition, factors such as B.E.D.’s Level 2 B-BBEE credentials, together with their very active sales force and mobile welding technical support teams made the decision to partner with them a very good one.”
Giltrow adds that both companies are very pleased to be working together with the mutual goal of growing and elevating Messer Cutting Systems brand profile and market penetration locally. “This is a re-emergence of the brand in South Africa,” he enthuses. “From B.E.D.’s side, we are excited to be working as a certified Messer distributor along with First Cut to grow this global brand and introduce it to a new generation of Messer customers in South Africa.”
Gas safety training
Quality and safety are of paramount importance to both B.E.D. and First Cut. This is further evidenced by the recent merger of interests, in late 2021, between First Cut and Gas Safety International (GSI).
Explains Poole: “The welding process follows on naturally from cutting, forming the next integral part of the fabrication and manufacturing value chain. The merger of interests with GSI, headed by Managing Director Peter Rohlssen, brings synergies, strengths and new offerings to the table, specifically with regards to gas safety training, consulting and auditing.”
Poole points to the currently strong commodities market, which has boosted mining and that mines are consequently well-placed to reinvest in aspects such as gas and welding safety training, a critical factor in their daily operations.
“Together with GSI, we have developed three gas safety courses – Levels 1, 2 and 3. This includes an introductory gas safety course presented in English and several local African languages along with an oral test on completion, which takes into account those participants who perhaps are not fully literate and cannot complete written examinations,” he explains.
Giltrow remarks that these gas safety training courses will be well-received in the mining sector, and this will enable B.E.D. to add further value to customers in this pivotal national industry.
Peter Rohlssen, MD of GSI, comments: “Having presented gas safety courses in South Africa for the last 30 plus years largely on our own, it is now a fantastic opportunity to extend our reach via the very well established and connected First Cut and B.E.D Group.”
Martin Zeller, Division Manager Sales: Oxyfuel Business Unit at Messer Cutting Systems says: “We really appreciate the way in which this dynamic collaboration has developed and have great respect for the obvious trust that this shows between B.E.D., First Cut and GSI.
“We are also most appreciative of the high regard that is paid to the role of safety amongst the partners which aligns with Messer Cutting System’s own proactive approach to safety. These strategic partnerships have given us the possibility to roll out our knowledge and expertise into the African market and the mining industry.”
For more information, please contact First Cut – Tel: 011 614-1112.
Despite the current turmoil in the Ukraine / Russian war zone, South African steel supplies have not been badly affected, even though these warring countries are two of the world’s largest steel producing and exporting countries, together accounting for some 20 percent of the European Union’s imports of finished steel products. Nonetheless, the local steel industry still faces challenges of its own, which the Southern African Institute of Steel Construction (SAISC) is poised to assist with. This is according to Amanuel Gebremeskel, Technical Director at the SAISC.
He says, “we are satisfied that the war in Europe will not create a local steel supply shortage, at least for the moment. It should also be noted that as a country, we are a primary steel producer ourselves and an importer of steel from China, so there is still a steady supply of steel currently. Nonetheless, we are keeping a careful eye on the availability of supplies and other local challenges which must be addressed,” he adds.
“The SAISC is well-known as a custodian of steel industry knowledge and standards and proud of its willingness to innovate, adapt and be an industry trailblazer!” comments Denise Sherman, SAISC Marketing Director.
Sherman says that following two years of the global Covid-19 pandemic and several years of steel sector difficulties prior to that, the sector requires a champion now more than ever.
Gebremeskel points out that the steel industry plays an important role in South Africa’s economy. “As such, the SAISC has been the sector’s official representative body, pioneering and championing its interests, innovation and development since its founding in 1956 and the Institute is respected for its reservoir of authoritative technical knowledge and its role as the collective voice of the steel construction industry.”
In fact, with access to over 60 years’ worth of local steel industry project case studies and an impressive number of experienced and highly-qualified team members, the SAISC is one of only six Institutes of its kind in the world and an extremely valuable resource for the local steel industry.
“It is our particular strength to be able to see the bigger picture, while liaising with role players and organisations across the steel value chain. From engaging with the primary steel producer, merchants and fabricators to consulting with engineers, specifiers and architects on technology and design recommendations, we play a key role for decision makers across the steel industry. The SAISC therefore encourages interested and eligible professionals to join as members, particularly engineers and fabricators and also looks forward to partnering with an increased number of large engineering companies, which perform such a key role in building the nation,” he explains.
“In this way, we hope to play a unifying role, helping South Africa to reindustrialise and thereby strengthening our economy. We are currently hard at work on one of the most important events in our annual calendar, the SAISC Steel Awards, which celebrates the use of steel in both industry as well as daily life, and showcases our role in fostering a spirit of innovation and a paradigm of excellence across South Africa’s steel value chain,” he says.
Sherman adds that during the lockdown period, the SAISC and its members, like most organisations around the world, adopted a remote and digital way of working. “This model definitely kept the wheels turning during the first two years of the pandemic. At the same time, the SAISC was changing to keep pace with a younger average industry age of its engineers and the on-boarding of a new digital generation.
“We have, however, started implementing face-to-face meetings again, wherever possible. In essence, we are preparing to foster a hybrid future, in which we continue to embrace digital working, while preserving our strong heritage of facilitating in-person relationships and networking.”
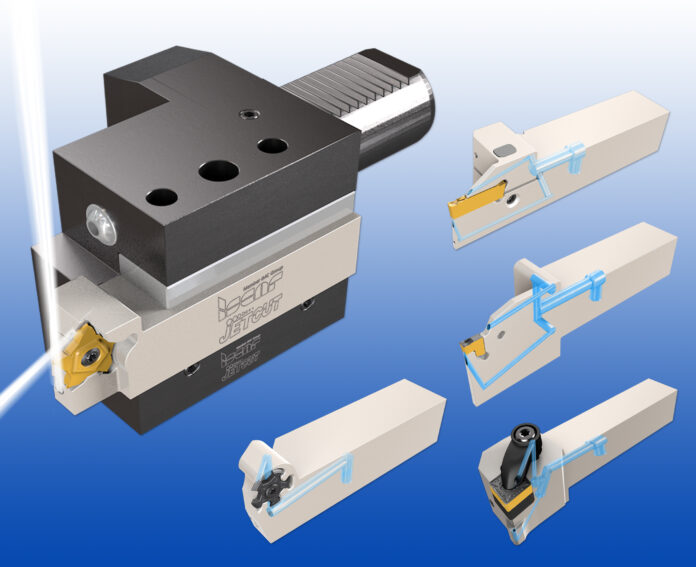
Tools with Bottom Fed High Pressure Coolant Channel for Mounting on VDI DIN69880 Tool Holders
ISCAR is expanding the Multi Connection (MC) JHP Line by adding parting, grooving, threading and turning tools for VDI tool holders with a bottom fed coolant system to ensure efficient coolant supply internally through the tool and externally through the flange. The specially designed system integrates JHP-MC turning and grooving tools featuring a bottom coolant inlet hole, and VDI-JHPMC tool holders with a long coolant outlet slot to enable adjustment of the tool’s overhang.
The compact and light VDI DIN69880 is the most popular quick change adaptation system for CNC turning machines with disc-type turrets. This standard holder adaptation serves mainly stationary turning or drilling tools.
VDI DIN69880 characteristics include high accuracy and center height repeatability, easy and fast set-up, and high stiffness due to a straight shank and flange face contact. Rigidity is facilitated by the serrated clamping system.
The tools are widely used by European, Japanese, Korean, USA, Chinese and Taiwanese machine tool builders, due to their simplicity, low-cost and tool clamping rigidity and have applications particularly in the aviation, aerospace and medical industries.
JHP tools also provide advantageous performance when conventional pressure is applied.
For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997-2700.
After four years, the sheet metal working community is eagerly awaiting its leading meeting place for the industry. EuroBLECH 2022, the 26th International Sheet Metal Working Technology Exhibition, takes place from 25 – 28 October 2022 at the Hanover Exhibition Grounds in Germany. Four months ahead of the show, around 1,300 exhibitors from 39 countries already secured their stand space at the world’s leading trade exhibition for the sheet metal working industry. Currently, major exhibitor countries are Germany, Italy, Turkey, China, Switzerland, the Netherlands, Spain, Belgium, Poland, Austria, Portugal and the USA. Exhibiting companies have already secured a net exhibition space of 88,600 square metres.
“A lot of innovations have been developed in the past few years, with a focus on cost and resource efficiency. While digitalisation and Industry 4.0 were topics, only large companies were realising at the previous EuroBLECH, these key drivers have now reached the factories of small and medium-sized companies, too. Exhibitors at this year’s event will present everything they have on offer to innovate and digitalise the manufacturing process, along the entire sheet metal working technology chain. All these developments are reflected in this year’s motto for EuroBLECH, ‘Your gateway to a smarter future’. The event will offer everyone in the community the opportunity to come together and see what the future of sheet metal working looks like. EuroBLECH offers its visitors the possibility to find solutions for the recent challenges in the industry and connects them with businesses from all over the world to help them integrate the latest machinery and software into their manufacturing process. An event that can’t be missed!”, says Evelyn Warwick, Event Director of EuroBLECH, on behalf of the organiser Mack-Brooks Exhibitions.
EuroBLECH is the must-attend event for design engineers, production managers, quality managers, buyers, manufacturers, technical directors and experts from associations and R&D in order to discover the latest trends and machinery in sheet metal working. Visitors to this year’s show can expect the complete spectrum of intelligent solutions and innovative machinery for modern production in sheet metal working, which are presented in form of numerous live demonstrations at the exhibition stands.
“With international travel restrictions to enter Germany from abroad fully lifted, we can’t wait to welcome back our international audience to the world’s leading sheet metal working technology exhibition. Our exhibitors are already busy preparing their participation for the long-awaited return of the show in October. Equally, we are getting a lot of requests from visitors planning their trip and visa”, concludes Evelyn Warwick.
Visitor Information
EuroBLECH is the largest exhibition for the sheet metal working industry worldwide and is the marketplace to discover and source the latest innovative manufacturing solutions. Numerous live demonstrations at the exhibition stands offer trade visitors the opportunity to experience machines and systems from all areas of sheet metal working in action. The EuroBLECH exhibition profile covers fifteen technology sectors and therefore covers the entire sheet metal working technology chain: sheet metal, semi-finished and finished products, handling, separation, forming, flexible sheet metal working, tube/ section processing, joining, welding, additive manufacturing, surface treatment, processing of hybrid structures, tools, quality control, CAD/CAM/CIM systems, factory and warehouse equipment as well as R&D.
The exhibitor list, available on the EuroBLECH website, is regularly updated and provides plenty of information on exhibiting companies, such as exhibitor profiles, company videos and contact details. The EuroBLECH e-news, which is sent out frequently ahead of the show, offers the latest news about the event, the exhibitors and the industry sector. The subscription form for EuroBLECH e-news is also available on the website www.euroblech.com. On social media, EuroBLECH can be followed on LinkedIn and YouTube. The official hashtag is #euroblech.
EuroBLECH 2022 will be held in halls 11, 12, 13, 14, 15, 16, 17, 26 and 27 at the Hanover Exhibition Grounds in Germany. The opening times are from Tuesday, 25 October 2022 to Friday, 28 October 2022, from 9:00 to 18:00. The ticket shop is now open for visitors to purchase their tickets to the event ahead of the show. International flight connections, as well as the excellent local infrastructure make the venue in Hanover easily accessible by plane, car and public transport.
Visitors requiring a visa to travel are recommended to start their preparation as early as possible. Further information is available in the Travel hub on the website. Further detailed information about the exhibition, as well as travel and accommodation, is available on the show website www.euroblech.com.
To meet market demand, smaller double-sided four corners designed BLMP 04 inserts have been launched for small and high feed machining applications.
The smaller size inserts mean more inserts can be mounted to the same diameter cutters, which will greatly improve productivity over the existing BLMP 06 type under similar conditions. Available in Ø8(1z) and Ø10(2z)sizes, these are an alternative to solid end mills for roughing operations.
While both the BLMP 11 and BLMP 13 cover a similar machining range, the BLMP 11 inserts give an advantage as they make it a finer pitch same diameter cutter for better productivity.
The cutters come in all types: face mill, end mill and modular types.
As part of the new campaign, the design for the new CHASE-4-FEED line highlights TaeguTec’s new direction, while the new CHASE-4-FEED logo will be applied to the BLMP 06, 09 inserts and cutters as well.
For more information please contact TaeguTec – Tel: 011 362-1500.
With the recent addition of the SBMT 06 small insert to the existing 09 and 13 size inserts, the CHASE-FEED line has been expanded.
The SBMT 06 insert is suited for low depth of cut operations, such as less than 1 mm, while the finer pitch cutters, with more teeth, improve productivity. In addition, the smaller insert has a large 3 mm thickness and high helix cutting edge, which enhances rigidity and results in excellent performance.
The SBMT 06 insert line includes cutters in end mill -, modular and face mill types, while end mills and modular types are available in the 16-32 mm range and face mills in a 32-63 mm diameter range. All SBMT 06 line tool holders are coolant capable, due to their built-in through hole design.
The SBMT 06 inserts are available in 2 geometries, such as ‘M’ for general purpose, ‘ML’ for difficult-to-cut materials, including stainless steel, heat resistant alloy and unstable conditions.
For more information please contact TaeguTec – Tel: 011 362-1500.
NEW FAMILY OF FAST FEED MILLING CUTTERS CARRYING TANGENTIALLY CLAMPED RHOMBIC INSERTS
ISCAR is introducing a new family of high feed shell mill cutters carrying tangentially clamped rhombic inserts with 4 cutting edges. The new cutters have been designed for roughing operations of cavity and pocket milling in the die & mould industry and for general engineering.
The FFV D…-R-VN07 tools are available in shell mill configurations in a diameter range of 40 to 100 mm and can be applied up to 1.5 mm depth of cut.
Featuring a 16˚ lead angle, R2.8 mm programming radius, strong dovetailed insert clamping, and ramp down and side plunging capability, the tools enable high metal removal rate due to the small entrance angle, which allows high table feed at shallow depths of cut. Coolant holes are directed effectively to the cutting zone and a new polished coating for smooth chip flow and protection against corrosion and wear.
The new tangentially clamped FF VNMT… inserts are available with two types of cutting geometries for optimal machining of a large variety of engineering materials: “ER” for general applications and “ETR” with reinforced cutting edges for interrupted cut and unfavourable conditions. The main application field is rough- and -semi-finish milling of sculptured surfaces and steep profiles, including up-and down-ramping.
For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997-2700.
A serrated cutting edge of HELI3MILL inserts enables high-performance milling of non-ferrous materials.
In milling applications, 90° cutters are perhaps the most common tools. These versatile tools are used for milling square shoulders, slots, face operations bound by shoulders, edges, pockets, and cavities. Face mills perform machining by ramping and turn-milling. These 90°cutters prevail in the product range of tool manufacturers that produce general-purpose mills whether indexable, solid, or brazed.
In selecting 90°milling cutters, there are several factors to be examined such as the material to be machined, the removal of stock, required accuracy, surface finish, stability, and the characteristics of the machine tool in use. These factors influence the cutter type, cutting geometry, tool configuration, and more. The same factors are also the key points for choosing a cutter design on behalf of a tool manufacturer intended for its production processes. For example, solid mills provide ultimate machining accuracy while an indexable tool concept enables machining under heavy loads and provides additional cost-effectiveness per cutting edge. The cutting geometry of solid and brazed mills becomes complete only after grinding. In indexable mills, the shape of a sintered insert is the key contributing factor to achieve optimal tool geometry.
A quantum leap was achieved in the world of metalworking during the early 1990’s with the introduction of the ISCAR HELIMILL – a family of 90° milling tools that introduced helical shaped edged inserts. A highly effective edge was generated by the intersection of the insert’s top (rake) face and the helical insert side (relief) surface. This milestone geometric design formed a constant positive rake and a constant relief along the length of the insert’s cutting edge. The ground-breaking feature caused a significant reduction in power consumption and ensured a very smooth cut. ISCAR’s HELIMILL concept heralded a new design approach and benchmarked indexable milling by anchoring the geometry of an insert at the forefront of milling technology.
A polygon comprises the shape of inserts in 90° milling cutters. These inserts may be rectangular, square, parallelogram, rhombic, triangular or trigon (broken triangle). The shape of an insert determines the number of indexable cutting edges. There are additional important insert features, which relate to the insert’s shape. A square or triangular insert features greater width compared to a rectangular insert shape. Increasing the insert width facilitates a larger central hole and enables using greater clamping screw sizes to improve the securing function of an insert. However, increasing the insert width limits the minimal diameter of a milling cutter and requires larger chip gullets, which reduce the strength of the cutter body. This is just one factor to consider when designing 90° milling cutters with indexable inserts. At the same time, there are other contributing elements such as the mounting method (radial, tangential), range of corner radii, a wiper flat, chip splitting functions, and more. It is imperative to consider the type of material being processed and the type of milling operation for which the cutter is designed.
A parallelogram shape provides an optimally harmonious combination of the cutting-edge length, varied corner radii, ramping-down capabilities, and additional parameters of the cutting geometry and insert strength. This explains why the parallelogram shape remains common. A significant disadvantage of the shape is the number of cutting edges – limited by two in a traditional design configuration. A double-sided, reversible insert concept seems to be the simple way to increase the number of edges on an insert more effectively. There are additional attributes to think about when considering a double-sided insert configuration. Additional limitations affect the relief angle and increase the axial rake of a milling cutter after the inserts are assembled on the tool body.
The examples mentioned must be considered when developing indexable milling cutters. The careful study of contributing factors and understanding the relationship between the intricately engineered elements can lead to a winning tool solution. To provide a wide array of solutions for 90° milling cutting tool manufacturers develop multiple cutter shapes and innovative single- and double-sided indexable inserts.
With the many forms and shapes of cutters in the tool market, the creation of new geometries has become an obsolete task. ISCAR’s NEOLOGIQ campaign has given birth to unique innovative milling solutions in aim to conquer new quests for fast and productive milling solutions.
The combination of a square profile with specially shaped rake and side faces is a design feature of cost-effective NEODO S890 inserts.
ISCAR’s prolific R&D design engineers invented the new NEODO S890 milling cutters designed for rough, semi-finishing, face and square shoulder milling operations primarily for steel and cast iron. The 90° cutter design places cost-effectiveness and productivity at its forefront, intended for milling under unfavourable conditions. The tool utilizes a strong-structured double-sided insert. The insert features a square profile, while the top, bottom and side face of the insert are specially shaped by ISCAR’s unique pressing technology. This provides 8 helical right-hand cutting edges, 4 from the top and 4 from the bottom. When mounted on the cutter, the insert guarantees positive radial and negative axial tool rake angles, which promise smooth cutting and reduced power consumption for milling under diverse machining conditions and interrupted cuts. A dovetail profile of the insert pocket enables very rigid clamping that substantially increases cutter stiffness. The insert has a built-in wiper flat to improve surface finish. A new look on a square insert profile in combination with the advantages of pressing technologies has resulted in effective and economical solutions for face milling, particularly for machining close to shoulders where work holding constraints exist.
The double-sided 90° HELIDO Trigon tool was derived from a trigon shape.
A double positive cutting geometry characterizes HELIDO Trigon milling cutters that carry double-sided inserts of a “broken-triangle” profile.
The insert configuration provides 6 indexable cutting edges and ensures higher tooth density for increased feed rate and maximized productivity. The tools have a double-positive cutting geometry: positive axial and radial rake angles. These attributes contribute to lower power consumption and allow rough milling applications on machines with limited power. The versatile HELIDO Trigon tools are suitable for milling shoulders, slots, side plunging and ramping by use of helical interpolation. The main advantage of these tools is the combination of 90° profile accuracy, productivity, and cost efficiency.
Efficient milling of aluminium alloys and other non-ferrous materials (ISO N group of application) requires a sharp cutting edge and a polished rake face. The chip-splitting capability of a cutting edge is an additional tool to improve performance. The serrated edge geometry of the single-sided triangular HELI3MILL inserts, which have proven themselves as real workhorses in 90° milling, are cost-effective tools.
Given case studies convincingly confirm the conclusion that the possibilities for improving 90° indexable milling cutters are not exhausted. A fresh right-angle on the cutter design will lead to an attractive solution, even when considering the redundancy in developing new insert geometries.
A serrated cutting edge of HELI3MILL inserts enables high-performance milling of non-ferrous materials.
For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997-2700.
A Micro 90 coolant-driven high-speed compact spindle ensures extremely high rotating velocities.
“Where Innovation Never Stops!” is the slogan that appears on the walls of the production facilities at ISCAR headquarters and has been synonymous with the company for several decades.
The COVID-19 pandemic did not interrupt the innovation process, and between 2020 and 2021, ISCAR introduced the NEOLOGIQ marketing campaign comprised of advanced cutting tools and tooling solutions for modern metalworking. The significant changes in manufacturing, such as intensive digitizing, the shift to electric drive in the automotive industry, and growing precise workpiece fabrication, have emerged new demands for cutting tools. Notwithstanding, the accelerated pace of changes sharpens the demands and requires more ISCAR NEOLOGIQ products that answer to modern age machining. “Machining with No Boundaries” is the NEOLOGIQ mindset.
Holemaking news
CHAM-IQ-DRILL, the family of assembled drills that mount exchangeable carbide heads, is now upgraded with new heads in the diameter range of 33-40 mm. These heads can be mounted on any drill possessing the appropriate pocket size. The main feature of the new heads is a multifunctional cutting geometry, which enables effective drilling of various engineering materials such as steel, stainless steel, heat-resistant special alloys, and titanium (ISO P, M, and S groups of application) assuring hole precision within IT10-IT9 accuracy grades. ISCAR’s customers will benefit from using the new heads which guarantee to maintain less stock of tools for machining diverse materials.
3-flute LOGIQ3CHAM drills provide nearly flat bottom holes.
The ISCAR LOGIQ-3-CHAM is also based on the concept of exchangeable carbide heads with 3 flutes for improved productivity and is now supplemented by new carbide heads for achieving a nearly flat bottom hole. Flat bottom holes are necessary for screw head sockets, spring seats, washer ports, etc. The heads ensure drilling up to an 8-hole depth-to-diameter ratio without a pre-hole. The new design facilitates generating holes with a nearly flat bottom by use of a single pass. The heads are mounted on existing LOGIQ-3-CHAM tools that significantly expand the application range of the family and reduce inventory costs.
So, how do you increase the drilling depth? Use a longer drill?
MODUDRILL is a family of modular drills with replaceable carbide heads that carry indexable inserts and provide an alternative solution. Mounting an exchangeable extension holder on a drill body increases the drilling depth by an additional 200 mm when machining holes in a diameter range of 33-40 mm.
In high-speed reaming, a combination of a carbide reaming head with a rolling device in one single tool results in a short operational time for achieving accurate hole diameter along with a mirror-like surface finish.
Key aspects in turning
A NEOSWISS turning tool carries a quick-change head with indexable insert.
A modular tool concept is the way to reach high versatility. NEOSWISS, a new tool system with quick-change heads, follows this concept. There are different types of heads for indexable inserts. The system is suitable for turning, parting, grooving, and threading applications. By use of a unique high-clamping-force mechanism, the heads are mounted on a toolholder. The mechanism provides an accurate cutting edge position each time and utilizes high position repeatability. The system intended mainly for Swiss-type machines enables removing heads and replacing inserts within the tight confines of CNC machining centers.
ISCAR has developed a new lever dual lock securing mechanism for improved clamping rigidity intended for ISO turning inserts. The new design, referred to as the COMBI-D-LOCK family, combines the advantages of two conventional clamping methods by the use of a lever and a top clamp. An insert is locked in two directions from the top and the bottom. This provides better stability and rigidity, and in comparison, to the conventional lever improves tool life and increases productivity.
LOGIQ-F-GRIP features a new highly advanced tool family for parting solutions. The central component of the family is a robust tool block that mounts a 4-pocket adapter. There are cases when the rib, a reinforcement element of the block, interferes and prevents clamping the block on typical turret positions. NEOLOGIQ overcomes this problem by providing additional blocks with the rib placed on the alternative side of the block. The revolutionary LOGIQ-F-GRIP parting system was designed to achieve extra stability and vibration-resistant high productivity parting and grooving operations. The highly engineered LOGIQFGRIP is an assembled tool block that comprises a unique durable holder and a high-stiffness quad blade with pockets for mounting inserts.
Innovations in milling
NEODO S890 is a family of 90° indexable face mills for rough and semi-finishing operations. The mills mount durable square double-sided inserts with 8 cutting edges. NEODO S890 facilitates face and square shoulder milling while providing an additional option for milling close to shoulders where there are workpiece or work holding fixture constraints. ISCAR customers have requested additional corner radii and tool diameters, therefore, this tool family was expanded with additional pressed-to-size inserts with a 0.8 mm corner radius and cutters in diameters 32 and 25 mm including endmill design configurations.
A 90-degrees NEODO S890 face mill.
A durable double-sided round insert is now available. The combination of an innovative pocket design and a special peripheral shape of the insert provides reliable insert clamping and fail-proof insert indexing. Depending on the depth of cut, there are up to 6 insert indexes on each side (up to 12 indexes total). When indexing, there is no need to remove the insert clamping screw. The main application of the new cutters is for rough and semi-finish milling complex surfaces, especially in die and mold, power generation, and aerospace parts.
The range of solid carbide endmills has been expanded by adding new tool diameters and corner radii.
Upgrading toolholders
A Micro 90 coolant-driven high-speed compact spindle ensures extremely high rotating velocities.
ISCAR SPINJET, a family of coolant-driven high-speed compact spindles for small diameter tools, intended to upgrade existing machines to high-speed performers, is now supplemented with Micro 90 intended for miniature rotating tools in milling, drilling, countersinking, thread milling, engraving, chamfering and deburring operations. Micro 90, made of a solid titanium shell and assembled from only six parts, enables rotating velocities that range from 35000 to 53000 rpm while the main machine spindle remains idle.
The chuck thickness is a factor that limits the working space of a tool. This factor often causes increasing the tool overhang to reach a machined surface. A novelty in X-STREAM, a family of thermal shrink toolholders, is a series of slim design chucks to eliminate such a restriction. The new chucks follow ISCAR’s coolant jet channel technology providing direct coolant supply to the tool cutting edge.
Changes in metalworking technology place new demands on cutting tools. To meet these demands, cutting tool manufacturers develop new products to assure increased performance. The industries’ response to the products sprouts new requirements.
ISCAR’s NEOLOGIQ campaign is based on new tools that were developed in accordance with customers’ input. You can expect more NEOLOGIQ sequels to assure advanced machining in the new era of metalworking.
For more information, please contact ISCAR South Africa (PTY) LTD – Tel: 011 997-2700.