Home Blog Page 73

System Driven Strengths

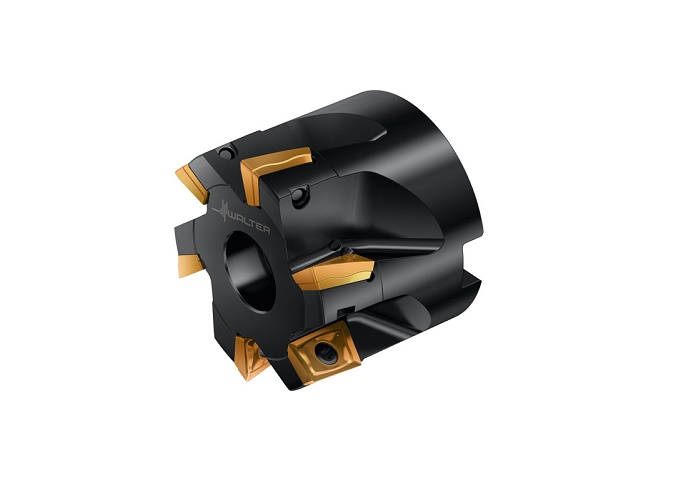
Walter AG is presenting a shoulder milling cutter that is a logical continuation of the M4000 system concept in the form of the M4130. The idea behind this is to reduce costs through the ability to use universal system inserts in different applications and tools. In the case of the M4130, this applies to the system inserts with rhombic basic shape and a 15° clearance angle, which can also be used either in the routing cutters or porcupine milling cutters from the M4000 range. The double-edged inserts with sintered circumference are available in three sizes each with three CVD-coated and three PVD-coated grades. In addition to its high level of flexibility, it also stands out thanks to its cost efficiency.

According to Walter, their soft cutting action makes the M4130 shoulder milling cutters ideal for roughing operations involving steel, cast iron, stainless steels and materials with difficult cutting properties and are also capable of plunge milling. Specifically, these operations are shoulder milling, ramping, pocket milling and circular interpolation milling. The milling cutter with a 90° approach angle is available as standard with depths of cut of 8, 13 and 16mm, in the 16–100mm diameter range. It is also available as a special tool in a considerably wider diameter range. The M4130 milling cutter is part of the Walter Xpress fast delivery range and is manufactured in a CO2-compensated process.

For more information, please contact Spectra Carbide – Tel: 0860 23 23 23.

High Performance Taps

NORIS taps for processing a wide variety of steel alloys, cast iron and various nonferrous alloys are well known under the names SALOREX UNI for blind holes and STABIL UNI for through-hole. REIME NORIS now extends the UNI series to high performance taps made of HSSE-PM (HSS-PS) with improved cutting geometry and TiCN coating.

NORIS SALOREX UNI – the specialist for deep blind hole threads up to 3 x D thread depth – has 42° right-hand helix flutes. These provide secure chip removal against the cutting direction.

NORIS STABIL UNI stands for the production of through hole threads up to 4 x D thread depth. The special STABIL-flutes move the chips in the cutting direction. The drills are available in metric sizes from M3 to M20 and M8 x 1 to M16 x 1,5 in stock. In both versions, the use of powder metallurgical high-speed steel permits higher cutting speeds while increasing tool life.

The user benefits by increasing the cycle times and a reduction in tool costs. With the ability to process a very wide range of materials, additional cost of storage and tool investment can be reduced. The proven cutting edge geometries were further optimized in detail. They are specially adapted to the characteristics of the HSSEPM substrate and the coating.

REIME NORIS thus promises significant performance gains and expects especially in the production of small- and medium-sized series, the greatest economic advantages of using these high performance taps.

For more information, please contact Duncan Macdonald – Tel: 011 444-4345.

Even Better Groove Milling

Trouble-free precision groove milling in an easy-to-use format is what manufacturers are set to enjoy by using the latest CoroMill® 331 indexable insert cutter from cutting tool and tooling systems specialist Sandvik Coromant. New features set to deliver multiple advantages to customers include internal coolant and light cutting geometries for stable and secure machining.

“We have introduced a number of new features that help meet customer demands such as process security, component quality and cost,” explains Jenny Häll, Product Manager Groove Milling at Sandvik Coromant. “Arguably most notable is the addition of internal coolant, which helps regulate heat in the cutting zone for long and predictable insert tool life. This factor is especially beneficial in ISO M and ISO S materials [stainless steel and heat-resistant alloys], which exhibit poor thermal conductivity. Additionally, internal coolant provides excellent chip evacuation, a key factor for groove quality and process security.”

Enhanced process security promotes trouble-free machining, a factor that is further supported through the introduction of light cutting geometries. For ISO M and ISO S materials, L30 and L50 geometries replace the company’s existing assortment for good conditions/light applications and tougher conditions/heavy applications respectively. For ISO P (steel) and ISO K (cast iron) materials, the M30 geometry now complements the existing assortment. M30 is purpose-designed for the delivery of secure machining where weak set-ups and long overhangs are present.

Another factor underpinning process security is enhanced cutter rigidity. In applications where long overhang or elevated levels of vibration are likely to be present, CoroMill 331 can be deployed with Silent Tools™ damped adaptors. Here, the shorter arbor cutter bodies of CoroMill 331 bring the cutting edge closer to the Silent Tools damping mechanism, thus providing an even more stable tool with a reliable performance.

Extra process security and stability deliver higher component quality to manufacturers in industries such as energy, aerospace and automotive. Typical parts to benefit include hour glass valve bodies, aerospace brackets, flap tracks and steering knuckles, to list but a few. CoroMill 331 offers high levels of versatility that render it suitable not just for groove milling, but for parting, double half-side machining, shoulder milling, face milling, back-face milling, gang milling and circular interpolation.

Better security in machining also promotes productivity. CoroMill 331 offers true 90° corners and excellent metal removal rates that make this cutter the most productive of its kind.

Ease-of-use is a further requirement of machine shops the world over. For this reason, CoroMill 331 makes use of spring-loaded cassettes with serrations that provide security and easy setting for the desired width. Moreover, a pin-controlled adjustment range enables manufacturers to set the cutter with high accuracy for precise groove dimensions.

Available is a wide range of tools in an extensive choice of diameters, widths, insert geometries, corner radii and grades, along with a large selection of mounting options.

For more information, please contact Sandvik Coromant – Tel: 011 570-9615.


IC882 And IC5820 New High Performance Milling Grades For Machining Titanium, Stainless Steel And High Temperature Alloys

Today, as more and more titanium parts are necessary for the construction of modern airplanes, the aerospace industry is in constant demand to increase cutting tool performance for machining titanium. To comply with this high market demand, ISCAR introduces new IC882 and IC5820 carbide grades that feature a more productive means of machining titanium alloys.

These include the common Ti6Al4V and tougher, harder to cut titanium alloys such as Ti-5Al-5V- 5Mo-3Cr (Ti 5-5-5-3), Titanium Ti-10V-2Fe-3Al (Ti 10-2-3) and other super alloys.

Grade IC882 features a particularly tough and strong substrate. The fracture toughness (K1c) that measures the resistance of material to the propagation of a crack in the substrate is at least 20% higher when compared to competing carbide grades. The IC882 with its tough carbide substrate, new PVD hard coating and SUMO TEC® post-coating treatment substantially improves impact strength, hot hardness, oxidation resistance, notch wear and built-up edge resistance; all contributing to longer tool life, reliable results on wear and chipping resistance for higher metal removal rates and reduced production costs per part.

The new IC882 grade is intended mainly for machining titanium alloys and heat resistant steels. In addition, it can be used successfully for milling stainless steel and high-temperature super alloys (HTSA) at medium to high cutting speeds, even under unfavourable machining conditions or interrupted cuts. The ISO application range of grade IC882 is M25-M45 / S20-S30.

Grade IC5820 has a very tough, strong carbide substrate combined with CVD new hard coating and SUMO TEC® post coating treatment. It features a substantially improved impact strength, higher hot hardness, oxidation, notch wear and built-up edge formation resistance. These contribute to longer tool life, reliable wear and chipping resistance. The IC5820 grade enables the increase of cutting speeds that result in higher metal removal rates and reduced production cost per part; it is mainly used for milling titanium alloys.

The ISO application ranges of grade IC5820 are M20-M35 / S15-S25. With 20% – 30% higher cutting speeds vs. existing known carbide grades, the grade requires high flow rate and pin-pointed coolant; its best performance can be achieved with highpressure coolant.

For more information, please contact ISCAR South Africa – Tel: 011 997-2700.


Indexable Tools Challenge Solid Carbide For Small Diameters

Solid carbide tool accuracy compares favorably with that of indexable tools, particularly for small-diameter endmills and for tools with diameters beyond the range. However, the role of reduced accuracy for tools of small diameter (for example, a milling cutter’s radial runout) increases in significance as a factor affecting tool life.

An indexable tool is made up of a tool body, replaceable inserts and mechanical parts such as clamping screws or wedges, which secure the inserts in the body. Decreasing the tool diameter necessitates reducing dimensions of the assembly components. Reducing the size of the securing elements leads to weakening their strength and the tool becomes unable to withstand cutting loads under normal machining data. This seriously limits the tool application; further decreasing may cause degradation of the entire assembly structure.

The prices of small rotating tools are often high compared to the assembled concept, which adds to the perceived limitations of indexable tools in the small diameter range.

The Indexable Option.

Indexable tools possess several distinct advantages that makes applying these tools within the above range very attractive in the eyes of the customer. In many cases, especially in rough machining, changing a worn cutting edge by simple indexing provides economic benefits compared with having to replace a whole life-expired solid tool with a new tool. In addition, there is no need to use up time and resources on regrinding and recoating worn-out onepiece cutters.

Tool manufacturers have made significant progress in developing reliable designs thatcould be commercially viable against the solid carbide concept. Work in this direction has shown results already and assembled mills and drills with interchangeable cutting heads are proving to be a realistic alternative to solid carbide tools.

Competitive Performance

The introduction of tools with replaceable solid carbide cutting heads signifies a change in focus. ISCAR provides two examples of this concept with the ISCAR MULTI-MASTER milling line and the CHAMDRILL line in drilling.

Performance and accuracy characteristics have positioned the new tools to be functionally competitive with solid carbide designs. Versatility of these lines, where a head can be mounted in different bodies and vice versa where a single body can carry different heads, facilitates various assembly combinations and contributes to reducing items in tool stock.

Another important design approach – “no setup time” – characterizes these lines, as a wornout head does not require spending time on set-up and can be replaced while the tool is still clamped in the machine tool spindle. This cuts cycle time and consequently, reduces production costs. In contrast, replacing a worn-out solid carbide mill or drill inevitably leads to a new set-up procedure.

In addition, the concept ensures sustainable use of cemented carbide with all the associated advantages. The principle of indexable carbide tools has distinct merits and features strongly in tool design within the diameter range that is under discussion. The minimal diameter of MULTI-MASTER milling heads is 5mm and that of SUMOCHAM drilling heads is 6mm, while the MULTI-MASTER combined countersink heads for center drilling feature a minimal 1mm diameter.

The LOGIQ factor

ISCAR has recently introduced a new range of small-size indexable rotating tools under its new LOGIQ line campaign. The company proposes several families of cutters with a nominal diameter of up to 20 mm. A brief look at some of these families can provide a clearer understanding as to whether the new tools will be able to breach the solid stronghold wall.

The new families of indexable milling cutters within the diameter range of 8-16 mm attract the most interest. They have several common features: the cutters carry triangularshape inserts with 3 cutting edges and the mechanical part that secures the inserts is represented by a screw. These families are intended for milling square shoulder or fast feed (high feed) milling. But here the similarity ends, and the difference begins. While the design of the HELI3MILL and MICRO3FEED families for tool diameter 10-16 mm is committed to the classical principle of insert securing, by clamping screw through the central hole of an insert, the NANMILL and NANFEED families for tool diameter 8-10 mm have adopted another concept.
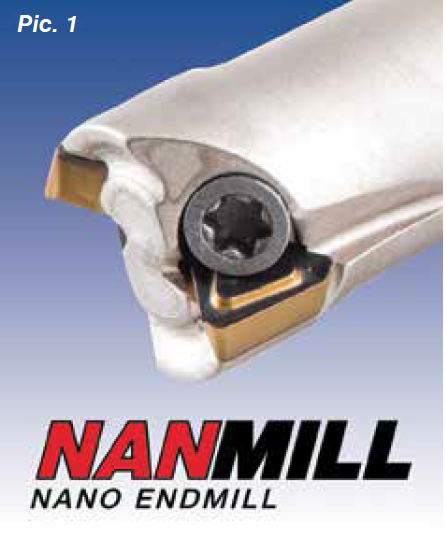
Within such a small diameter range, the central clamping screw, as noted previously, does not provide an acceptable solution. According to the new concept, the screw is located above the insert, and the screw head plays the role of a wedge (Pic. 1). This approach provides reliable and rigid clamping, ensures a durable homogeneous insert structure with no hole, and allows insert indexing to be quick and simple.

It is predicted that these new families will be particularly effective in manufacturing compact parts and in machining smallin- size cavities, pockets and small parts utilized in industrial sectors such as die and mold making, as well as in producing miniature components.
Small change, large impact

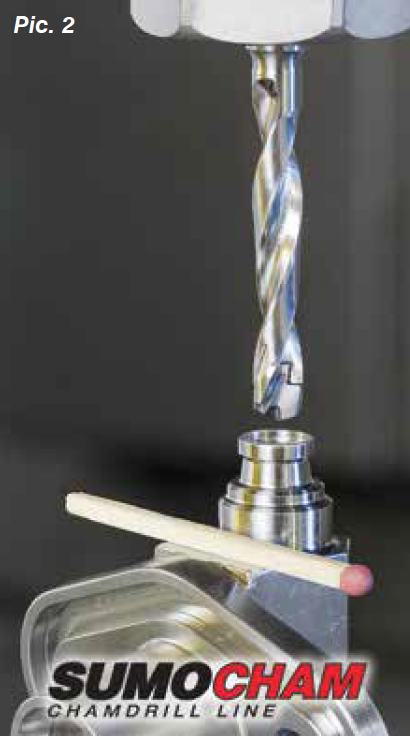
A 1mm change in size: is this a lot or a little? For indexable tools in the small diameter range, it makes a noticeable difference. ISCAR’s new SUMOCHAM 5mm diameter drilling head represents an important step ahead in expanding the application fields of indexable drills (Pic. 2).

Within the small diameter range, indexable tools can offer precision and performance advantages that position them competitively against the more traditional solid carbide tools. Indexable tools are beginning to shear their way into metalworking practices – and the industry is taking note.

For more information, please contact ISCAR South Africa – Tel: 011 997-2700.

 

Hyundai WIA XF6300 5-Axis VMC

XF6300 is a 5-axis vertical type machining center designed by European R&D center in Germany.

The XF6300 comes with a 19″ large monitor for enhanced visibility and the SIEMENS ShopMill customized technology package as standard.

ShopMill provides simple operation, supporting all operator actions with graphic help displays and functions for quick and practical machine setup, including calculating the workpiece position in the machine. The control panel has the same configuration as a computer keyboard for easy usage. Mold Package is provided as standard for a highly efficient mold process with the aid of various NC options and automatic tool measurement.

While the integrated bed and column have been designed by using HYUNDAI WIA’s unique analysis method, the XF6300 features a 4-way structure box type saddle inside the cross-beam to increase stiffness and minimize thermal displacement. The Box-in-Box structure design accomplishes thermal equilibrium, while minimizing thermal deformation. The direction of the main axis’ center of gravity and z-axis moving direction are in the same line, providing more precise machining.

The XF6300 features X-axis 650mm, Y-axis 600mm and Z-axis 500mm with 60 m/min rapid traverse and 1G of X/Z-axis acceleration and deceleration and a linear scale to all linear axes plus rotary scale to rotating axes as standard.

Various multipurpose built-in spindles are available, providing 15,000 rpm or optionally 24,000 rpm and 40,000 rpm for high quality mold machining. The main spindles produce almost no noise and vibration even at high speed machining, while ensuring highly stable machining performance.

The XF6300 main spindle features an oil cooling device as standard promoting high accuracy for long periods of time and a HSK tool holder for high positioning accuracy and precision.

The XF6300 is designed with a 5-axis rotary table which can be moved 30 degrees to the front side of the machine and 120 degrees to the rear side of machine based on A-axis and C-axis and can rotate 360 degrees. A-axis and C-axis achieve 70rpm and 110rpm, respectively.

The HYUNDAI WIA Europe R&D Center has also developed a racktype magazine providing various options. XF6300 is equipped with 34 tools, which has a single layer as a standard. Tool magazines can be upgraded to accommodate 68 tools and 102 tools, respectively.

For more information contact Rothco – Tel: 011 970 1930

Hurco Introduces Double Column Bridge-Type Machine

The stability of the BX40i double-column bridge-type CNC machine design and the overall weight (20,062 lbs.) provide exceptional accuracy and outstanding surface finish capabilities.

While designed specifically for the mold market and aerospace industry, the BX40i meets the needs of any high speed machining application that requires tighter tolerances while allowing the machine to operate at optimum spindle speeds.

With the double-column design, there is less tool deflection and less vibration compared to a single column CNC machine and less thermal deformation due to the fact that the heat only affects the bridge structure in a straight line instead of occurring on both the X and Y axes. Another advantage is the fact that the spindle is closer to the mass of the machine on a double-column machine, which provides increased rigidity. Additionally, the BX40i is built with size 45 roller rails on all axes and linear scales are standard.

The Hurco BX40i differs from other bridge type CNC machines due to the integrated Hurco control powered by WinMax® control software and the patented motion system called UltiMotion®. The flexibility of the Hurco control makes machinists more productive and job shops more profitable because it supports multiple programming methods: conversational programming that minimizes idle time that occurs when waiting for the CAD/CAM station; industry standard NC programming; and a Hurco specific feature called NC/Conversational Merge that optimizes efficiency even further.

UltiMotion is the sophisticated motion control software system Hurco invented that determines the optimal trajectory to run the tool and achieves programmed feed rates more consistently, reducing cycle time by as much as 30 percent or more, depending on the complexity of the part, while improving surface finish quality. With UltiMotion, cornering velocity is 2.5 times faster than conventional motion and machine jerk is reduced by at least 50 percent. Instead of fixed look-ahead, UltiMotion includes dynamic look ahead that is smart enough to adapt as required by the tool path. UltiMotion is different than the smoothing features offered by CAD/CAM software and improves upon even excellent CAM output because it provides better handling of the machine mechanics and dynamics. All Hurco CNC machining centers are equipped with UltiMotion.

BX40i specifications:
Table Size: 41.3″ x 27.6″
Table Load: 2,204 lbs
XYZ Travels: 27.6″ x 40.2″ x 19.7″
XYZ Rapids: 1,535 ipm (Direct Drive Ballscrews)
Spindle Taper: HSK 63A
Spindle RPM: 18,000 (motorized)
Spindle HP: 47
Spindle Torque: 88 ft-lbs @ 2,800rpm
ATC Stations: 30
Machine Weight: 20,062 lbs

For more information contact Hurco – Tel: 011 849 5600

Okuma’s Genos M560-V With Larger Work Envelope

The GENOS M560-V vertical machining center, combines a high column design and CAT 40 BIG- PLUS® spindle to cut large, complex parts.

The larger work envelope minimizes restrictions on workpieces, tool lengths and the rotary table. A highly rigid, thermally-stable, double-column construction gives this CNC machine the ability to withstand thermal deformation, resulting in improved machining performance. It’s also one of the heaviest machines in its class.

A powerful 30 hp spindle with 146 ft. lbs. of torque allows this machine to cut challenging metals such as titanium and Inconel as well as stainless steel and aluminium. A separate automatic tool changer door makes tool changing seamless without interrupting the machining process. The table moves only in Y, while the spindle moves in X & Z, enabling a smaller machine footprint, rapid feed rates, precise cutting and smooth surface finishes. Coupled with a user-friendly design and energy-saving technology, the GENOS M560-V truly delivers machining excellence.

Thermo-Friendly Concept, Okuma’s proprietary thermal deformation compensation technology is standard on this machine. Pretension ball screws and bi-directional spindle cooling allow for better control of the machining process. Optional Collision Avoidance and Machining Navi Intelligent Technologies are available.

Key specs of the GENOS M560-V vertical machining center include a max machining volume of 1,050 x 560 x 460mm, table size of 560 x 1300mm and a max. load capacity of 900kg. Add to this a spindle speed of min⁻Å 15,000, spindle motor power of 22/18.5 kW (hp), a rapid traverse of X-Y 40 m/min and Z: 32 m/min and magazine capacity of 32 tools.

For more information contact F&H Machine Tools – Tel: 011 397 4050

Okuma 5-Axis Machining Centres – MU-8000V-L And MU-4000V-L

Both the MU-8000V-L and the MU-4000V-L provide the power of process-intensive machining and high-speed, high-accuracy cutting through a combination of turning and 5-axis multitasking machining.

Okuma’s 5-axis machining centres MU- 8000V-L and MU-4000V-L grant the unrivalled accuracy customers have come to expect from the manufacturer. Both machines are ideally suited for use in die and mould construction, in medical applications or for the manufacturing of very complex aerospace or automotive components. While the MU-8000V-L features a more generous working area, the MU- 4000V-L is smaller in its overall dimensions. Both models deliver high traversing speeds and high cutting performance and offer maximum flexibility in 5-sided or 5-axis simultaneous machining of complex shapes. Process reliability, dimensional stability and geometrical accuracy are ensured thanks to a sturdy portal construction and the Thermo-Friendly Concept. The latter combines control technology and machine design to minimise the amount of heat generated and enable extremely accurate thermal deformation compensation. The MU-8000V-L and the MU-4000V-L are operated with Okuma’s OSP suite, which delivers the best IT-applications in one package.

Plenty of options for specific challenges

Okuma provides several options that can be used on both machines to meet the specific demands of their customers. As part of Okuma’s Intelligent Technology, the 5-Axis Auto Tuning System allows operators to take precision to the next level. It effectively compensates geometric errors that can naturally occur when machining with a 5-axis CNC machine tool – including volumetric accuracy. Adjustments can be performed within approximately ten minutes, whereas manual methods can take several hours.

The system is easy to use and allows the operator to focus on machining. Thus, the 5-Axis Auto Tuning System is an effective way to efficiently prevent problems, such as shape defects in curve machining and steps in slope machining.

All MU-V series machines are fit for options like Dynamic Tool Load Control, the monitoring and skiving functions and the ECO Hydraulic Unit.

For more information contact F&H Machine Tools – Tel: 011 397 4050

Turn & Mill Complete Machining Of Large Workpieces

With the compactMASTER Turn & Mill spindle, the additional turret including Y-axis and a bar diameter of ø 102mm, the new NTX 3000 2nd Generation from DMG MORI combines maximum productivity with a footprint of just 16.5 m2.

Hard on the heels of the NTX 2500 2nd Generation exhibited at EMO 2017, DMG MORI presented the latest model of its compact turning-milling centres in the form of the NTX 3000 2nd Generation at the Open House in Pfronten. This world premiere is designed for larger bar diameters of 102mm and is also capable of machining the most complex of components with a torque of up to 1,194 Nm. As with its smaller siblings, the experience gained from more than 1,000 installed NTX 2000s is also brought to bear in the NTX 3000 2nd Generation. The latest model is therefore endowed with high process stability and flexibility with a generous work area (675mm in the X-axis and ±150mm in the Y-axis) on a footprint of only 16.5m2.

The decisive core component here is the B-axis with the company’s in-house compactMASTER spindle for demanding 5-axis machining with up to 122 Nm. With 1,194 Nm torque and optional counter-spindle, the main spindle extends the performance of the NTX 3000 2nd Generation into the realm of 6-sided heavy-duty machining in the aerospace industry, the automotive sector and medical engineering. Turn & Mill machining centres are in the premier league of modern machining. This is also borne out by the new NTX 3000 2nd Generation from DMG MORI. It is based on the robust machine bed together with stable roller guides. Added to this are comprehensive cooling systems in the spindles and ball screw drives. These ensure stable temperature conditions as a basic prerequisite for precision machining in continuous operation with 5 axes.

A further important criterion of the world premiere is the short, 350mm compactMASTER spindle on the B-axis, which, along with its actual performance data, provides additional space in the working area. Like the Turn & Mill spindle, the second tool holder in the form of a BMT turret with driven tools also has a Y-axis (±40 mm). The company’s in-house toolSTAR tool magazine with 38 stations, which, at the customer’s request, can be expanded to up to 114 pockets, makes for short setup times.

The NTX 3000 2nd Generation embodies the trend towards automation from two  perspectives. While the integral tool measurement and tool breakage monitoring system and tool measurement in the work area ensure efficient machining, a choice of needs-oriented handling systems takes care of tool loading and unloading, the robot version being just one example.

On the control side, the NTX 3000 2nd Generation follows the Path of Digitization, on the basis of which DMG MORI is promoting the digitalization concept. The latest turningmilling centre is therefore equipped with the CELOS APP-based control and user interface and large, 21″ multi-touch display. On the one hand, CELOS enables consistent management, documentation and planning of job orders in production engineering and in the workshop. On the other, CELOS APPs such as CONDITION ANALYZER and PERFORMANCE MONITOR offer the user a detailed insight into the machining processes and the status of the machines as a basis for a continuous improvement process. CELOS works to an ever-increasing extent as an IoT interface and thus provides the basis for cross-company interaction in production networks of the future.

DMG MORI Technology Cycles are also available for the NTX 3000 2nd Generation. Easy Tool Monitoring enables spindle load and axis feed to be monitored. Technology cycles make it easy for operators to carry out demanding machining, setting up and measurement with universal machines as well as standard tools and fixtures. Special machines, programmes and tools were previously necessary for this.

For more information contact Retecon – Tel: 011 976 8600