Home Blog Page 77

Laser Technology: Unique Products Thanks To Laser Texturing


With the innovative LASERTEC Shape technology, DMG MORI has set new standards in the mould making sector.

The laser texturing of geometrically defined surface structures is more environmentally friendly than conventional etching and provides significant design freedom with at the same time highest reproducibility. Furthermore, the surface properties can be influenced in this procedure in a targeted way. Tool and mould makers benefit from this in almost all industries, where products also set themselves apart from the competition with individually designed surfaces: Fittings in the automotive industry, mobile phone cases, jewellery or drinks bottles. The LASERTEC Shape series from DMG MORI provides suitable production solutions. With the LASERTEC 45 Shape, the LASERTEC 75 Shape as well as the large models LASERTEC 125 Shape and LASERTEC 210 Shape, the machine tool manufacturer covers practically all component sizes.
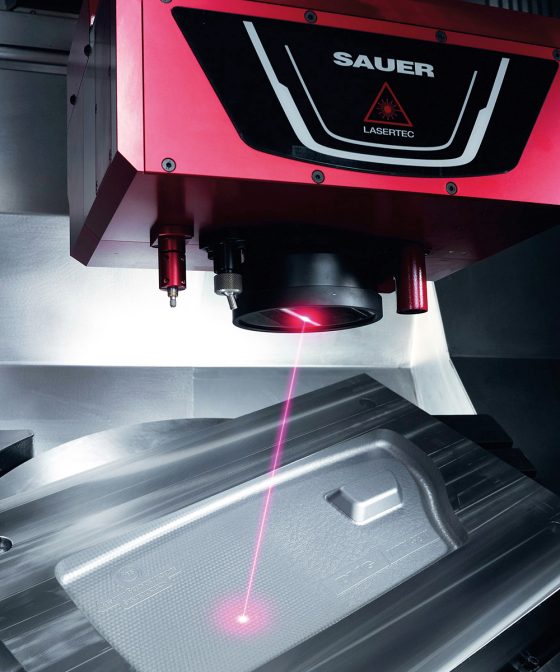
With the innovative LASERTEC Shape technology, DMG Mori has set new standards in the mould making sector – representation of a glove compartment cover with combined honeycomb/leather structure.

The introduction of the LASERTEC Shape technology was a big step for tool and mould makers. Particularly in automotive engineering, there has since been a futureoriented alternative to conventional etching. Other industries benefit from the significantly higher precision compared to conventional milling. Blow moulds for PET bottles, or for example watch faces in the watch-making industry can be equipped with finest structures, but also lettering and engravings.

LASERTEC 75 Shape – state-of-the-art laser and future-oriented software

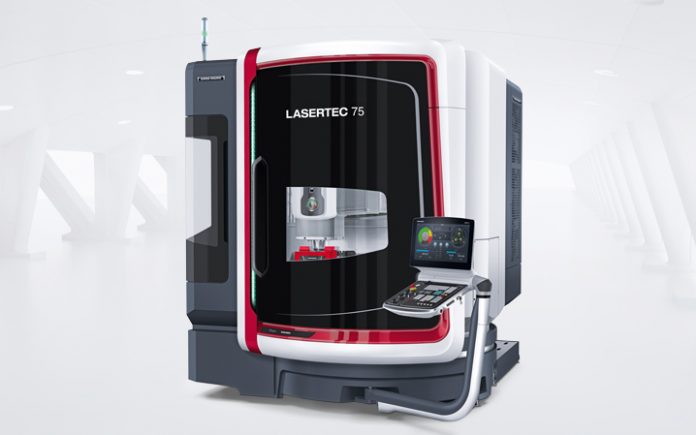
DMG MORI is prepared for this development and has only recently integrated the compact LASERTEC 75 Shape in its portfolio for laser texturing, which is already fully equipped for Industrie 4.0. With a footprint of < 8 mÇ, it is the ideal complement even in tightest production environments. Its ergonomic design with a door opening of 1,310mm provides perfect access to the generously dimensioned work area. Workpieces weighing up to 600kg (with the optional tandem drive up to 1,000kg) with diameters of max. ø 840mm and heights of 520mm find sufficient space here. The traverse paths are 750mm x 650mm x 560mm in the X, Y and Z axes.

The core elements of the LASERTEC 75 Shape are the powerfully pulsed 100 W fibre laser and the 3D processing optics. These are responsible for the material removal by 3D laser in layers and in combination with the NC swivel rotary table, provide contourparallel laser shaping. This enables fast and smooth laser texturing also for 3D free-forms.

When it comes to the control system, DMG MORI relies on a SIEMENS 840 D solutionline for the LASERTEC 75 Shape. Combined with CELOS, the machine can also be optimally integrated into the company organization. User-friendly and applicationrelated LASERSOFT software features ensure simple and productive operation of the LASERTEC 75 Shape.

For more information, contact Retecon – Tel: 011 976 8600
Laser Technology: TRUMPF – Laser Welding Saves Time And Money

One of TRUMPF’s goals at the Schweißen und Schneiden welding trade fair in Düsseldorf was to demonstrate how lasers can facilitate the welding process.

“Laser welding may not be able to replace every MAG weld seam, but it offers plenty of advantages in the cases where it can,” says Thomas Rupp, Head of Sheet Metal Laser Welding at TRUMPF. The ongoing trend towards greater product customization poses a challenge to companies as they seek ways to produce small batches more efficiently. Cost per part is a key factor – and one way to reduce it is by minimizing throughput time. Joining is one of the steps that offers particular potential in this regard. Depending on the quality requirements in each case, parts often require several minutes of finishing work to grind down beads on conventional weld seams. That’s where laser welding can make a real difference: whatever the batch size, a laser can reduce the need for post-processing and accelerate the joining process. Investments in this technology quickly pay for themselves, even with small batch sizes. “In many cases you can cut costs by 50 percent or more,” says Rupp.

Less finishing work required

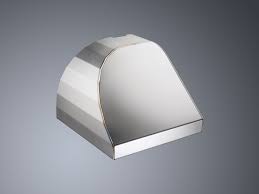
Deciding which laser welding method is the most economical choice depends on the type of part you are processing. Heat conduction welding joins together thin-walled parts and produces seams of very high surface quality. In many cases, this eliminates the need for any subsequent grinding and polishing of the joint, which is why this method is particularly suitable for parts that need an aesthetically superior finish. Another advantage of heat conduction welding is its low heat input, which means that less heat enters the part during machining. This reduces deformation and cuts the cost of subsequent straightening. Overall, this method requires considerably less post-processing, which significantly reduces the cost per part. In the case of a hood made from mild steel 1.5 millimeters thick, for example, the use of a laser has been shown to reduce machining time by 90 percent for a weld seam 122 centimeters long.

Fast welding, new opportunities

Deep penetration welding produces deep, narrow, high-strength weld seams. It can be used with both thin and thick-walled metal sheets, and it gets the job done fast. For example, the 600 centimeters of seams  required to weld together a water tank made from stainless steel three millimeters thick can be handled by a laser at welding speeds of up to 5.4 meters a minute. At that rate, it takes less than 2.5 minutes to weld together the entire tank. Processing times as short as these drive down part costs. What’s more, lasers enable users to open up new avenues of business. This flexible tool can handle a multitude of new joint types and geometries, even if the area to be welded is only accessible from one side. Examples of the challenges lasers can tackle include lap seams, concealed T-joints and even materials of different thicknesses.

Welding together a hood made from mild steel 1.5 millimeters thick using a laser has been shown to reduce machining time by 90 percent for a weld seam that is 122 centimeters long.

Heat conduction and deep penetration methods offer the best quality when it comes to laser welding, though to achieve this the part should normally be subject to the tightest possible tolerance levels. The new FusionLine joining technique can be used to join parts, even when this involves the bridging of gaps. It smooths out any unevenness during the welding process and closes gaps up to one millimeter wide. That makes it possible to use the laser on many parts that were originally designed for conventional welding methods. As a result, FusionLine provides an easy introduction to the world of laser welding, enabling users to boost the capacity of their machines. The system can easily switch between FusionLine and other laser welding methods without retooling, even when it is halfway through processing a part.

Thanks to deep penetration welding, the 600 centimeters of weld seams required to produce a water tank can be processed in less than 2.5 minutes.

The plug-and-play integration of the TruLaser Weld 5000

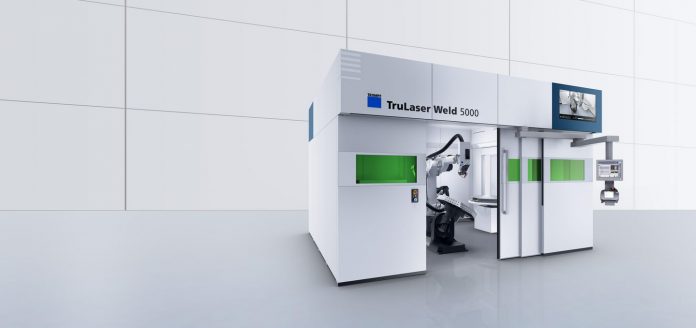
The TruLaser Weld 5000 machine is designed for sheet metal manufacturers who are keen to enter the realm of laser welding. This automated laser welding system can handle heat conduction welding, deep penetration welding and the FusionLine process. The system offers a range of loading and unloading solutions, including the possibility to load the next parts while welding is still taking place. The TRUMPF LaserNetwork system gives sheet metal manufacturers an economical way to gain a foothold in this new technology. It allows the welding machine to use a beam source from an existing machine, eliminating the price of the laser from the investment in the new system.

For more information, contact Retecon – Tel: 011 976 8600
Autonomous 3D Scanner Supports Individual Manufacturing Processes

Let’s say the armrest is broken in your vintage car. As things stand, you would need a lot of luck and persistence to find the right spare part.

But in the world of Industrie 4.0 and production with batch sizes of one, you can simply scan the armrest and print it out. This is made possible by the first ever 3D scanner capable of working autonomously and in real time.

Part of the charm of vintage cars is that they stopped making them long ago, so it is special when you do see one out on the roads. If something breaks or stops working in the vehicle, however, this special status quickly becomes a problem, as spare parts are no longer manufactured either. With the advent of Industrie 4.0, this is set to change: manufacturing is turning toward batch sizes of one and individualized production. This is sometimes also referred to as highly customized mass production.

New scanner works autonomously and in real time

Although this kind of individual manufacturing is still some way off, researchers at the Fraunhofer Institute for Computer Graphics Research IGD are taking the vision of batch sizes of one a big step closer to reality, with a new type of 3D scanning system. “The special thing about our system is that it scans components autonomously and in real time,” says Pedro Santos, department head at Fraunhofer IGD. For the owners of vintage cars with a broken part, this means that the defective component is glued together and placed on a turntable, which is situated beneath a robot arm with the scanner. Everything else happens automatically. The robot arm moves the scanner around the component so that it can register the complete geometry with the minimum number of passes. Depending on the size and complexity of the component, this takes anything from a few seconds to a few minutes. Already while the scan is running, intelligent algorithms create a three-dimensional image of the object in the background. Then a material simulation of the 3D image checks whether a 3D print satisfies the relevant stability requirements. In a final step, the component is printed using a 3D printer and is then ready to be fitted in the vintage car.

No need for protracted learning process

Santos emphasizes that the real achievement here is not so much the scanner itself, but the combination of the scanner with view planning to form an autonomous system. This view planning technology was also created by Fraunhofer IGD. During an initial scan, algorithms calculate what further scans are necessary so that the object can be recorded with as few scans as possible. Thanks to this method, the system is able to quickly and independently measure objects that are entirely unknown to it. This is a unique selling point, because previous scanners either had to be taught how to do this, or else you had to have the CAD model of the component, making it possible to recognize the position of the object relative to the scanner. If you had taught the scanner to scan a car seat for quality control (TARGETACTUAL comparison), then it would be able to scan the next 200 car seats, because they would be largely identical in mass production conditions. But conventional scanners are not suited to the task of handling batch sizes of one. “By contrast, our scan system is able to measure any component, irrespective of its design – and you don’t have to teach it,” explains Santos. “Also, you don’t need information about CAD models or templates – in other words, the specifications of standard forms that a component usually has.”

Manufacturing assistant for Industrie 4.0

Thanks to this USP, the autonomous scanner enables completely new kinds of applications. For example, it can be used as a manufacturing assistant and improve cooperation between humans and machines. This interaction is the focus of the EU-funded Autoware project, which involves the assembly of cylinders including the various pistons, casings and seals. Before now, the cylinders were assembled manually and the subsequent quality control was carried out using a printed checklist and manual measurements. “Our 3D scanning system now enables robots —via comparisons with the database — to recognize what component it has in front of it and also to determine which component its human colleague needs next for assembly of the cylinder,” explains Santos. In addition, the machine carries out the final quality control, scanning the cylinder to check whether the dimensions are accurate. As part of further projects, the Fraunhofer IGD researchers are also testing the entire chain from recording and visualizing up to 3D reproduction.

The researchers will be presenting their autonomous scanning system at Hannover Messe Preview on February 6 and at Hannover Messe from April 23 to 27. Visitors will get the opportunity to place various objects under the laser scanner and view the results live on a monitor. Upon request, they can also scan their own objects. This will allow them to see for themselves how the system actually captures the precise geometry of three-dimensional objects autonomously and in real time.

Efficient Use Of Resources In Manufacture Of Metal Components

Additive Manufacturing has established itself in many industrial sectors as a method for making plastic parts.

The 3D printing of metals is on the road to becoming a similar success story. In the newly opened 3D-Printing Lab for Metals and Structural Materials at the Fraunhofer Institute for High- Speed Dynamics, Ernst-Mach-Institut, EMI, researchers have investigated how resource-efficient the manufacturing process is when lightweight aluminium components are manufactured using additive methods. They discovered that even marginal reductions in the material and resources used per component yield high cost savings in series manufacturing.

The 3D-Printing Lab for Metals and Structural Materials at Fraunhofer EMI in Freiburg houses one of the largest commercially available 3D printers for metal currently in existence. In the research sector, an apparatus of this size is unique. Using the selective laser melting technique metal structures with dimensions of up to 40 centimeters can be made by additive manufacturing. 3D printing offers completely new ways of designing components with highly complex shapes and optimizing their weight. But it is only by combining Additive Manufacturing and intelligent lightweight design that you can maximize resource efficiency in manufacturing. Fraunhofer researchers in the 3D-Printing Lab have investigated just how economical the manufacturing process is in terms of resources and whether material and operating costs can be minimized compared to conventional industrial methods. To do this, they took a practical, widespread component for their tests: a wheel carrier such as might be used in a lightweight vehicle. “We were able to quantify the effect lightweight construction – and specifically the use of structural optimization methods – has on the resources used in the SLM manufacturing process,” says Klaus Hoschke, scientist and group leader at Fraunhofer EMI. The focus was on energy and material consumption, the manufacturing time and the CO2 emissions that arise during the small-scale production of twelve wheel bearings.

Resource efficiency of a small manufacturing run

After the researchers had used the numerical finite element method (FEM) to simulate and analyze a draft design and determine the right geometric shape with structural optimization methods, they constructed the wheel bearing in an optimized lightweight design.

Several structural components arranged on a base plate after a selective laser melting process. © Fraunhofer EMI

The result was a wheel bearing designed for the defined load scenarios and offering maximum performance. Because of their geometric complexity, structures produced in this way cannot be manufactured by conventional methods such as milling or turning. “With the lighter model, we were able to save hugely on resources during production, as less material has to be produced per component. If you multiply this by the number of units in a small-scale run, then you require less time, material and energy for manufacturing. Reducing volume through the use of higher-strength materials offers the greatest potential for energy savings here,” says the researcher. Using the numerically optimized version of the wheel bearing, 15 percent less energy was required for the additive process than for the conventional method: Twelve kilowatt hours of electricity were needed for the conventional design, whereas only ten kilowatt hours were needed for the numerically optimized design. (In each case, the measured value refers to a series-manufactured component.) Manufacturing time was cut by 14 percent and CO2 emissions by 19 percent. And where material consumption was concerned, it could be significantly reduced by 28 percent.

Finite element analysis of the start design of a wheel bearing technology demonstrator (left); numerical design optimization of the technology demonstrator to reduce the component’s mass without impairing functionality (center); and CAD template for manufacturing the 3D metal component (right). © Fraunhofer EMI

Additive Manufacturing – the method of choice

Although structure-optimizing algorithms and numerical optimization simulations are already being employed in the 3D printing of components today, they are only used when the component must be extremely lightweight, such as aircraft parts designed to reduce fuel consumption during operation. Components that lack these implications as regards structural optimization are still generally manufactured using conventional industrial methods. The results of the smallscale series production of the wheel bearing suggest that additive manufacturing can also be useful when a component does not have to be structurally optimized as such. “A heat exchanger or a tool mold, for example, do not have to be lightweight to improve their functionality. Nevertheless, it makes sense to design them with reduced weight and volume when manufacturing them additively, because this way you can bring down manufacturing costs,” explains Hoschke.

Lattice cube with edge length of 40 centimeters, one of the largest metal structures manufactured using selective laser melting (SLM). © Fraunhofer EMI

Forecasts on what effect the Additive Manufacturing of metals will have on global production vary widely. But everyone agrees on one thing: for many industries – such as aerospace, automotive engineering, medical engineering and toolmaking – it is a game changer. “Our positive results for resource efficiency in the manufacturing process should reinforce this,” says the scientist. In the future, Hoschke and his team want to research the extent to which other design heights, series sizes and materials such as titanium affect the resource efficiency of the manufacturing process.

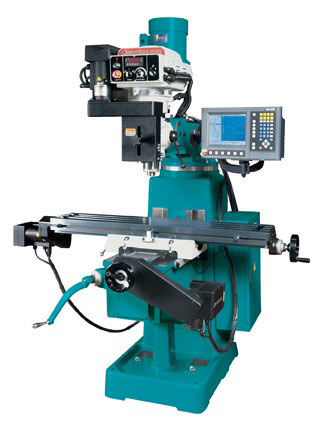
The New Clausing MillPWR CNC Milling Machine

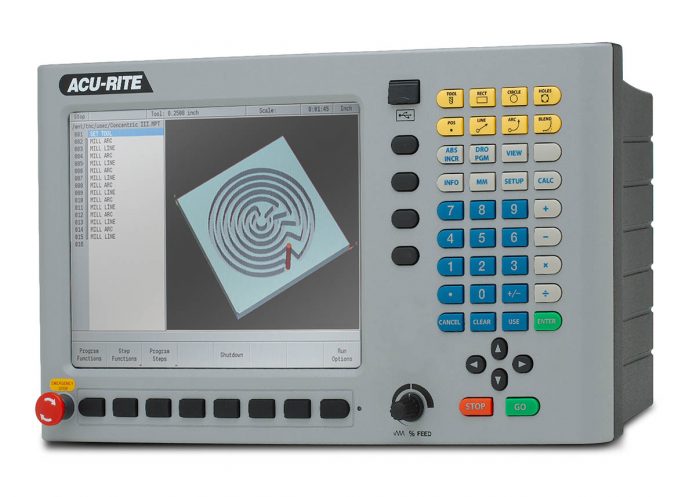
The New MillPWRG2 CNC milling machine is fitted with the powerful, flexible and user-friendly Acu-Rite control system from Heidenhain, which is also available in 4 optional languages such as English, French, German and Spanish.

The MillPWR mill allows you to create and program complex parts in minutes, manufacture one-offs and small batch components, routinely mill prototype and test components, uItilise the easy-to-use, full conversational programming system for quick, no fuss cutting and produce highly accurate parts first-time with ultra-high precision 1μm resolution scales.
The MillPWR Acu-Rite control uses a 12.1″ high-resolution screen, displaying graphics in either 2 & 3D line or 3D solid formats and although user-friendly conversational programming is used throughout with the addition of an on-board calculator, the MillPWR system allows uploading, editing and running G Code and DXF files, enabling users to transfer and use programs directly to and from the machine.

Data storage is also industry-leading, with a huge 2.5 GB of internal memory and the ability to store and modify up to 99 part programs, all as standard features. For external storage, USB and Ethernet capability are also available as standard.

The MillPWR CNC mill is supplied in three models with table sizes from 230 x 1245mm and 254 x 1370mm. Powerful 2.2 or 3.7kW motors are used, giving spindle speeds of up to 4350 rpm, combining fast, powerful and highly accurate cutting. Spindle tapers of either R8, ISO 30 or 40 can also be supplied.

For more information contact F&H Machine Tools – Tel: 011 397 4050

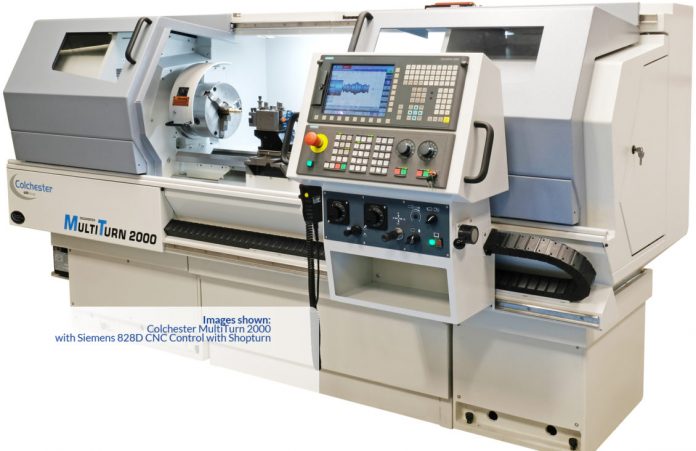
Colchester Multiturn CNC Lathe Launched

The MultiTurn takes a highly established, robustly engineered lathe concept from Colchester that makes it the perfect machine for many of today’s CNC turning applications.

The MultiTurn is robust, stable and highly precise, irrespective of the component size handled.

The Siemens 828D control with Shopturn has a well-earned reputation for being highly user-friendly and intuitive, ensuring that operators can cut quickly and easily with very little training. However, the Shopturn system is also powerful enough for more advanced CNC users to output maximum productivity quickly.

The Colchester MultiTurn lathe has been designed specifically for CNC users looking for increased versatility on one-off and small batch production, first time CNC buyers and jobbing shops looking for real programming simplicity and education and training establishments needing a real lathe with step-by-step simplicity.

Available are six Colchester MultiTurn models, starting with the compact MultiTurn 1000, which has a 330mm swing over bed, a 7.5kW motor, outputting spindle speeds of 3500 rpm, right through to the heavyweight MultiTurn 6000, which has a massive 760mm swing over bed and an 18.5kW motor giving spindle speeds of up to 1400 rpm.

The MultiTurn 6000 also has bed length options ranging from 1.5 to 6 metres, ensuring that the MultiTurn is capable of turning any component, regardless of size, right through to long shafts, billets, bar stock and castings.

Isuzu Motors South Africa Is Officially Launched

Isuzu Motors announced the official launch of its business operations in South Africa recently.

This follows the announcement of last year where Isuzu had said that it would purchase the light commercial vehicle operations in Port Elizabeth and also the balance of shareholding in its Isuzu Trucks South Africa operations.

Speaking at the event which was held at manufacturing plant in Struandale Port Elizabeth, the President and Representative Director of Isuzu Motors of Japan Masanori Katayama said that Isuzu was committed to growing its business in South Africa. “This is the first commercial and light commercial vehicle manufacturing operation outside of Japan in which we have acquired a 100% ownership. We are represented in 30 countries outside of Japan and successfully operate 47 manufacturing plants in these countries with joint venture partners.”

“Our decision with regards to South Africa demonstrates the confidence we have in this market and also is indicative of our longerterm view that South Africa will serve as an important base for our future growth on the African continent.”

COEGA EIA Landmark Approval For ADZ

The Coega Development Corporation (CDC) recently received news on a landmark approval of an Environmental Impact Assessment (EIA) for a 440 ha Land-based Aquaculture Development Zone (ADZ) and Desalination plant in Zone 10 of the Coega Special Economic Zone (SEZ).

“The approval of the EIA is a major leap towards fulfilling the Coega SEZ’s vision to locate one of the largest ADZ’s in South Africa on one geographical footprint, in the Coega SEZ and respond to the severe water shortages experienced by the Nelson Mandela Bay (NMB),” says Dr Keith Du Plessis CDC Manager: Project Development.

It has been found that failure by especially smaller companies to obtain EIA approval often result in projects never seeing the light of day. Because of this, the aquaculture sector in SA is largely untapped and underperforming.

“The approved EIA relieves the financial burden from the investor as it would ordinarily take up to two years for companies seeking to establish an aquaculture facility and or a desalination plant at the Coega SEZ. This is evident of the CDC’s value proposition as a plug and play environment, where investors have shortened timeframes from when they enquire about investing to when they have access to market,” adds Du Plessis.

The NMB Municipality, in this month announced that the water levels of the Metro supply dams have reached an all-time low of just above 24 percent. The CDC now has authorization to develop facilities for the desalination of water with a maximum capacity of 60 million litres (Ml) per day.

“This capacity, if tapped into, could provide for almost quarter of Nelson Mandela Metro’s current water consumption needs (currently at approximately 260 Ml/day). The CDC is a capable and potential solution to the water problems experienced in the Metro,” outlines Du Plessis.

Metals And Engineering Sector To Grow More In 2018

Speaking at the launch of its authoritative State of the Metals and Engineering Sector Report 2018 to 2019 in Johannesburg, SEIFSA Chief Economist Michael Ade said the metals and engineering sector is poised for 1,1% growth this year, following an impressive 2,7% growth in 2017.

Dr Michael Ade, Chief Economist of the Steel and Engineering Industries Federation of Southern Africa (SEIFSA).

Ade said this prognosis is supported by global economic growth, which remained fairly robust in 2017, aided by a rebound in investment and trade, against the backdrop of benign financing conditions, generally accommodative policies, improved confidence and the dissipating impact of the earlier commodity price collapse.

He said 2017 was a much better year for the metals and engineering sector, which rebounded from the recession in preceding years, registering a 2.7 percent growth “despite facing serious structural challenges”. He said the momentum was expected to continue in 2018.

“Despite the current potential to improve on margins in the M&E sector being fragile due to domestic headwinds, all indications are that the sector will record another increase in growth during 2018, barring any major disruptions to production,” Ade said.

Commodity prices recovered last year and are expected to gain momentum in 2018, thereby strengthening exports and improving growth prospects for commodity exporters in emerging markets commented Ade. “However, it is unclear how long the positive outlook will continue, given the volatility in commodity prices,” he said.

Ade said downside risks include disorderly financial market movements, negative effects of borrowing costs, as well as rising trade protectionism or geo-political risk which could also negatively affect confidence, trade and overall economic activity.

He said the prognosis also aligned with the outlook for an improving – but subdued – domestic growth underpinned by positive projections for fixed capital formation, better domestic trade conditions and reduced exchange rate volatility.

“Our position is also influenced by positive growth prospects for key industries which are important markets for the M&E sector’s intermediary products and are crucial in the sector’s value chain,” Ade said.

However, he cautioned that the recent downgrade of South Africa’s sovereign credit ratings to junk status by Fitch and Standard and Poor’s would have the propensity of increasing borrowing costs and the general cost of doing business, thus negatively affecting production and fixed investment into the sector and adding to its structural challenges.

Automation Industry To Help Fast Track Economic Growth

Speaking at the official launch of the Africa Automation Fair 2019 in Johannesburg recently, stakeholders noted that South Africa was emerging from turbulent times, but said that through collaboration to drive progress, the automation sector could help fast-track economic growth and development.

The automation sector, now moving toward a digital Industrie 4.0/IIoT era, is poised to drive greater efficiencies and make South African enterprises internationally competitive, which will ultimately benefit all South Africans, they said.

Oratile Sematle, President of the Society for Automation Instrumentation Measurement and Control (SAIMC), noted that the industry had already progressed to a point where its voice as a collective is now heard in government, institutions and various sectors. “But knowing that if we use automation in the right ways, we can ultimately change the landscape of the South African economy and improve the lives of all people, we need to continue to collaborate to drive further progress and make South Africa great again,” he said.

Marc Van Pelt, Chairman of the Industrial Instrumentation Group (IIG) and MD of Pepperl+Fuchs, noted: “as we seek to bring the country to new levels economically, we need to look to automation and smart manufacturing to make our industries competitive on a global basis. At the Connected Industries conference earlier this year, the sector started the Industrie 4.0/IIoT discussion, and the next question is: who is using it? Is the sector ready? As a country, we still have a long way to go.”

Sematle and Van Pelt encouraged industry stakeholders to step up collaborative efforts through forums such as the Africa Automation Fair and Connected Industries conference, where the sector is able to assess the automation industry’s challenges and seek solutions to support progress.

The Africa Automation Fair, which marks its 21st anniversary in 2019, and the Connected Industries conference, will expand its scope and reach in 2019, delivering Africa’s largest showcase of industrial automation and control technologies. The event, incorporating the Connected Industries conference (Industrie 4.0/IIoT), is a focused networking platform for the Automation and Control Industry and works closely with industry associations including the IIG and SAIMC.

Africa Automation Fair 2019 is organized by Reed Exhibitions.