Home Blog Page 75

Economic Confidence Continues To Build Ahead Of IMTS 2018

Numerous major economic indicators signal that the U.S. manufacturing industry, the second largest market in the world with a value of nearly $9 trillion, will enjoy its strongest growth in more than a decade leading up to IMTS 2018, held Sept. 10-15, 2018 at McCormick Place in Chicago.

Overall manufacturing growth for 2018 is expected to increase by 8 to 9 percent compared to 2017, according to Patrick McGibbon, Vice President of Strategic Analytics, AMT – The Association For Manufacturing Technology, which produces IMTS.

“Economic indicators suggest a longer term, continued expansion. In the short term, we anticipate immediate acceleration in capital investment among IMTS 2018 visitor and exhibitor companies,” says McGibbon. “Changes to the U.S. tax law should further encourage purchasing during and after the show. Reduced tax rates will increase available capital. R&D tax credits expand innovation and fully expense capital expenditures which encourages purchasing.”

“The U.S. manufacturing sector is expressing economic confidence at levels not seen since the dot com boom. If there was ever a year to experience the energy, optimism and innovations offered at IMTS, this is it,” says Peter R. Eelman, Vice President – Exhibitions & Business Development at AMT, who has participated in every IMTS since 1980.

Orders for manufacturing technology in January 2018 were up 44 percent compared to January 2017, according to the latest U.S. Manufacturing Technology Orders (USMTO) report from AMT. It was the second-largest January in the 22 years recorded by AMT’s USMTO program.

The February 2018 Manufacturing ISM® ReportOnBusiness® notesthatthePMI® (Purchasing Managers Index) registered 60.8 percent, an increase of 1.7 percentage points from the January reading of 59.1 percent and the 18th consecutive month of expansion. A reading above 50 percent indicates the manufacturing economy is generally expanding.

Other positive indicators include U.S. cutting tool shipments, a metric produced by the U.S. Cutting Tool Institute (USCTI) and AMT. With a year-to-date total of $2.195 billion, cutting tool shipments for 2017 was up 8.3 percent over 2016. The Michigan Consumer Confidence Index rose to 120 in March, the highest level in over 14 years.

Industry capacity utilization stands at 78 percent and is headed toward 80 percent, which economists consider a key metric that signals full utilization. At this point, supply chain and labor constraints can hinder further expansion. Some of the strongest U.S. segments include automotive (82.9 percent capacity utilization), aerospace (77.6 percent) and energy and power generation (79.8 percent) segments.

Smart Technologies Are Driving Tomorrow’s Production

EMO Hannover (18. bis 23. September 2017) - Weltleitmesse der Metallbearbeitung. mav industrie 4.0 area: Experten präsentieren Praxislösungen zur Digitalisierung Ihrer Fertigung (FRAUNHOFER IPA, Halle 25, Stand B60 WGP

EMO Hannover 2019, the world’s premier trade fair for the metalworking industry, will be held from 16 to 21 September 2019 under the motto of Smart technologies driving tomorrow’s production.

It will thus be concentrating on the current paradigm shift in industrial production operations, which are no longer focusing (only) on better, faster, more accurate, but on the development and implementation of new functions within the framework of Industry 4.0. Digitalization and intelligent networking in conjunction with numerous new developments, from Big Data, data analytics and artificial intelligence, all the way through to the platform economy, create the foundations for new business models, so that customers and vendors can reach a new level of productivity.

“The last EMO Hannover had already shown that Industry 4.0 has arrived in the machine tool industry,” says Carl Martin Welcker, General Commissioner of EMO Hannover 2019. “As the world’s leading innovation platform, we are progressing this trend by focusing on the next development step in production operations: the technical options opened up by digitalization and networking, which are being increasingly reflected in new business models,” he adds. “This doesn’t mean that in future we shall no longer be working on optimizing machines and processes in the traditional way. I am, however, confident that quantum leaps forward in terms of productivity, quality and reliability will be triggered primarily by the new technologies. So in 2019 we will  be seeing an abundance of solutions that implement new services for the machine tool industry’s customers.”

Rendering data intelligently usable

For new business models on a broad front, first of all the immense quantities of data generated by digitalization and networking of machines and processes have to be reduced to a usable level. Because only if you can extract the relevant data (Smart Data) from the superabundance of Big Data can you derive an entrepreneurial benefit from Industry 4.0. Last year, scientists at the German Academic Society for Production Engineering (WGP) in their position paper on Industry 4.0 had already published an action guide and shown how Big Data can be rendered manageable using the data mining method, for example. Besides this guide, the professors at the WGP contribute their state-of-the-art expertise to other bilateral arrangements between the industrial sector and the academic community. Not least, they utilise the EMO Hannover in order to showcase for a global public the projects they are conducting together with industrial partners.

Utilizing artificial intelligence

In recent years, artificial intelligence (AI) has achieved some amazing breakthroughs. One of its capabilities, machine learning, enables machines and processes to optimise themselves with the aid of Smart Data. They detect patterns in data flows and derive the appropriately responsive actions. The system learns from every situation.

Artificial intelligence has already arrived in our everyday reality. To ensure that the mechanical engineering sector also benefits from this, the VDMA has published a study entitled Machine Learning 2030, which is intended as a kind of roadmap. The recommendations for companies, politicians and researchers are currently being firmed up and implemented in a VDMA working group. It’s now only a question of time before this futuristic scenario, too, arrives in the factories. The automotive industry, for example, is already making massive use of artificial intelligence and entering into appropriate alliances. This is adequately exemplified by the cooperative arrangement between Mercedes- Benz and the graphics-chip manufacturer Nvidia. Together, they are aiming to put an AI-based vehicle on the road in the next few years. For machine tool manufacturers, too, artificial intelligence offers an abundance of potential.

Utilizing new economic structures

There is fresh evidence almost daily that the use of Industry 4.0 is helping to develop new economic structures. More and more platforms are being created, on which manufacturers and service providers can support their customers from a single source using a product-themed approach. So machine tool manufacturers, too, will be well advised to seize the opportunity and take this trend on board. Because the trend towards a platform economy is unmistakeable, as current studies show.

There are already some examples here, like Virtual Fort Knox, a Cloud-IT platform for production companies created by the Fraunhofer Institute for Manufacturing Engineering and Automation (IPA) in Stuttgart. “It functions as an IT backbone for Industry 4.0 solutions and networks production companies with software vendors and machinery manufacturers. But IT companies, control system and machinery manufacturers will also be offering their solutions.

“We are seeing how new technologies are influencing and even driving forward developments in the machine tool industry,” says General Commissioner Welcker. “By September 2019, numerous specific solutions will be available on the market. I can say this with confidence, since many EMO exhibitors will be using this international shop window, in order to showcase their corporate capabilities and enhance their profiles.” Industry 4.0, he adds, creates new customer needs, to which machinery manufacturers must respond in order to remain competitive.

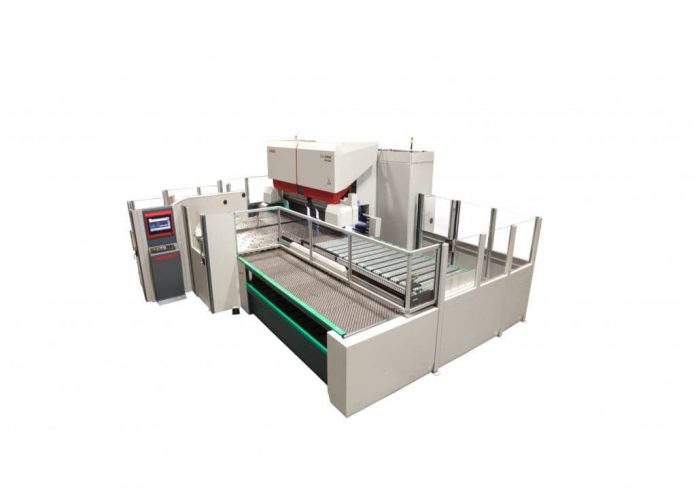
Durma Panel Bender Bending Centre

Fast manufacturing and high precision repeatability are amongst the most important criteria in today’s sheet metal processing industry.

For this reason, automation and robotic systems are increasingly in demand. Similarly, bending machines also require change in application technology. Complex bends that cannot be performed by using automated and robotic sub-systems and conventional bending machines, can be performed with high precision repeatability by using the Durma CNC fully automatic servo Panel Bender machine. The Panel Bender machine should not be confused with conventional bending machines. The Durma Panel Bender is a fully automatic sheet bending machine equipped with different systems in every direction.

While featuring 28 fully automatic operation axes, all axes are servo controlled in addition to 40 pneumatically controlled motion- and positioning axes. Thanks to the smart consumption system, the machine calculates the optimum amount of energy required, thus providing energy saving.

The Panel Bender machine is built on a stress relieved carrier body, which features a bending device, holding devices and movement – plus positioning equipment. In front of the machine, there are a referencingand manipulator device which manage positioning of the part to be bent.

As a working principle, the blanking sheet material manipulator is clamped between the upper and lower clamps. The manipulator device, has the ability to rotate and move toward, lean the sheet against the referencing pins in the reference device and the appropriate position. After this point the panel bender machine, having reference information, is fixed on the sheet bending area by means of the holding device and the appropriate bending is performed by movement of the bending device.

While the machine is able to handle sheet materials in thicknesses between 0,5mm – 3,2mm, it can also bend aluminium material up to 4mm thickness and stainless steel material up to 2,2mm.

The Panel Bender machine meets the requirements of manufacturing sectors such as elevator, steel door, panel, kiosk and control panel, cabin and case, industrial cooling systems, industrial ventilation systems, industrial kitchen, domestic appliance and lighting systems manufacturing.

For more information contact Durmazlar – Tel: 011 865 4090

Xact Smart Range Of Press Brakes

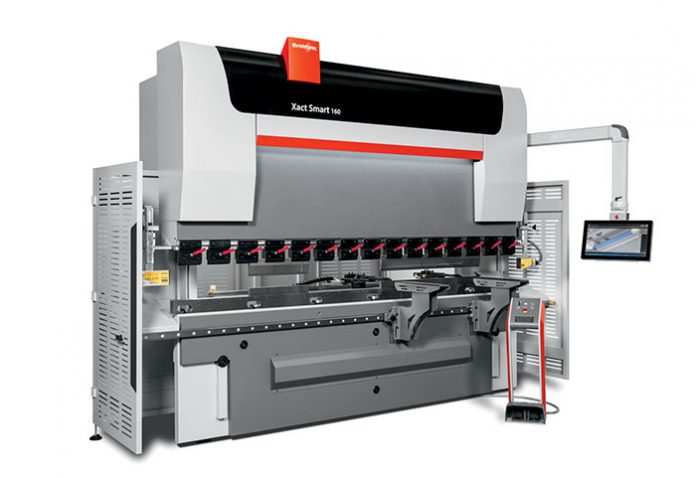
While many fabricators in business today require an easy-to-use bending solution that is affordable and which will complement their existing cutting and welding facilities, Bystronic has released the 100/3100, 160/3100 and 225/4100 models of their Xact Smart press brake range in South Africa.

In terms of bending force, the 100/3100 model will exert 100 tons/1600 kN, the 160/3100 160 tons/1600 kN, and the 225/4100 model 225 tons/2250 kN. The 100/3100 and the 160/3100 offer bending lengths of 3100mm while the 225/4100 model has a 4100mm bending length. The standard stroke for all three machines is 200mm and each has an open height of 480mm.

Options of extending the daylight and stroke by 100mm to an open height of 580mm are also available on all three models.

Other features of these press brakes are an intuitive user interface, LED work-space lighting, Energy Saver, Fast Bend increased speed as well as options of two, four or fiveaxis back gauge, hydraulic tool clamping and most importantly a laser safety system.

In terms of the user interface, with the use of Bystronic’s BySoft 7 CAD/CAM software, it is possible to design parts, create cutting plans and bending programmes. When manufacturing, it is possible to monitor the production process. In spite of the power of Bystronic’s BySoft software, it is userfriendly and easy to operate. Moreover, this software package will integrate Xact Smart press brakes with other smart machines in a factory operating environment.

Bystronic press brake operators are invited to use the Bystronic Bend Solver application for the calculation of all bending parameters. The Bend Solver illustrates the complex calculations using easily understandable visualizations. Depending on the material and its thickness, it provides the information about the required bending force, box height, upper tool height, the lower tool opening, the radius and the minimum flange length. In addition, should a manufacturing facility have a number of Bystronic press brakes of varying capacities, it is possible to establish which bending machine will be most suitable for the job in hand.

For operators, interface with an Xact Smart press brake is through an intuitive touchscreen. When bending steel parts, consistent accuracy is absolutely vital. Bystronic’s Xact Smart press brakes offer the highest levels of repetitive accuracy of any press brake on the market.

Bystronic also offers a comprehensive range of tools that will cover nearly every conceivable bending application. These tools will fit a range of clamping systems, while the hydraulic clamping of tools allows for rapid changes leading to greater productivity. Bystronic tools offer outstanding quality and a long service life thanks to manufacture using high-strength tempered 42CrMo4 steel, with deep inductive hardening to between 58 and 62 HRC.

In a busy production environment, it is still possible to keep track of tools as the most important information is engraved on the surface of the tool. However, should a custom tool be needed for a special application, Bystronic will be happy to have such a tool designed and manufactured and delivered quickly and reliably.

Users of Xact Smart press brakes will benefit from decades of expert product design and knowledge in the processing of sheet steel. With advanced fiber lasers for ever-faster fabrication, complementary Xact Smart press brakes provide all the speed and versatility required for bending solutions within the highspeed automated Industry 4.0 environment which characterises manufacturing today.

For more information, please contact Bystronic – Tel: 083 288 1111

Panel Bending – Fully Automatic Processing With Top Part Flexibility

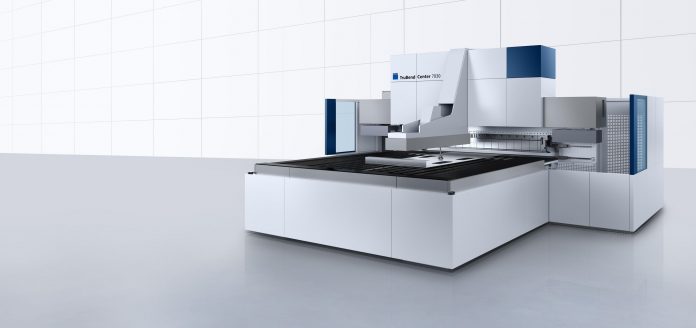
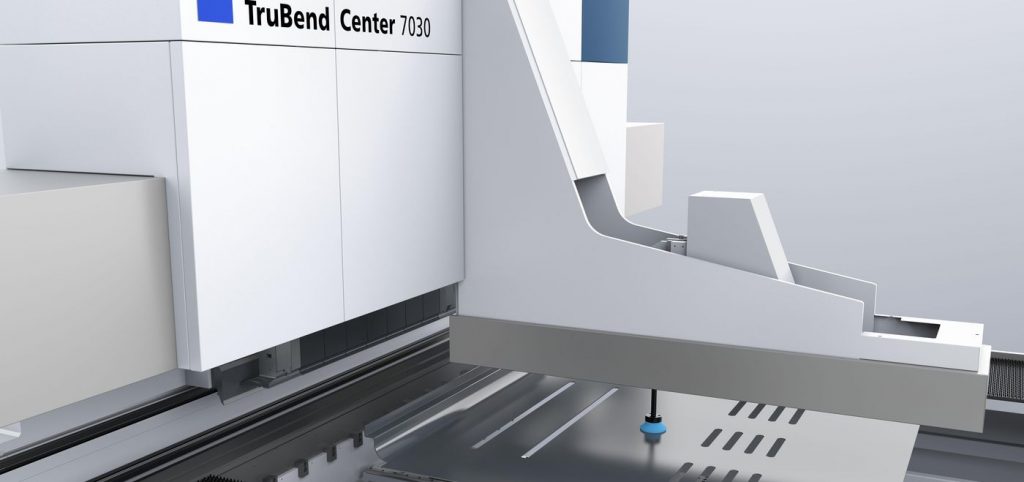
Panel bending with maximum part flexibility has now got even faster with the TruBend Center 7030, the fully automatic panel bending cell.

Panel bending with maximum part flexibility is faster with the TruBend Center 7030, TRUMPF’s fully automatic bending cell.

The machine turns the parts automatically, freeing up the operator and increasing the productivity of the bending process. The usual benefits of TRUMPF panel bending are retained – short side lengths, small profiles and parts with formed sections, recesses, diverse radii or multiple negative bends – the machine reliably bends them all with precision. The laser-based ACB angle measurement system enables operators to work with greater precision and in conjunction with TRUMPF TecZone Fold (the fastest offline programming tool on the market), more efficiently than ever.

Fully automatic machine with top part flexibility

Using the new rotary part manipulator, the TruBend Center 7030 can bend parts fully automatically. The manipulator secures the sheet and rotates it as needed into the required position. Here, axis speeds of 3,000 millimeters per second make it possible to achieve significantly increased productivity compared to the semi-automatic TruBend Center 5030 panel bender.

Using the new rotary part manipulator (highlighted in blue), the TruBend Center 7030 can bend parts fully automatically – the manipulator secures the sheet and rotates it as needed into the required position.

When it comes to positioning smaller parts, the patented 2-axis part manipulator also comes into play. The synchronized interaction of rotary and 2-axis part manipulator allows what is for fully automatic panel bending an unusually large degree of freedom to shape components. With its TruBend Center 7030, TRUMPF is offering a fully automatic panel bending machine with an additional vertical axis for the 2-axis part manipulator. This makes for unprecedented flexibility, since the gripper modules can fasten onto parts in a variety of positions, making it possible, for example, to secure narrow profiles on their edge or grip them with clamps and bend them. Without this additional feature, many parts would be impossible to manufacture. The vertical axis also ensures that the operator can easily remove parts with downward edges.

The TruBend Center 7030 is designed to allow for a wide range of shapes and formats, including sheets of aluminium up to 4 millimeters thick, mild steel up to 3 millimeters thick, or stainless steel up to 2.2 millimeters thick. The machine handles extremely short side lengths, boxes up to 220 millimeters deep, small profiles, narrow or negative bends and diverse radii. A single tool can be used to achieve these different bending radii very quickly and that increases both creativity and productivity by allowing product designers to incorporate more curves in trim panels or create exceptional geometries. Because the machine operates with extremely high precision (the accuracy of repetition is precise to within hundredths of a millimeter) and uses bending tools that are mechanically stable, it can process with a minimum of tool marks which is a great advantage in the case of stainless steel and painted sheet metal.

First angle measurement system for automatic panel bending

Precise angles are essential for bending. The main threats to achieving this precision come from variations in material characteristics such as strength, spring-back and fluctuations in material thickness. To ensure precise angle measurement, the TruBend Center 7030 is fitted with TRUMPF’s tried and tested Automatically Controlled Bending (ACB) solution. This makes it the first fully automatic panel bending machine to have an angle measurement system, which means quality parts from the outset. The two ACB laser modules for negative and positive bends are placed with the additional bending tools, and they automatically move into position for the measurement process. The laser then projects a line onto the sheet and a camera detects the position of the line and calculates the part angle in real time.

Another special feature of the TruBend Center 7030 is the extremely powerful TRUMPF programming software TecZone Fold. This is the fastest programming tool on the market, and it has won over users of the TruBend Center 5030. TecZone Fold automatically creates bending programs in a few seconds – as well as 3D-simulations complete with collision monitoring, which makes efficient workshop programming possible for the first time for panel bending. This operator-friendly software is included in the base model, and it runs on the control unit as well as on the office PC (as an offline version). That makes the TruBend Center 7030 extremely economical even for manufacturing small batches or single parts.

For more information contact Retecon – Tel: 011 976 8600

All-Purpose Talent In Aircraft Manufacturing

In aircraft manufacturing, much of the milling, drilling and assembly is still done by hand.

This is because the raw components vary not only in size and design, but also in shape accuracy. Small differences are unavoidable in extremely lightweight and elastic materials, which poses a challenge for automated processing. Working with an industrial consortium, Fraunhofer researchers have now developed a mobile robot that is able to handle these high requirements – the only robot in the world with this capability.

When automated machines are used in aircraft manufacturing today, they tend to be heavy, customized portal systems that slide slowly over the components on rails.

However, as well as being expensive and inflexible, these systems stand idle for long periods, meaning their productivity levels are low.

“Our new robot is able to travel to the components autonomously and carry out all the requisite tasks there. Measuring, bonding, drilling, milling – it can do it all. The robot is an all-purpose machine and can be adapted quickly and flexibly to shape inaccuracies of large components as well as product and model modifications,“ says Dr. Dirk Niermann, Head of the Automation and Production Technology department at the Fraunhofer Institute for Manufacturing Technology and Advanced Materials IFAM in Stade. Whereas earlier robots have failed when it came to the high precision requirements in the aviation sector, the new robot has no such difficulties: the deviations in its machining results are less than half a millimeter.

Accuracy gains thanks to output-side measurement systems

“Above all, by integrating specially developed output-side measurement systems (so-called secondary encoders), we managed to substantially minimize error,” explains Christian Böhlmann, Group Manager for Integrated Production Systems. While the measurement technology is attached to the engine in conventional industrial robots, it is fitted directly to the axles of the new robot. “This way, we always know the exact position of the axles.” Other technologies also helped increase processing accuracy, including the control-side compensation of frictional adherence effects from the gears and a refined calibration of the robot, by means of which one-off measurements are carried out to determine the true robot geometry, which is then factored into calculations of motion.

Because aviation components are often up to 20 meters in length, mobility was important when designing the new robot. “We developed a rigid platform with three drive wheels for the robot,” says Böhlmann. “This means it can move freely around the factory floor and go wherever it is needed at a given time. As soon as it reaches its destination, it draws in its wheels and stands in a stable position.”

In this way, the robot and other modular robotic production systems from Fraunhofer IFAM facilitate fluid, versatile manufacturing; they no longer pass through rigidly determined stations, but adapt quickly, flexibly and cost effectively to different requirements.

U.S. Investigation On Steel And Aluminium Products

The South African Government has noted the announcement of the President of the United States of America, Donald Trump on 8 March 2018 that he has signed proclamations to impose a 10 percent ad valorem tariff on aluminium articles and a 25 percent ad valorem tariff on steel articles.

It was further announced that the UnitedStates (US) will consider specific requests from affected domestic parties, to exclude from any adopted import restrictions those steel articles for which the Secretary of Commerce determines there is a lack of sufficient US production capacity of comparable products, or to exclude steel articles from such restrictions for specific national security-based considerations.

The proclamations make a provision for any country with which the US has a security relationship to discuss with the US alternative ways to address the threatened impairment of the national security caused by imports from that country. Should the US and that country arrive at a satisfactory alternative means to address the threat to the national security, the US President may remove or modify the restriction on steel articles imports from that country and if necessary, make any corresponding adjustments to the tariff as it applies to other countries as the national security interests require.

In relation to aluminium, the products to be affected are defined in the Harmonized Tariff Schedule (HTS) as: (a) unwrought aluminium (HTS 7601); (b) aluminium bars, rods, and profiles (HTS 7604); (c) aluminium wire (HTS 7605); (d) aluminium plate, sheet, strip, and foil (flat rolled products) (HTS 7606 and 7607); (e) aluminium tubes and pipes and tube and pipe fitting (HTS 7608 and 7609); and (f) aluminium castings and forgings (HTS 7616.99.51.60 and 7616.99.51.70), including any subsequent revisions to these HTS classifications.

The products affected in relation to steel are defined at the Harmonized Tariff Schedule (HTS) 6-digit level as: 7206.10 through 7216.50, 7216.99 through 7301.10, 7302.10, 7302.40 through 7302.90, and 7304.10 through 7306.90, including any subsequent revisions to these HTS classifications.

In addition, the Secretary of Commerce is expected to publish the Federal Register on the appeal process for US buyers to apply for exclusion within 10 days. The tariffs will be implemented on 23 March 2018, if no alternative arrangement is agreed to with individual countries.

South Africa is studying the proclamations and its implications for the domestic industry in South Africa. South Africa’s exports to the US on steel amounted to US$950 million in 2017 and accounted for 1.4% of U.S.’s global imports. In the case of aluminium, the SA exports were US$375 million in 2017, accounting for 1.6% of US imports from all global suppliers. It is clear that South Africa’s exports do not impose a threat to US industry and jobs. The SA exports are in some cases used as inputs into further processes in the US manufacturing sector thus in fact contributing to US jobs and production.

The Department of Trade and Industry (the dti) is fully engaged with the matter and continues to have discussions with the US on this issue. A formal submission will also be made to the US as is provided for in the proclamations.

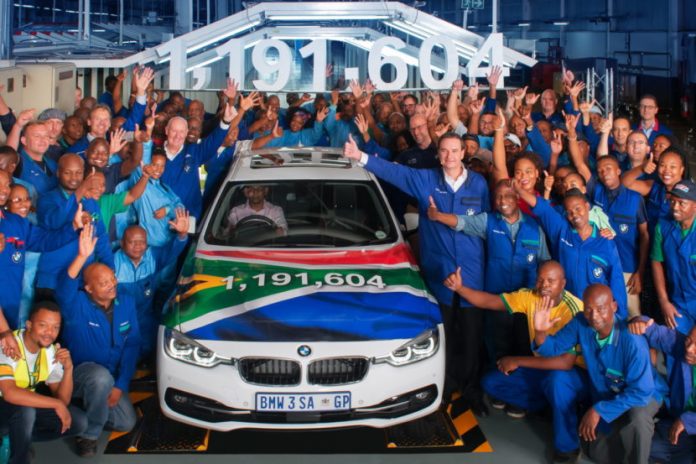
The Last BMW 3 Series Sedan Rolls Off The Production Line At BMW Group Plant Rosslyn

“We look back with great pride over an extraordinary career path of the production at Plant Rosslyn. Over the years, the development of our production and export programme has been the catalyst for our sustainable growth and contribution to the South African economy,” says Tim Abbott, Chief Executive Officer (CEO) of BMW Group South Africa.

In the next few months, Plant Rosslyn will launch the production of the BMW X3. In the future, the BMW 3 Series Sedan will also be manufactured at the new BMW Group plant in San Luis Potosí, Mexico.

One of the key milestones of the BMW 3 Series has been the success in founding the segment of the modern sports sedan, establishing itself as the embodiment of driving pleasure in its segment and becoming the world’s top-selling premium car. The enthusiasm for this model series was also shared by the production staff who expressed their passion for these cars by giving them legendary nicknames. Each generation of the BMW 3 Series produced at Plant Rosslyn had its own nickname: the third generation, for instance, was called Dolphin for its elegant contours. Limited edition models of the BMW 3 Series, such as the BMW 333i and 325iS, also emerged from the plant.

With the production of the new BMW X3 in the coming months, a new era will begin at Plant Rosslyn. In November 2015, BMW Group South Africa reaffirmed its long term commitment to South Africa by announcing that it will invest a total of R6 billion at Plant Rosslyn. The investment – one of the biggest in the local automotive industry – has enabled Plant Rosslyn to get ready to produce the new BMW X3. In October 2017, an additional R160 million was invested into the Rosslyn manufacturing facility to enhance production line speed.

SEIFSA Welcomes Rebound In Metals And Engineering Sector

Dr Michael Ade, Chief Economist of the Steel and Engineering Industries Federation of Southern Africa (SEIFSA).

The data indicated that production in the M&E sub-components increased by 5.1 percentage points in January 2018 on a year-on-year basis when compared to January 2017, and by 2.1 percentage points in January 2018 on a month-to-month basis when compared to December 2017.

“The output performance of the M&E cluster is welcomed and the expectation is for the positive growth path to continue, as all stakeholders within the cluster and the broader manufacturing sector step up efforts to boost overall production. The performance of the M&E cluster generally augurs well for the broader domestic economy and hopefully will significantly boost the real Gross Domestic Product (GDP) for quarter 1 of 2018,” Steel and Engineering Industries Federation of Southern Africa (SEIFSA) Chief Economist Dr Michael Ade commented.

Ade said although the past nine months to the end of quarter four 2017 have seen the real GDP recover from the contraction that marked the previous nine months, challenges to the supply side of the economy and especially in industrial production still prevailed. He said the benefits of a slight up-tick in production in the M&E cluster in 2017 was still not felt by local companies due to prevailing economic challenges, with the production trend still remaining variable and being largely pro-cyclical.

“It is clear that while the recent political forces of change have the potential to improve on perception, credit worthiness and the output stance of the domestic economy, there is still more work to be done in all industrial sectors in general and in the manufacturing sector in particular. The contribution of the manufacturing sector to the broader economy has declined over the years, from roughly a 24% contribution to GDP in the 1990s to a low 12.29% in 2017, with dire consequences on jobs levels,” Ade said.

He said that, moreover, the variability in output in the manufacturing sector – including its M&E sub-components in the years after the 2014 crisis – was still evident, underscoring the need to continue exploring ways of reviving the fortunes of the sector.

“Clearly, there is still more work to be done and all stakeholders have to pool resources together to ensure a return to the glorious growth levels last recorded in the early 1990s. Accordingly, a continuous rebound in production is needed if the manufacturing sector is to regain its position as the main contributor to the broader economy.

“This objective is possible, given the improvement in business confidence and sentiments since the beginning of this year, against the backdrop of a domestic political shift,” Ade concluded.

Critical Technical Infrastructure For Industrialization Efforts

The Deputy Director-General of Industrial Policy Development at the Department of Trade and Industry (the dti), Garth Strachan says that it is of the outmost importance for the Southern African Development Community (SADC) to get a superior understanding of the technical infrastructure and its capabilities to achieve common industrialization efforts.

Strachan was speaking at the 33rd SADC Technical Barriers to Trade (TBT) Structures Meeting in Johannesburg recently.

The annual meeting is co-hosted by the dti together with the SADC Secretariat and is attended by all 16 SADC Member States. It is aimed at laying the framework for the continued implementation of the Technical Barriers to Trade (TBT) Annex to SADC Protocol on Trade.

Strachan indicated that while the area of technical infrastructure was little understood and does not usually occupy the public discourse because of its technical and scientific nature, it had the ability to create cohesive and strong regional growth when implemented properly.

“Our biggest challenge is that we need to be looking at this as a region in order to get a superior understanding of how critical technical infrastructure institutions and their capabilities are for this common purpose. To do this we need to ensure that we secure intra-regional investment in trade and industrial integration and that together with the private sector we build industries that are characterized by a high-level of technology, value-addition and exports,” said Strachan.

The week-long programme centred on discussions to progressively eliminate unnecessary TBT amongst SADC members and other regional and international trading blocks and promote an infrastructure for quality.

“Achieving this would require policy coherence within the perimeters of national independent sovereignty. An education and skills strategy in support of this effort, a system of science technology and innovation to support this effort and economic infrastructure and what I refer to as the absolute necessity of technical institutional capabilities to support this effort,” he said.