Home Blog Page 49

TRINITY PROJECT TO HELP SMES TO BENEFIT FROM ROBOTICS, IOT AND CYBERSECURITY TECHNOLOGIES

Robotics, automation and cybersecurity technologies are critical to the factories of the future. The TRINITY opening event on “Robotics for agile and competitive manufacturing” gave concrete examples of how these technologies can help to increase productivity, agility and make lot size one economically feasible. The TRINITY project will offer financial and technical support to European small and medium-sized companies to test and benefit from these technologies through two rounds of open calls.

Minna Lanz.

Robotics, automation and IoT play a critical role in the factories of the future. These technologies are essential for manufacturing companies to survive in the next decade, increase their competitiveness and production capacity. Nevertheless, only a small percentage of companies is using these technologies. Projects such as TRINITY can speed the technology transfer and shorten time to market. This was the main outcome of the opening event organized by the TRINITY project on 19 September 2019 during the EMO Hannover fair.

The shortage of highly skilled manufacturing workers was one of the main challenges mentioned by the speakers behind the need for robotics and further automation. “In 2030 the manufacturing sector will experience real difficulties in finding skilled workers” said Minna Lanz, TRINITY project coordinator and professor at Tampere University. “In 2040 we won’t have enough people to work in the factories. Automated factories are necessary in order to deal with this problem”, she added.

Another challenge is the increasing complexity and demand for customization of products. To this respect, Tomi Kankainen, CDO at Fastems, one of the TRINITY partners, highlighted the real challenge was not only about producing lot-sizeone but about flexible batch production, this is, producing lot sizes from one to hundreds or to thousands at the same time. He also explained how, as part of the TRINITY project, Fastems developed a new robotized manufacturing cell able to adapt automatically to manufactured products and production lot-sizes thanks to the reconfigurability of hardware and software.

Boris Fiedler, Digital Leader at ABB Robotics, highlighted the important role of robots in meeting these challenges and their benefits in terms of efficiency, reliability and flexibility. He provided a vision of the future factory based on the ABB new robotics factory in Shanghai. This vision was characterized by further convergence, digital integration and production based on automated cells rather than on fixed assembly lines. In this context, Automated Guided Vehicles (AGVs) would be used to deliver parts to the production robots and to collect finished parts and move them to other cells as necessary.

Andreas Walbert.

Andreas Walbert, Business Development Manager at Kuka presented the Kuka matrix production system. A similar concept than the one presented by ABB, already successfully implemented in a factory of the future dealing with the industrialisation of Additive Manufacturing at Premium AEROTEC in Varel (Germany). Together with Pascal Haas, Head of Automation at Erowa they showcased a concrete example on the automatization of die and mould workshops. The example highlighted the importance of logistics automation by using mobile robots.

The need to raise awareness about cybersecurity risks in a context characterized by further integration was also highlighted by the speakers. Ulrich Seldeslachts, CEO of LSEC, another TRINITY partner pointed out that manufacturing, with 31% of all incidents, was leading the number of cybersecurity incidents reported. The number of attacks is increasing exponentially every year and it is important to raise awareness and take the necessary measures to avoid theft of sensitive data, financial losses, loss of productivity and damage to the company’s reputation.

Florian Ernst, Managing Director of RESADO pointed out that the long product lifetime of industrial equipment is an important challenge from the point of view of cybersecurity He also introduced a new technology developed by his company aiming at protecting IoT devices. This new technology is based on the creation of a digital fingerprint for a device which allows for its unique identification and secure communication.

TRINITY open calls for funding

TRINITY is a four-year project, which started in January 2019 and it is funded by the European Union’s Horizon 2020 research and innovation programme. It aims at helping European small and medium-sized companies (SMEs) to implement and benefit from new digital and robotic technologies to increase their agility and innovation capability. The focus areas are robotics, IoT and cybersecurity.

In order to reach these objectives TRINITY will develop a series of use cases to demonstrate how novel robot and digital technologies can contribute to increasing the agility of production processes across different manufacturing sectors. As part of the project two rounds of open calls for funding will be launched. Through these open calls SMEs can team up with technology providers, OEMs (Original Equipment Manufacturers), end-users and other partners to get funding and technical support to test some of the technologies showcased or to propose completely new demonstrators. Companies can get up to EUR 300,000 per demonstrator (maximum funding rate of 70%). The first call, for which EUR 4 million will be made available, will open on 20 November 2019. Companies will have three months to present their proposals.

KRAKEN – WORLD’S LARGEST AND MOST ACCURATE MULTI-MATERIAL 3D PRINTING MANUFACTURING SYSTEM

Recently the KRAKEN system has been presented at the AITTIP Technology Center, in Zaragoza (Spain) in the frame of project final conference to 120 attendees from Spain, UK, Germany, Italy, Greece and USA.

The KRAKEN is a research result from H2020 EU program, capable of producing parts through Additive Manufacturing alternating material deposition with subtractive operations (layerby-layer) within a maximum working area of 20m x 8m x 6m.

José Antonio Dieste, Aitiip researcher and project coordinator said, “the machine is ready for the market, it has been tested in real manufacturing environment and project demonstrators have been validated by the companies in real conditions. We can deliver now pieces or install Kraken cells according to client demands.”

Project partners presented project results to the audience and expressed their aim to revolutionize the manufacture of large parts, both metallic or hybrid, thanks to the quality and size of final parts, which together with the efficiency of the process and the speed of production, makes it an all-in-one manufacturing system unique in the world.

Besides system calibration, frame alignments and realtime correction, quality inspection of semi-finished or final parts is a very important step and an additional advantage of the embedded metrology system. In this sense Markus Steiner (Hexagon Manufacturing Intelligence) enlightened “Due to the integrated Leica Absolute Tracker, parts manufactured by the KRAKEN machine can be digitized in 3D and checked against the CAD design to verify the quality of manufacturing over the full volume of the machine, even fully automated if needed.“

“Guaranteeing accuracy in large workspaces (100m2 ) is a challenge that Kraken has solved by integrating real time laser tracking technologies within the closed loop control of the robotic system. Thanks to this method, tool precision can be assured down to 0,1mm.” Francesco Crivelli, CSEM SA was responsible for designing the control algorithms and implementing the software.

Industrial companies also showed their interest in additive manufacturing results. AIRBUS, the aircraft manufacturer, confirmed that hybrid technologies are not the future but the present and as of now the company is going to demand tools and tooling manufactured with this technology no matter where or who produce it.

Not only aircraft industry is interested, also automotive industry demonstrated their interest. Vito Guido (GroupMaterials Labs, CR Fiat) confirmed that this technology will be used for sure for mock-up productions, it has demonstrated that for short productions the technology offers quality results on time.

Indeed, thanks to the KRAKEN machine it is now be possible to produce very large prototypes, such as designs for architecture and the creative and cultural industries, concepts for the transport sector, as well as large scale models for wind tunnels in the case of the aerospace industry.

The Additive Manufacturing system, provides metallic material using WAAM at a deposition rate of 1.5l/h. The KRAKEN machine also includes a bi-material resin extrusion system which can reach deposition rates of 120 kg/h. The metallisation process can reach deposition rates of 6kg/h.

In addition, the subtractive capabilities of the machine allow for cutting, sanding and polishing operations, reaching 2mm of cutting at 10m/minute.

All these operations are controlled by a laser tracker, which monitors and controls the position of the head 1000 times per second, correcting its position automatically. The system also incorporates two types of cameras and artificial vision systems to control the deposition flows and for the subsequent verification of the piece, through three-dimensional scanning.

The possibility of building large metal and resin parts by means of high-quality 3D printing has raised the interest of a wide part of the industry. Some demonstrators of the project are already finished. These demonstrators aimed at validating the functionality of the system and they will be presented for the first time at the facilities of AITTIP Technology Center in Zaragoza (Spain).

Hybrid lining panels for road tunnels of 3 · 1.2m have been manufactured for Acciona, one of the consortium partners. Thanks to the combination of resin and metal, electrical connections can be made much easier.

Regarding the automotive sector, a mock-up car of one of the latest Pininfarina car models has been produced to validate its design. The built piece has a size of 2.2x1x0.6m and a weight of 250kg.

These are some of the real applications that have already been tested, although the sectors that can benefit from this system are much broader, since it offers low cost, high quality, fast and efficient alternatives for the die and mould sector and to the tooling of large parts.

This manufacturing system is the result of a European Project coordinated by AITIIP in which 15 partners have collaborated for the last three years.

ISCARDRILL – NEW GRADE IC5500 FOR STEEL DRILLING

ISCAR is launching IC5500 – a new MTCVD grade for drilling carbon and alloyed steel (ISO P).

The new grade features a new multi-layer and special post-coating treatment to substantially prolong tool life and strengthen insert toughness, while improving operational reliability.

The new grade will be available on square inserts that are used on DR drills: 3340386 SOMX 060304-DT IC5500, 3340385 SOMX 070305-DT IC5500, and 3340384 SOMT 09T306-DT IC5500.

The inserts made from IC5500 are aimed for use only in the outer pocket of DR drills (the inner insert should be an IC908 or IC808 PVD coated insert).

The upgraded IC5500 MTCVD coating enables improved toughness, chipping resistance and thermal crack resistance, while the combination of new coating and new treatment improves overall performance and process reliability.

The coating includes a post coating treatment to reduce residual stresses and improve chipping resistance, Alpha Alumina to reduce crater wear and improve chipping resistance, a thick Al₂ O₃ to improve thermal crack resistance and an intermediate layer to enhance adhesion between the Al₂ O₃ and TiCN layer in the bonding area, improving peeling resistance. The TiCN layer improves flank wear resistance and the adhesion layer enhances adhesion with the substrate, preventing peeling during machining.

IC5500 provides an excellent solution for alloy and carbon steel drilling.

For more information please contact TaeguTec – Tel: 011 362-1500.

TAEGUTEC’S DRILLRUSH DEEP HOLE DRILL

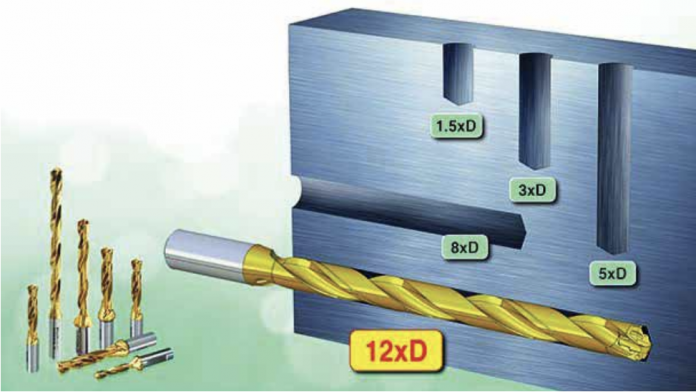
The DrillRush 12xD drill range for deeper hole drilling and the body’s polished flutes offers smooth chip evacuation without damaging the surface finish.

The strong delivery of coolant through its twisted body channels enables a widened gullet design and keeps the drill and workpiece material cool at all times while minimizing cycle times when drilling diameters from 12 millimeters to 22.9mm.

The DrillRush 12xD’s offers accurate performance due to the good run-out made possible due to tight manufacturing tolerances, while other important factors are repeatability, smooth surface finish and high productivity for deep hole drilling applications which are achieved without the need for pecking cycles.

To promote machining convenience in hole making applications, the 12xD body can be accentuated with TaeguTec’s chamfering rings which drill and chamfer in a single operation in order to minimize cycle times as well as inventory and tooling cost for improved cost effectiveness.

To add value by enabling stable machining and longer tool life, TaeguTec chamfering rings use two TT9080 specially treated, multilayered, physical vapor deposition coated CRNG inserts on either side which can machine any type of alloy.

TaeguTec also supplies special plugs with an internal thread for coolant connections used on lathes that can be pressed into the cavity on the back end of the shank.

For more information please contact TaeguTec – Tel: 011 362-1500.

THE NEW S33 – THE GOOD VALUE SOLUTION

FOR INDIVIDUAL REQUIREMENTS

Universal and flexible are the features of the new S33 CNC universal cylindrical grinding machine from STUDER. It can grind small to large workpieces in single batch, small or large series and is available with centre distances of 400mm, 650mm, 1000mm, 1600mm and a centre height of 175mm. The changeover from grinding between centers to live spindle grinding takes place in record time. Complex workpieces are easily ground in just one clamping.

The basis for the universal cylindrical grinding machine S33 is the machine bed made of solid Granitan® S103. Thanks to its favorable thermal behavior this offers a high degree of dimensional stability, while short-term temperature fluctuations are largely compensated for by the mineral casting. STUDER has redesigned the machine base geometry and supplemented it with an innovative machine base temperature control, which ensures fast and stable production. The mounting of the dressing unit on the double T-slot of the longitudinal slide massively reduces time needed for set-up or changeover of the machine.

While the S33 is based on the STUDER T-Slide concept, which now features an extended X-axis stroke of 370mm, STUDER offers various wheelhead versions. The turret wheelhead with a 1° Hirth coupling and automatic swivel can accommodate up to two external and one internal grinding spindle and is equipped with the latest generation of contact detection. The external wheelhead with a grinding wheel right, can be manually set to 0°, 15° and 30°. The machine set-up and changeover costs can be reduced thanks to the turret wheelhead with multiple grinding wheels and the fast set-up software Quick-Set. The S33 can easily handle internal-, external- and face grinding in one clamping which leads to an even higher efficiency in complete machining. The C-Axis, with an option of either a direct or indirect measuring system, allows the grinding of forms and threads. The S33 can also be equipped with a chuck workhead, specially designed for grinding chuck parts.

More than a hundred years of grinding experience is integrated in StuderWIN, which enables safe programming and efficient use. StuderTechnology requires just a few parameters to automatically calculate precise grinding parameters in just seconds. Good quality and a stable process is assured right from the beginning. The optional integrated modules such as StuderForm, StuderThread or StuderContourBasic extend the functionality of the machine. The hand-control device PCU makes it possible to set up the machine close to the grinding process. With electronic contact detection, downtimes can be reduced to a minimum. With the standardized loader interface, the S33 can also be automated.

For more information, please contact Retecon – Tel: 011 976-8600.

STUDER favorit

The STUDER favorit is offered with centre distances of 400, 650, 1000 and 1600mm. While it is suitable for short to long workpieces, it can be used universally.

This CNC universal cylindrical grinding machine is designed for grinding in individual and batch production and can be automated. It can subsequently be easily adapted to other grinding tasks using various accessory kits such as in-process gauging, balancing system, contact detection and length positioning.

The favorit is a very cost-effective machine. As with all STUDER cylindrical grinding machines, the proven solid Granitan® machine base ensures the highest precision, performance and reliability. The full enclosure ensures an optimal view of the grinding process. The wheel-head, which can be automatically positioned every 3°, can take one belt-driven external and internal grinding spindle respectively.

The favorit is a very cost-effective machine. As with all STUDER cylindrical grinding machines, the proven solid Granitan® machine base ensures the highest precision, performance and reliability. The full enclosure ensures an optimal view of the grinding process. The wheel-head, which can be automatically positioned every 3°, can take one belt-driven external and internal grinding spindle respectively.

The STUDER favorit has an integrated coolant tray and a machine base with temperature control. Potential deformations of the slide on the Z-axis are eliminated. At the same time the “active temperature control” option brings the machine to operating temperature faster.

The practical STUDER grinding software with its proven StuderPictogramming means that even less experienced users can quickly and practically program grinding and dressing cycles. The modern and user-friendly design is complemented with a touch-screen panel, which allows the operator to easily and directly control the machine. Service doors at the rear and on the right of the machine ensure high ergonomic efficiency during machine operation. Development, production, assembly and inspections of STUDER products all takes place in a process-oriented manner and complies with the stringent directives stipulated in VDA 6.4 and ISO 9001.

For more information, please contact Retecon – Tel: 011 976-8600.

TIMESAVERS 42 SERIES ROTARY BRUSH MACHINE

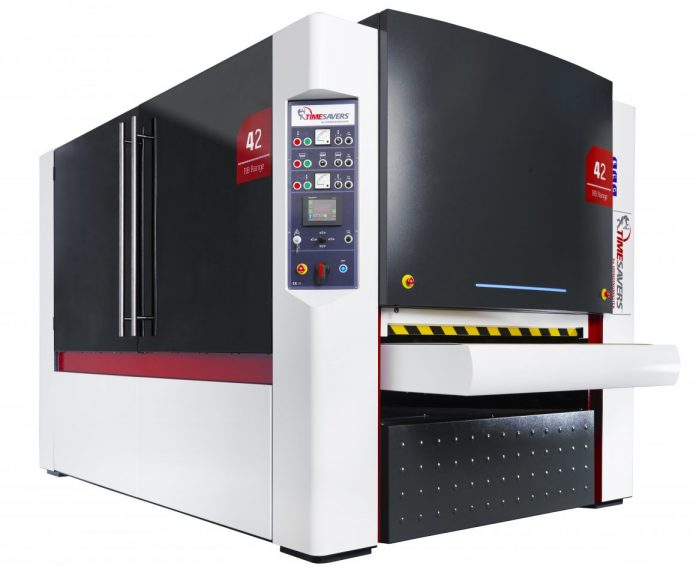
The technologically-advanced 42 Series Rotary Brush machine adds more value to steel processing businesses, with the allnew add-on underside finishing machine.

This add-on machine is placed in front of the machine, and serves to remove burrs from the underside of workpieces before they enter the main deburring process. The advantage of this is that deburring can be done with one single pass – in half the time it previously took.

In the world of fabrication today, there is overwhelming demand for increased speed of production, while still meeting quality requirements. The 42 series meets these requirements in full. With modern fibre laser technology, in some clients’ fabrication centres, the output of newly cut components has reached unprecedented rates. With the add-on machine, Timesavers has therefore ensured that the process of deburring and edge-rounding effectively eliminates any production bottlenecks and increases productivity and profitability accordingly.

In addition, the add-on machine allows the 42 Series to be more easily integrated into fully automated processing lines.

Not only does the 42 series offer improved deburring, rounding and finishing in one processing step, it is also able to process a large variety of sheet thicknesses and metal types. This machine is very versatile, as it can deburr and grind small parts from 30mm to large parts up to 1600mm, while being capable of processing a large variety of materials including stainless steel, aluminium, zincor, zinc and laser film products.

The machine features a centrally installed and user-friendly control panel and an automatic table opening of 0 – 100mm. To ensure a perfect finish, the machine has a carousel rotating brush head equipped with eight brushes, four rotating to the left and four to the right. The frequency-controlled conveyor belt feeds at speeds ranging from 0.2 to 8 m/min. Window panels and a well-lit interior make it easy to keep a visual check on processing.

The brushes have an extremely long service life of approximately 3,000 hours. However, when brushes or belts need to be replaced, there is a quick replacement system for virtually uninterrupted production. To monitor feed status, the machine is equipped with LED beams on the infeed and outfeed and the vacuum table has an automatic cleaning cycle.

While the most common finish achieved by the Timesavers wide belt machine is the straight line or grain finish for decorative or aesthetic purposes, some customers may require a random, circular or orbital scratch pattern. Timesavers offer machines for each of these requirements and will run samples to demonstrate the required finish results accordingly.

Alternatively, the component can be given a finish with the surfaces prepared for painting or for receiving a specific micro-finish. If any customer has a specific deburring challenge, the First Cut and Timesavers teams are always ready and willing to consult, in order to find an optimal deburring or grinding solution.

Many Timesavers customers have found that switching from time-consuming manual deburring to an automated Timesavers machine has not only saved them a substantial amount of operational time – but substantial costs as well.

Ultimately, for unmatched high-end finishes, the 42 Series is the ideal solution for the fabricator or manufacturer dedicated to supplying their customers with premium standard, quality-cut and finished components.

For more information, please contact First Cut – Tel: 011 614-1112.

GF MACHINING SOLUTIONS’ FORM FAMILY OF DIE-SINKING EDM MACHINES

Whatever the current or future diesinking electrical discharge machining (DSEDM) challenge, GF Machining Solutions’ AgieCharmilles new FORM family of DSEDM machines are future-shaping solutions to advance manufacturers’ success.

The AgieCharmilles FORM X, FORM S, FORM P and FORM E series advance their forebearers’ software and technical innovation, such as the renowned AC FORM human-machine interface and GF Machining Solutions’ legendary EDM know-how. Whether the requirement is a single machine for straightforward use or full automation, these new, easily integrable FORM solutions position users to meet every challenge, with greater flexibility and machining accuracy to eliminate costly manual operations.

These eco-friendly solutions offer Econowatt technology to save energy, a variety of Industry 4.0-oriented connectivity features to support manufacturers’ digital transformation and eTracking software for EDM process monitoring and full traceability.

From faster rib machining to micromachining, the AgieCharmilles FORM family of DSEDM solutions is evidence of GF Machining Solutions’ continued and significant investments to advance DSEDM research. The result is that AgieCharmilles FORM series users achieve performance like never before in machining with graphite and copper. Perfectly repeatable machining of micro cavities is just one example of the manufacturing challenges expertly resolved by this range of DSEDM solutions. In parallel, this series’ iGAP technology enables the rigidity of plastic injection molded end products with deep, plastic reinforced ribs; it ensures fast, accurate machining of rib cavities with superior respect for the required demolding taper and VDI homogeneity throughout the cavity surface.

Manufacturers requiring maximum use of their AgieCharmilles FORM machine can exploit the range’s eConnectivity features and MTConnect capability to stay informed of the machine’s status. Moreover, the FORM E 350 allows switching between DSEDM to drilling EDM, allowing extended use of the machine. Automation is another way AgieCharmilles FORM series machine users can extend their productivity: In today’s fast-paced manufacturing environment, unattended manufacturing is a must, so the AgieCharmilles FORM E, P, S and X series solutions can be connected to external robots and offer integrated pallet as well as electrode changing solutions.

AgieCharmilles FORM X – extreme and uncompromising accuracy

Extreme accuracy, highest precision in mass production, and unparalleled productivity come together as future-shaping solutions with the AgieCharmilles FORM X series. This series’ TECFORM ensures highest accuracy and reproducibility on both big and small parts. This is due to the fixed table and stiff machine base delivering perfect positioning accuracy along the entire axis travel. The result – high precision throughout the machining area.

Furthermore, manufacturers’ mass production of highly precise micro parts is assured by the AgieCharmilles FORM X series precisionenhancing qualities. High quality, automated mass production is easily within reach, thanks to these machines’ dynamic thermostabilization.

As manufacturers face ever-shorter delivery time, the AgieCharmilles FORM X series delivers high running time – no manual intervention necessary – thanks to its vast Automation capabilities. These include accommodation of linear, rotary or robot pallet and electrode changers, as well as smart features such as Part Express and Job List management. Users can ramp up their profitability by automating their production, thanks to the AgieCharmilles FORM X series’ ability to accommodate two frontoriented machines on each side of the robot.

AgieCharmilles FORM S: big success in micro-profiles

GF Machining Solutions’ AgieCharmilles FORM S solutions open new fields for miniaturization, optimize productivity, ensure lasting accuracy, and have the automation readiness to position users for the future.

New fields of miniaturization are opened by the maximum respect for details provided by these solutions’ Intelligent Speed Power Generator (ISPG) evolution and specific micro technologies. The latest-generation ISPG makes it possible to use a smaller-than-ever spark gap to remove minute amounts of material in order to achieve finest geometric details.

At the same time, AgieCharmilles FORM S 350 users achieve more with less by using fewer electrodes to achieve greater detail. Behind this achievement lies this solution’s process, enabling such a small electrical current that electrode wear becomes insignificant. Consequently, only few electrodes are needed to machine cavities and this represents a significant advantage over similar products.

High, lasting accuracy is made possible by a specific controlled process during production of the AgieCharmilles FORM S series, so the machine retains stable accuracy across its lifetime. Stable performance is ensured by this solution’s standard thermostabilization equipment.

Moreover, the AgieCharmilles FORM S 350 is Automation-ready and GF Machining Solutions has a perfect automation configuration to meet every need, whether the requirement is a simple linear tool changer or any kind of robot in any cell.

AgieCharmilles FORM P

As the preferred choice for automated parts production with adapted investment cost, the AgieCharmilles FORM P series puts perfect results and high productivity at the user’s fingertips.

Perfect results are enabled by the intuitive, easyto-learn and easy-to-use die-sinking EDM process ensured by GF Machining Solutions’ AC FORM human-machine interface (HMI). Designed for productivity, the FORM P series leads the way in high running time without manual intervention, thanks to the series’ multiple Automation choices from a linear, rotary or robot pallet or electrode changer as well as smart features like Part Express and Job List management.

Perfect results are enabled by the intuitive, easyto-learn and easy-to-use die-sinking EDM process ensured by GF Machining Solutions’ AC FORM human-machine interface (HMI). Designed for productivity, the FORM P series leads the way in high running time without manual intervention, thanks to the series’ multiple Automation choices from a linear, rotary or robot pallet or electrode changer as well as smart features like Part Express and Job List management.

AgieCharmilles FORM E

This multifaceted performer delivers best value for the investment in the production of molds and parts. It offers superb accessibility, automated dielectric management, extended Automation capabilities, ever-evolving technological improvements and the availability of GF Machining Solutions Customer Services’ rConnect world of digital services.

Automatic dielectric management increases machining time while reducing human intervention. Filling and emptying the work tank is now automatic, and the dielectric height can be adjusted while running a program. Furthermore, the AgieCharmilles FORM E series offers extended Automation capabilities, including linear and rotary tool changers for machines produced in Switzerland. In addition, the FORM E 350 can accommodate an external robot.

Thanks to GF Machining Solutions’ continuous improvement of EDM technology, AgieCharmilles FORM E users get the EDM performance necessary to address their daily challenges. With rConnect, GF Machining Solutions continues to push technological boundaries to deliver the future of services—today. As the machine tool industry’s most in-depth digital service platform, rConnect represents this GF Division’s Industry 4.0 vision of intelligent and high-performing services. AgieCharmilles FORM X, S, P and E series machines are all rConnect ready.

For more information, please contact Retecon – Tel: 011 976-8600.

Slowdown in Manufacturing Output is Concerning

SEIFSA CEO Kaizer Nyatsumba.

The slowdown in the broader manu-facturing sector’s production, as reflected in manufacturing production figures released by Statistics South Africa (Stats SA) recently, is concerning, the Steel and Engineering Industries Federation of Southern Africa said recently.

Speaking after the release of the data, SEIFSA Economist Marique Kruger said against the backdrop of a struggling economy and the plethora of challenges faced by manufacturing companies, production volume from businesses took a knock and the official output data reflects a constrained business environment for manufacturing companies.

The latest preliminary seasonally-adjusted data released captures a year-on-year slowdown in production in the broader manufacturing sector in June 2019 when compared with May 2019, with output dipping to -3.2 percent in June 2019, from 0.4 percent recorded in May 2019. Moreover, the volatility in the data is more pronounced when analyzed on a month-to-month basis.

“The dip in the year-on-year manufacturing output data highlights the urgent need to deal with underlying dynamics leading to a depressed economic environment and high unemployment numbers,” Kruger said.

However, she pointed out that the expectation is for companies in the broader manufacturing sector in general and the metals and engineering sector in particular to take advantage of a possible up-turn when the much-anticipated quarter 2 GDP data are released. The upturn in GDP is imperative in order to grow the domestic economy and create jobs in the long term.

Now in its fifth year, the Indaba is organized and hosted by SEIFSA.

Are South African Manufacturers Ready to Take Advantage of the Opportunities Presented by AfCFTA

May 2019 saw the official launch of the much-anticipated African Continental Free Trade Agreement (AfCFTA), which not only provides access to a continent-wide market of 1.2 billion people worth $2.5 trillion, but also effectively places Africa as the world’s largest free trade zone by population since the 1995 creation of the World Trade Organization.

The agreement which effectively breathes life into the largest trading bloc in the world enabled the creation of a single continental market for goods and services, with free movement of business people and investments.

“There is no doubt that the AfCFTA has remarkable potential for intra-continental trade.
The deal cuts duties on 90% of goods. It is expected to boost regional and international trade and to improve on the proportion of trade by African nations with continental neighbours,” Steel and Engineering Industries Federation of Southern Africa (SEIFSA) CEO Kaizer Nyatsumba said.

The deal presents a unique opportunity for South African companies to trade with those of other regions, such as in the West and Central Africa regions, where there is a dearth of trade agreements he said.

But just how ready are South African manu-facturers to take advantages of the opportunities presented by the AfCFTA? The assessment of local manufacturers’ readiness will be discussed at the upcoming Southern African Metals and Engineering Indaba taking place at the IDC Conf erence Centre in Sandton on 11 and 12 September.

Taking part in this plenary session will be Deloitte Managing Director: Africa and Emerging Markets Dr Martyn Davies, Africa House Director Duncan Bonnett, Department of Trade and Industry Africa Multilateral Economic Relations Chief Director Wamkele Mene, Manufacturing Circle CEO Philippa Rodseth and SEIFSA Vice-President Alph Ngapo.

Nyatsumba said that panellists in this plenary session will also propose necessary interventions to ensure that companies operating in the metals and engineering sector are ready to take advantage of the opportunities presented and to be competitive.