Home Blog Page 80

Dr Roland Feichtl New CECIMO President

The CECIMO General Assembly recently elected Dr Roland Feichtl as President for a period of two years.

Feichtl has been entrusted with the responsibility of leading the European Association that represents more than a third of the world machine tool (MT) production.

Dr Roland Feichtl, President of CECIMO

Feichtl is responsible for machine-tools and automation within the MTB-Group (1.000 m revenue and 5500 employees), and Group CEO of several traditional machine-tool companies like, for example, 200 years’ Mauser-Werke Oberndorf (Germany) or fineboring specialist Krauseco in Vienna (Austria) which has more than 100 years of experience. Here, Feichtl developed Krause+Mauser Group to become the world market leader for connecting-rodmachines and laser-cracking-technology and a premium supplier of the international automotive industry. He is, also, co-owner and Chairman of the Supervisory Board of the company Feiba in Traun (Austria), specializing in Automation and Robot-Application.

Feichtl joined CECIMO in 1999 as a Delegate, was Chairman of Technical Committee, CECIMO Vice-President and Board Member for the last 17 years.


Inside 3D Printing – Sounding Out The Future

For example, new technologies – in line with the Gartner Hype Cycle – usually pass through five stages of public attention.

A technological trigger seizes people’s imagination and generates exaggerated expectations, which rapidly give way to disillusionment. Only then will realistic assessments come to the fore, enabling the technology concerned to be productively used.

A productive plateau of this kind has been achieved in the 30-year history of technology by rapid prototyping, for example, by layerby- layer construction of single pieces and sample components from CAD data and by 3D printing of hearing aids. Applications in the fields of dental technology and automaking have left the disillusionment phase behind and have long since been evolving into successful models. Other processes like 3D printing of consumable materials, surgical implants or bioprinting of human tissue still have a long way to go.

What business models for additive manufacturing might look like is exemplified by Protiq GmbH, a subsidiary of Phoenix Contact GmbH & Co. KG and represented at Inside 3D Printing by Johannes Lohn. Industrial customers upload the data of their 3D models to Protiq’s website, select the material they want, and place a printing order. The models will then be printed within a few days, and dispatched worldwide. “The quality is in some processes so high that intensive reworking is not needed. It suffices to polish the workpieces at certain points, and they can be used directly,” emphasizes Stefan de Groot, Additive Manufacturing Technologist at METAV’s Press Forum in Blomberg. He sees the advantages in significant cost reductions, particularly for small batch sizes, but also in greater functional depth. Close-to-contour cooling and weight reductions based on topological optimization, for example, are reflected in simpler handling.

“As an international meet-up for the sector, Inside 3D Printing provides an opportunity to talk with top-ranking speakers and companies,” explains Prof. Dr.-Ing. Franz- Josef Villmer from Ostwestfalen-Lippe University, who will be acting as the host for this conference. “In the shape of Dr. Phil Reeves and Prof. Thierry Rayna, for example, we have brought on board true pioneers and visionaries of additive manufacturing, whose keynotes are definitely something for visitors to look forward to.”

Visitors to METAV will thus perceive Inside 3D Printing as an ideal supplement to the fair’s other attractions. While at the exhibitors’ stands they will experience the latest state of the art, the conference at the fair will provide them with insights into what companies have in the pipeline for the future. But trade visitors who travel to Düsseldorf only for the Inside 3D Printing event will also find it definitely worthwhile. To quote Prof. Villmer: “Because we are moving away from frontal lectures and giving preference to meaningful interaction between speakers and conferees, a visit is well worthwhile for all stakeholders in 3D printing. They will meet experts with huge funds of specialized knowledge, able to provide a crucial boost for their own work.”

Collaboration For Curative Technology

The requirements applying to production systems for medical technology are enormously stringent: the certified lines have to operate faultlessly, meet strict hygiene regulations, and document every important step in the production process.

Unsurprisingly, innovative firms opt for intercompany teamwork here: the Medical Area of METAV 2018 will open new interesting chapters of collaboration here in 2018 – in Düsseldorf, the IMSTec company from Rhineland-Palatinate will be showcasing a new production line that it has developed together with the machine tool manufacturer Schütte from Cologne, Germany.

“We develop end-to-end solutions for medical technology,” explains Edgar Mähringer- Kunz, Managing Director of IMSTec, Klein- Winternheim (near Mainz, Germany). “The customers come to us with a job profile: we transfer this to a specification and analyse it for weaknesses and risks.” This is followed by line manufacture, commissioning and support within the framework of maintenance agreements.

Collaboration is usually arranged in three different ways: IMSTec, for example, has developed and built a fully automatic line including all production processes, on which a customer is manufacturing implants that are fitted directly in the eye, and supply it with medication. The technical term used for this is “complete process development outsourcing”. To quote Mähringer-Kunz, “this was an ideal case, where we developed the processes in parallel to the product, and at the same time built the complete line.” Other customers have developed a production process that’s already been clinically approved, which IMSTec is then progressing from laboratory status to an industrial process. The third variant involves optimizing, expanding and automating an already-existing production operation.

All three variants are characterized by a common denominator: for example, manufacturers of lines for medical technology have to comply not least with the stipulations laid down in DIN EN ISO 13485 (a standard covering a comprehensive management system for the design and manufacture of medical products), stringent statutory specifications like those of the USA’s FDA and the GMP rules (Good Manufacturing Practice). In addition, they have to pass various audits by customers. “So the quality and documentation system is already very unusual,” emphasizes IMSTec’s Managing Director. “What’s more, you have to remember that this sector, like the aviation industry, cannot permit itself any mistakes whatsoever. For example, we automated a line for packing orthopaedic components, because within two years a part had been mixed up one single time during manual packing. This is why systems for dependable monitoring and tracking of process conditions, known as traceability, play an extremely important role.

New EU stipulations for medical products already met

The European Union has taken on board these stringent requirements with the new legal framework for medical products in force since 2017 (Medical Device Regulation – MDR), which obligates manufacturers of medical products to modify their processes appropriately and provide their products with UDI (Unique Device Identification) by May 2020 at the latest. “All our lines already possess the appropriate systems for individual-part tracking,” says Mähringer-Kunz. “We can label, unambiguously identify and trace each individual part. It’s also possible to acquire all parameters of a product lifecycle – so for years now we’ve already been implementing parts of Industry 4.0.” This means that on these lines products can be dependably manufactured in ultra-small series or even Batch Size One. The highlights here include the world’s first fully automated lines for producing eye implants, for example.

When it comes to automation, the company has recently begun to collaborate with the machine tool manufacturer Alfred H. Schütte from Cologne in developing automated production lines, which can be used to completely machine cast knee implants, for example. To quote Mähringer-Kunz, “we’re already engaged in contractual negotiations with the first customers.” So far, he continues, the solution concerned possesses a unique selling point in that knee implants, for example, can be manufactured significantly more efficiently and productively – and this “with an attractive return on investment”.

Turning: Intelligent Machine Productivity In A Compact Footprint

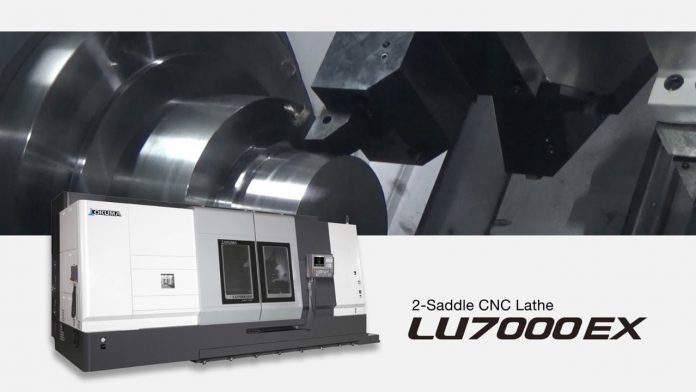
Okuma Corporation has developed a large 2-saddle CNC lathe, the SIMUL TURN LU7000EX, for the large, difficult-to-cut parts of heavy industry.

The LU7000 EX has a large work envelope that handles super-large diameter, long parts with a maximum turning diameter of ø900mm and spindle bore diameter of ø560mm (optional). It is a 2-Saddle CNC lathe that achieves high productivity, including simultaneous turning with upper and lower turrets and follower rest applications.

A high output, high torque spindle enables heavy-duty cutting with turning capacity of 10mm2, while a first-in-thisclass, newly-developed milling turret achieves process-intensive machining of large parts in with powerful millingtool spindles that have an axial milling capacity of 120 cm3/min. Four different main spindles are available to match the workpiece, from a bore diameter of ø200mm and spindle speed of 1,500 min- 1 to ø560mm and 350 min-1, respectively, for the best machining with the best spindle. Innovative production is achieved with a rich array of applications, including simultaneous machining with upper and lower turrets, a long boring bar attached to the upper turret and a follower rest mounted on the lower turret.

The range of functions provided with Okuma’s next-generation CNC, the “OSP suite”, supports smart manufacturing with advanced Okuma Intelligent Technologies including the Thermo-Friendly Concept to maintain stable machining accuracies during long runs, Machining Navi for optimal cutting conditions required for turning, milling and threading and the Maintenance suite visual control tool for maintenance activities.

For more information contact F&H Machine Tools – Tel: (011) 397 4050

Turning: Innovating Production With A Large Smart Machine


Okuma Corporation has developed a large 2-saddle CNC lathe, the SIMUL TURN LU7000EX, for the large, difficult-to-cut parts of heavy industry.

The LU7000 EX has a large work envelope that handles super-large diameter, long parts with a maximum turning diameter of ø900mm and spindle bore diameter of ø560mm (optional). It is a 2-Saddle CNC lathe that achieves high productivity, including simultaneous turning with upper and lower turrets and follower rest applications.

A high output, high torque spindle enables heavy-duty cutting with turning capacity of 10mm2, while a first-in-thisclass, newly-developed milling turret achieves process-intensive machining of large parts in with powerful millingtool spindles that have an axial milling capacity of 120 cm3/min. Four different main spindles are available to match the workpiece, from a bore diameter of ø200mm and spindle speed of 1,500 min- 1 to ø560mm and 350 min-1, respectively, for the best machining with the best spindle. Innovative production is achieved with a rich array of applications, including simultaneous machining with upper and lower turrets, a long boring bar attached to the upper turret and a follower rest mounted on the lower turret.

The range of functions provided with Okuma’s next-generation CNC, the “OSP suite”, supports smart manufacturing with advanced Okuma Intelligent Technologies including the Thermo-Friendly Concept to maintain stable machining accuracies during long runs, Machining Navi for optimal cutting conditions required for turning, milling and threading and the Maintenance suite visual control tool for maintenance activities.

For more information contact F&H Machine Tools – Tel: (011) 397 4050


Turning: Colchester Multiturn CNC Lathe

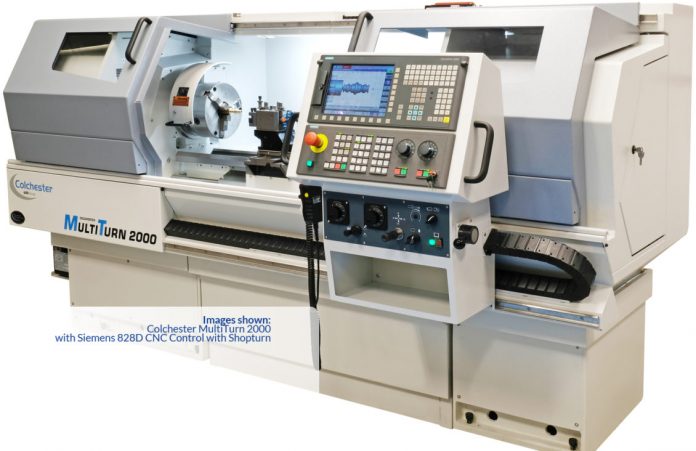
The MultiTurn takes a highly established, robustly engineered lathe concept from Colchester that makes it the perfect machine for many of today’s CNC turning applications.

The MultiTurn is everything that you come to expect from a Colchester lathe – robust, stable and highly precise, irrespective of the component size handled. The Siemens 828D control with Shopturn has a well-earned reputation for being highly user-friendly and intuitive, ensuring that operators can cut quickly and easily with very little training. However, the Shopturn system is also powerful enough for more advanced CNC users to output maximum productivity quickly.

The Colchester MultiTurn lathe has been designed specifically for CNC users looking for increased versatility on one-off and small batch production, first time CNC buyers and jobbing shops looking for real programming simplicity and education and training establishments needing a real lathe with step-by-step simplicity.

600 UK offer 6 Colchester MultiTurn models, starting with the compact MultiTurn 1000, which has a 330mm swing over bed, a 7.5kW motor, outputting spindle speeds of 3500 rpm, right through to the heavyweight MultiTurn 6000, which has a massive 760mm swing over bed and an 18.5kW motor giving spindle speeds of up to 1400 rpm.

The MultiTurn 6000 also has bed length options ranging from 1.5 to 6 metres, ensuring that the MultiTurn is capable of turning any component, regardless of size, right through to long shafts, billets, bar stock and castings.

For more information contact F&H Machine Tools – Tel: (011) 397 4050


Turning: Multi-Spindle Automatic Lathes For Swisstype Machining

The MULTISPRINT 25 and MULTISPRINT 36 set a new standard in series production with six spindles.

Each spindle position already has a Y-axis in the standard. On the basis of countless technology studies and a wide range of customer requirements, the developers have fulfilled the requirements for reducing throughput times and setup times, lowering the cost of process development and integration and also dealing with the increasing degree of complexity. Nozzles in fluid technology, implants in dental technology and shafts in car construction are just three examples of complex components which can be manufactured in a highly productive way on the versatile machines. The result is a manufacturing solution for scalable requirements from series production startup to series production itself.

With the new multi-spindle automatic lathes, DMG MORI has developed a highly flexible machine concept which productively manufactures complex turned and milled parts in both chuck and bar machining.

The bar capacity is a diameter of 25mm with the MULTISPRINT 25 and 36mm in the MULTISPRINT 36. The cross-slides on the six spindles (optionally up to eight) all have a Y-axis with travel distance of 100mm and an X-axis with travel distance of 50mm. The Z-axis travel distances are 100m in the standard version, and 180m in combination with the SWISSTYPEkit. With this, the MULTISPRINT machines can be converted from a short automatic lathe to a long automatic lathe in less than two hours. The maximum turning speed is 7500 rpm.

The MULTISPRINT 25 and MULTISPRINT 36 can manufacture even extremely complex workpieces effortlessly because of their up to 28 tools. Up to 24 driven tools can be used. The speeds go up to 13,800 rpm or maximum torque of 14.2 Nm.

For rear machining the MULTISPRINT machines can be optionally equipped with a pick-up spindle or one or two counter-spindles. The cycle times can be reduced by up to 35 percent in this way. The pick-up spindle move 230mm along the Z-axis. The one or two counter-spindles move 280mm along the X-axis, 320mm along the Y-axis and 370mm along the Z-axis. A double tool station with three driven and two fixed tools completes the scope of the equipment. Demanding off-centre machining is also possible. The indexing of the counter-spindles is a highprecision 0.002° in both configurations.

On the automation front the MULTISPRINT machines can be equipped with a bar loader. DMG MORI has developed its own bar loader especially for the new MULTISPRINT machines. Up to two robots can be used directly in the work area for machining chuck components. These take care of simultaneous loading and unloading and the turning of chuck components with diameters of up to 50 x 80mm.

For more information contact Retecon – Tel: (011) 976 8600


Turning: The Completion Of The CLX Range – Now Also With Fanuc

The CLX 550 universal turning centre from DMG MORI impresses with its high level of stability, sturdy construction, a powerful 630-Nm spindle and a multitude of customer-orientated hardware and software options.

In addition to Siemens the FANUC I series is now also available as a new and additional 3D control alternative. The CLX series represents the segment of high-performance universal machines with a diverse choice of options within the product range of universal turning centres from DMG MORI. The CLX series is a modular solution offer for many different branches – including the automotive industry or general machinery and plant engineering. The new CLX 550 now joins the CLX 350 and CLX 450 to expand the spectrum of successful universal turning centres. With a 480mm turning diameter and 1,225mm turning length it offers users a larger work area on a compact footprint (7.4 m²). The sturdy cast-iron bed with its innovate design ensures the necessary rigidity, optimum vibration behaviour and improved chip fall. Powerful DMG MORI spindles and a VDI40 turret with twelve stations guarantee a high level of productivity. An extensive portfolio of technology solutions, DMG MORI software solutions and applications round off the offer of the high-performance CLX 550.

Its sturdy machine bed, large ball screws and the equally sturdy spindle bearing make the CLX 550 a flexible all-rounder through to heavy-duty machining with a torque of up to 630 Nm in the DMG MORI portfolio of universal turning centres. There is also a 280 Nm counter-spindle available that enables the 6-sided complete machining of complex workpieces. This new and now largest model in the CLX series enables bar machining with diameters of up to 80 mm (ø 102mm as an option) with a high degree of accuracy (circular precision: < 3 μm). In its standard version the CLX 550 comes equipped with a VDI40 turret with twelve tool stations and six block tool holders.

Diverse options enable application-oriented equipping and upgrading of the CLX 550. In addition to the larger bar capacity and lower spindle there are also VDI30 or VDI50 turrets available as well as a tailstock and a steady rest. Both can be ordered alternatively as CNC controlled units. This means the manufacture of crankshafts is also possible on the CLX 550. DMG MORI underscores the high demand on machining quality with versatile equipment options such as direct path measuring systems and integrated workpiece measurement. Altogether the customer has a choice of over 100 hardware and software options which enable individual CLX machine configurations.

Completely new is the 3D control strategy for the CLX: In its standard version the 19″ DMG MORI SLIMline multi-touch control panel with SIEMENS 840D solutionline and Operate 4.7 ensures a high level of user comfort and reliable machining processes. In addition to this the FANUC I-series CNC is now also available as an option for all CLX machines. All machines with FANUC are built in the traditional plant GRAZIANO in Tortona, Italy.

Dr. Michael Budt, CSO for the DMG MORI plants in Poland and Russia, explains, “the decision to produce the CLX machines in Italy as well as in our plant in Poland means we can meet the enormous demand and also come a step closer to achieving our goal of selling up to 3,000 CLX / CMX machines worldwide in future.”

DMG MORI Technology Cycles, such as Easy Tool Monitoring, are also available in addition to the diversity of 3D control. These cycles boost machining efficiency and so of course customer benefit as well. Easy Tool Monitoring, for example, prevents damage by controlled stopping of spindles and axes in the case of broken or overloaded tools.

For more information contact Retecon – Tel: (011) 976 8600


Turning: Universal Turning In The High-Performance Class

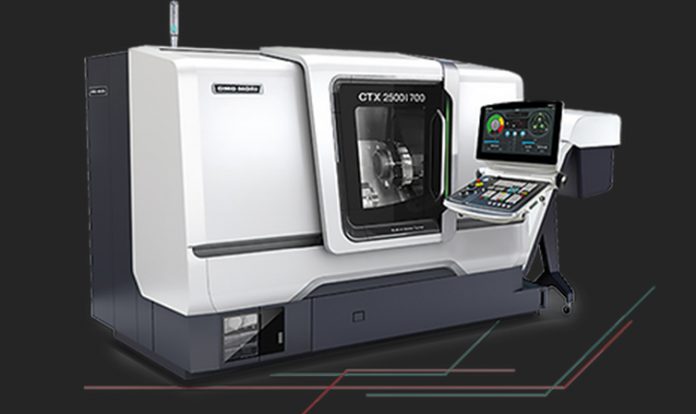
With its robust and rigid construction, the CTX 2500|700 offers the perfect basis for powerful heavy-duty machining combined with high surface qualities.

The machine design was developed using FEM analysis. Robust guides in all axes ensure dynamic rigidity – the rapid traverses achieve up to 30 m/min – as well high vibration damping. Large-scale ball screw spindles as well as 4-fold bearing of the spindle motors result in up to 50 percent higher overall rigidity compared with its predecessor.

DMG MORI combines the rigidity of the CTX 2500|700 with high thermostability. A spiralshaped oil jacket fitted around the spindle unit controls the temperature increase. Also in the circulating coolant of the cast components, which minimizes displacements and is just 2.0 μm. The incremental length measuring system from MAGNESCALE, with a standard resolution of 0.01 μm, underscores this mark of quality.

When it comes to performance, the CTX 2500|700 excels with its turnMASTER main spindles. A 10″ model with 4,000 rpm, 26 kW and 525 Nm and optionally a 12″ model with 3,500 rpm, 30 kW and 1194 Nm are available. The counter spindle is 6″ as the standard model and achieves 7,000 rpm, up to 11 kW as well as 70 Nm. An 8″ spindle with 5,000 rpm, 32 kW and 360 Nm is offered as an option here.

The precision disk turret with active disk cooling and VDI-40 interface is the standard of the MC models and Y models with an additional Y-axis. The rotational speed is 6,000 rpm. The torque achieves a maximum of 32 Nm. The SY expansion stage with counter spindle is equipped with the 6,000 rpm star turret torqueDRIVE with up to 85 Nm torque as standard. The BTM interface is available as an option. The speedDRIVE turret with 12,000 rpm and 56 Nm is also available. All turrets offer space for either 12 or 16 tools in the optional VDI 30 design (not for torqueDRIVE).

With ø 366mm turning diameter and 705mm turning length in the case of the CTX 2500|700k, the new turning centre offers enough space for a broad range of tools. The chuck size for the standard model is 250mm with a bar capacity of 76mm. The travel paths in the X-, Y- and Z-axis are 260 x 100 x 795mm.

The ergonomic design of the CTX 2500|700 makes the work area easily accessible, which also enables crane loading of heavy components from the top. A pocket for long tools is built into the wall of the spindle gear box to prevent collisions. The oil cooler and hydraulic unit are mounted at the rear and easily accessible.

The user friendliness of the operating system offered by the turning centre is continued in the control system. A ERGOline Control with 21.5″ multi-touch screen and CELOS with SIEMENS inclusive ShopTurn 3G are put to work here. CELOS enables integral administration, documentation and job planning in work preparation and workshop on the one hand and on the other, CELOS APPs, such as the condition analyzer or performance monitor, offer our customers a detailed insight into the machining processes and the status of the machines as the basis of a continuous improvement process. Moreover, CELOS functions to an ever-greater extent as an IoT interface and creates the basis for cross-company interaction in the production networks of the future.

A topic for the future is automation. DMG MORI offers a flexible connection to various automation solutions for the CTX 2500. In addition to integrated tool unloading, a bar loader connection and the option of using the Robo2Go, DMG MORI has now taken over the GC gantry loaders from the NLX series.


For more information contact Retecon – Tel: (011) 976 8600


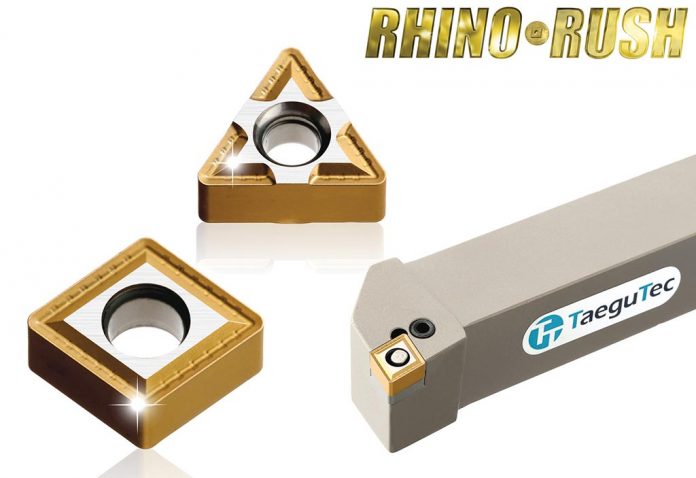
Turning: FS And MK RhinoRush Chip Breakers

The RhinoRush MK chip breaker is ideal for medium applications while machining stainless steel and heat resistant materials.

The MK chip breaker is a more stable insert that offers long tool life because of its sharp edge design that minimizes built-up-edges during machining operations.

Case studies prove the effectiveness of the MK chip breaker with tool life being increased by over 300 percent.

For example, during the product testing phase of a workpiece made from SUS 304, the MK chip breaker coated with TaeguTec’s TT9080 grade witnessed an increase of tool life by 343 percent during continuous cutting conditions with speeds of 160 meters per minute and same cutting conditions.

During another continuous cutting test, on difficult-to-cut Inconel 718, tool life was increased by 159 percent with all cutting parameters the same.

The RhinoRush FS chip breaker is specifically designed for excellent chip control on steel finish turning with superior evacuation under low feed and low depth of cut applications, while the insert’s sharp cutting edge drastically reduces machining load resulting in minimal vibration during operations.

For more information contact TaeguTec – Tel: (011) 362 1500