Home Blog Page 52

TRUMPF is Expanding the Scope of 3D Printing EMO Hannover 2019

TRUMPF has printed a mount to hold microwave filters for the German communications satellite Heinrich Hertz, reducing its weight by 55 percent in the process. Source: TRUMPF, GettyImages, TurboSquid

TRUMPF will show how 3D printing can drive advances in various industrial sectors with a showcase at EMO Hannover.

Additive manufacturing processes enable the creation of unprecedented complex shapes that are both light and stable. With the benefit of digital connectivity, they fit seamlessly into state-of-the-art manufacturing systems in use today. The 3D printer is a key tool for many manufacturing processes ranging from mass customization to one-off builds. It can print anything from bespoke facial implants to special parts for cars or airplanes. Able to print components in one piece, these systems often spare vendors the effort of multiple manufacturing steps. “Interest in additive manufacturing technologies remains high because the process’s benefits are proving their merits in more and more practical applications. This applies as much to conventional metalworking companies as it does to future products in the aerospace industry,” says Thomas Fehn, general manager at TRUMPF Additive Manufacturing. TRUMPF is one of the few providers of 3D printers to develop its own lasers, the most important component of the machine. This enables the company to rapidly branch out into new applications and continuously improve the process. For example, TRUMPF recently printed copper and gold with a green laser for the first time. The jewelry and electronics industries stand to benefit from this promising innovation.

Personalized craniomaxillofacial implants

Russian medical device manufacturer CONMET has been using a TRUMPF 3D printer to produce craniomaxillofacial implants since early 2018. Creating implants for use in surgery has been a stressful business until now. The surgeon has to cut the craniomaxillofacial implant out of a perforated titanium plate during the procedure and then shape it to size. This is a taxing task where the time pressure can have a negative impact on the quality of fit. Such procedures are much easier with a 3D-printed implant. First, the hospital determines the patient’s data and sends it to CONMET.

This 3D-printed nozzle for USB Düsen’s sewer cleaning system was optimized by TRUMPF.

Its engineers draw on this data to create a CAD model and design the implant in consultation with the surgeon. Then the 3D printer can go to work. The implant is ready for insertion, precisely fitted and cleaned, before the procedure begins. This enhances patient safety while cutting costs and speeding up surgery. The system makes light work of the kind of complex topologies that implants often require. What is more, it can print parts that are sturdy and durable while still cushioning against blows. The implant’s porous structures facilitate the ingrowth of healthy tissue. Prices also come down as additive manufacturing only uses as much material as the implant actually needs. CONMET has managed to reduce the cost of manufacturing craniomaxillofacial implants by around 40 percent. The company is planning to step up mass manufacturing of implants with TRUMPF 3D printers and add more machines to its inventory.

A lightweight mounting bracket for communication satellites

TRUMPF has been commissioned by the space company Tesat-Spaceroom to produce a 3D-printed mounting structure for Germany’s Heinrich Hertz communications satellite, which will be used to test the space-worthiness of new communication technologies. The mount holds strap-on motors serving to control microwave filters. In collaboration with the company AMendate, TRUMPF engineers succeeded in optimizing the geometry of the mounting structure and reducing its weight by 55 percent. It now weighs just 75 grams instead of 164 grams. “This is just one example of how we can use additive processes in satellite construction to reduce weight and increase payload capacity,” says Matthias Müller, industry manager for aerospace and energy at TRUMPF Additive Manufacturing.

Thomas Fehn is general manager sales, marketing & finance at TRUMPF Additive Manufacturing. Source: TRUMPF

The experts printed the redesigned part on TRUMPF’s TruPrint 3000 3D printer. The new geometry cannot be produced by conventional means. This optimized mount is both lighter and more robust. During the launch of the satellite the new mounting structure will withstand the same high forces and will hold its shape better.


Easy-to-make sewer cleaning nozzles

TRUMPF joined forces with USB Düsen and Heilbronn University of Applied Sciences to demonstrate the benefits of 3D printing in the fabrication of cleaning nozzles for sewers. These nozzles are mounted on the head of cleaning bombs that slide down channels on carriages, spraying jets of water at 300 bar pressure to dislodge sludge in larger sewer lines. Although the nozzles’ design is simple, it stills takes workers four steps to make these components.

Medical device manufacturer CONMET uses a TRUMPF 3D printer to produce craniomaxillofacial implants for the CIS market.

First, they have to cut the raw material, then thread it on a lathe, mill out a nut and finally glue in a ceramic base. The worker has to constantly move from one machine to the next and gluing often leaves imperfections. The 3D-printed variant eliminates the need for milling and gluing. The component can be printed without any supporting structures, so there is no finishing work to be done afterwards. The software- driven process is far more accurate than manual gluing. Measurements have shown that printing cuts production time by 53 percent. For the first time, this will allow up to 10,000 parts to be manufactured per year, while another benefit is a smoother flowing jet of water.

New Dimension in Networked Production

Dr. Alexander Broos, umati project manager and Head of Research and Technology at the EMO organizer VDW.

umati – universal machine tool interface goes live at EMO Hannover 2019 from 16 to 21 September with an exciting presentation. “Around 50 machine tool manufacturers from all over the world will be joining forces to show how umati makes machine data usable,” says Dr. Alexander Broos, umati project manager and Head of Research and Technology at the EMO organizer VDW (German Machine Tool Builders’ Association). Trade show visitors will experience live the benefits the standardized interface offers.

“umati represents a quantum leap in the implementation of Industry 4.0 in production,” explains Broos. “The use of a standardized interface will give machine tool users and their customers a whole new dimension of benefits,” he continues. The networking of machines, systems and software is one of the most important trends in manufacturing right now. Today’s customers expect to be able to integrate new machines into their own IT ecosystems with no difficulty. umati does this on the basis of the international interoperability standard OPC UA – easily, quickly and securely.

This sticker on a machine indicates that it is connected via umati. The data can be tracked live in a central dashboard by scanning the QR code. Picture VDW

For over two years, a team of various machine tool manufacturers – today’s core partners – have been working on developing this uniform language for machine tools. Together with control manufacturers, they aimed at making its use as userfriendly as possible. “The concept is so impressive that many international manufacturers, but also various associations and scientific institutions, have signalled an interest in participating in umati,” reports Broos.

More than 50 companies from seven countries demonstrating umati in Hannover

More than 50 companies from seven countries have currently registered for EMO Hannover, which will connect machines or value-added services as part of the live demonstration. Those are from Germany Adamos, Alfred H. Schütte, Axoom, Chiron-Werke*, DMG Mori*, DVS Technology Group, Elha- Maschinenbau Liemke, Emag*, Gebr. Heller Maschinenfabrik*, Grob-Werke*, Heinrich Georg Maschinenfabrik, Index-Werke, IT Engineering Software Innovations, K.R. Pfiffner*, Kapp, Liebherr-Verzahntechnik*, MAG-IAS, Maschinenfabrik Berthold Hermle, Peiseler, Profiroll Technologies, Röders, Sauter Feinmechanik, Symmedia, Trumpf Werkzeugmaschinen*, Leibniz University of Hanover – Institute of Manufacturing Technology and Machine Tools, Vollmer Werke; from Italy Guiseppe Giana; Orchestra; from Japan Citizen Machinery, Makino Milling Machine, Murata Machinery, Okuma Corporation, Toshiba Machine and Yamazaki Mazak: from Austria: Emco Maier; from Switzerland Agathon, GF Machining Solutions*, Precitrame, Tornos, United Grinding Group*; from Spain Danobat, Ibarmina Innovatek, Nicolas Correa, Soraluce, Zayer; from Taiwan: Buffalo Machinery, Leadyang Precision Technology, Selica International (*core partners).

All umati partners at EMO Hannover can be recognized by this logo. Picture VDW

The participants are supported by the most important control suppliers, which partly also connect machines or added value services at their booths: B&R Automation, Beckhoff Automation, Bosch Rexroth, Fagor Automation, Fanuc, Heidenhain, Mitsubishi Electric and Siemens. The demonstration is realized in cooperation with T-Systems, who provides a data hub to connect machines and services.

“We assume that this already impressive list of companies will be considerably extended before the fair,” says Broos. Interested parties can find out about the current number of participants at any time on the Internet at www.umati.info.

umati activities at EMO Hannover

The participants will be connected to a central dashboard. Furthermore, 18 software and data evaluation service providers will also be demonstrating how this data can then be used to generate added value for customers. Visitors can pick up information at the booths of the affiliated partners as well as at the central umati information booth in Hall 9, E24. This is where the data from the connected machines merges. Twice a day, at 10:30 and 14:30, the umati project team will invite visitors to Meet the Experts at the booth, where representatives of the core partners will report on their involvement in the project group and discuss various issues with the audience. Together with the OPC Foundation, the VDW is organizing a focus topic on OPC UA in manufacturing technology on Tuesday 17 September 2019 in the Forum New Technologies, also in Hall 9. This will be rounded off with a Get Connected Event on the exhibition stand. On Friday 20 September 2019, the Forum New Technologies will also be devoted to umati.

Author: Dag Heidecker, daxTR – Technik + Redaktion, Wermelskirchen (near Cologne)

Cobots Successful Collaboration Between Man and Robot

The more closely man and machine can collaborate, the more efficient robot applications will become. Photo: BMW Group

Robotics and automation are among the key technologies for ensuring lasting international success. Cobots interact directly with humans and give manufacturing companies a competitive edge in the market. At EMO Hannover 2019, trade visitors will find countless automation solutions and collaborative robots aimed at enhancing productivity.

Automation and digitalization can be used to make manufacturing processes more efficient. Of particular interest here are cobots. These collaborative industrial robots work together with humans – without special protective measures such as fences or demarcated areas. In which processes are cobots already being used? How can collisions and any resulting risk of injury be avoided? Robotics manufacturers, suppliers of various peripheral components for automation solutions, as well as safety and scientific experts will be providing an overview of the current situation and giving forecasts for future developments.

Making working life easier – and more ergonomic

“Humans are indispensable for intelligent production,” says Jochen Vetter, Manager of Robot Safety at Pilz. “Robots can perform physically demanding or repetitive activities, leaving the humans to take care of more sophisticated tasks. Automation can thus also provide a response to the demographic shift.” Different validation methods have to be applied to human-robot collaboration (HRC). For example, it is imperative that measurements are taken to determine the safety risks involved in any possible collisions. Pilz has developed its own method for this. A system measures the forces acting on the human body and compares them with the ISO/TS 15066 limit values for collaborative robots.

“The challenge is to eliminate any boundaries between the working areas of humans and machines. In addition to the dangers posed by the robot, human movements must also be taken into account,” says the robotics safety expert. “The speed of these is not always predictable, nor are human reflexes or the sudden arrival of other people.

Schunk automation specialists are aiming to provide robot manufacturers and integrators with independently tested co-act grippers. Photo: Schunk

“Collisions, however, should never result in injury.” These must be prevented by the use of more reliable control systems and intelligent, dynamic sensors built into the robot. In addition, it is important to set reliable safety standards based on normative principles.

“The interaction will develop organically, for example in terms of language and gestures,” Vetter is convinced. “This will take HRC to a new quality level for a different category of actions. In addition, HRC solutions will in future be linked to the factory control system via OPC UA or Industry 4.0 RAMI standards. Potential areas of application lie not in largeseries production, but in the manufacture of medium and small series. HRC makes sense in situations where employees can be relieved – ergonomically – of physically strenuous tasks, such as in maintenance work.”

Gripping workpieces of up to 8 kg using safety intelligence

“The biomechanical limits specified by ISO/ TS 15066 have so far restricted the use of cobots to the handling of small parts, for example in assembly applications in the electronics industry or in the pick & placing of housings, turned and milled parts, etc.,” says Prof. Markus Glück, Managing Director of Research & Development, Chief Innovation Officer at Schunk. “Our EGL-C long-stroke gripper, however, allows a new scale of components to be manipulated. For the first time it is possible to handle workpieces up to 8 kg safely with form-fit gripping. This opens up great potential, including for machine tools or in assembly.” Thanks to integrated safety intelligence, the Co-act (collaborative actuator) EGL-C has succeeded in achieving gripping forces of up to 450 N in collaborative applications. This is around three times greater than before and represents a world first – and is also on show at EMO Hannover 2019. “HRC will radically change the world of work,” predicts Glück. “The focus is on improving the ergonomics, creating more flexible work processes, increasing efficiency and optimizing processes. Intelligent gripper systems will permit higher component weights to be handled in the future. In addition, 24V technology will enable them to be deployed on mobile platforms which will gain in importance as a result. There is also great potential for the use of lightweight robots to assist in assembly.”

A new era in machine tool charging

Division Manager Peter Pühringer with the new six-axis generation of TX2 robots, also on show at EMO Hannover 2019. Photo: Stäubli Robotics

“Collaborative and mobile robot systems offer new possibilities for the automation of machine tools. For the first time, automation can break out of its rigid constraints and achieve unprecedented levels of flexibility and productivity thanks to innovative robotic solutions,” reports Peter Pühringer, Division Manager at Stäubli Robotics. In order to maximise this flexibility, Stäubli has designed its new six-axis TX2 generation for universal use. The robots in the new version can collaborate directly with humans. They are also available as mobile and collaborative robot systems. “This heralds a new era in machine tool charging,” states Pühringer. The robots work both in stand-alone operation and directly with machine operators. Mobile versions of the robot can easily link different machine tools together and take care of the complete workflow in an Industry 4.0 environment. “This unbelievable flexibility allows completely new, digitally networked production processes to be created,” says Pühringer. “These will significantly increase productivity and give innovative enterprises an unprecedented competitive edge.

Sensors help avoid possible collisions

Human-robot collaboration (HRC) must rule out the possiblity of injury in the event of a collision. Photo Dag Heidecker

A crucial and topical issue is how the CE process is handled when robots are used at different stations. Photo: Bernd Müller

“At present, cobots are frequently used for simple handling processes, such as charging machines. Although there is often no safety fence, they are equipped with additional safety features and are not generally used for direct human-robot collaboration,” says Prof. Gunther Reinhart, holder of the Chair of Industrial Management and Assembly Technology at the iwb (Institute for Machine Tools and Industrial Management) at the Technical  University of Munich. “Work is currently focussing on HRC planning support, on safety and also on instructing the robots. Safety-related innovations are aimed at detecting possible collisions in advance through the use of different types of sensors – such as capacitive or ultrasonic sensors – or cameras.” The Institute for Machine Tools and Industrial Management will be on hand at EMO Hannover 2019 to provide further information to trade visitors.”

Author: Dag Heidecker, daxTR – Technik + Redaktion, Wermelskirchen (near Cologne)

New Threading Tools with Coolant Channels

ISCAR is expanding the range of square shank threading tools by adding SER/ L-JHP tools with channels for high pressure coolant.

The use of high pressure coolant is growing as manufacturers seek ways to reduce cutting time, improve machining process reliability and achieve longer tool life. ISCAR’s new JHP tools with coolant channels provide all of these advantages. High-pressure coolant lowers temperature at the cutting zone and reduces – or even eliminates – built-up edge phenomenon, especially when machining stainless steel and high-temperature alloys.

Shorter chips are easily managed, as they do not tangle around the work piece or machine parts and so there is no need to stop the process frequently. With conventional cooling, the chips usually prevent the coolant from reaching the insert rake face in the cutting zone. However, the JHP tools coolant stream is directed precisely between the insert rake face and the flowing chips, which results in a much more reliable process as well as an improved surface finish and longer tool life.

With a growing demand for JHP tools, ISCAR has introduced new TTADR/L-JHP threading adapters with high pressure coolant channels carrying TTG DECAIQTHREAD 10-cornered inserts. The adapters are designed for use with standard MODULAR-GRIP MAH…- JHP holders.

For more information, please contact Iscar South Africa – Tel: 011 997-2700.

Harp Waytrain Horizontal Bandsaw

Harp Waytrain Horizontal Bandsaw, Model 330A.

Harp Waytrain horizontal bandsaws are manufactured in Taiwan. The company was established in 1983, and is well known for producing high quality machines. Sizes range from 180mm diameter cutting capacity, up to 330mm diameter. Rigidly constructed, with great attention to detail, these saws are ideal for all engineering companies. Harp Waytrain horizontal bandsaws combine quality, reliability and affordability. Five models are available ex-stock, such as the UE-712A, UE916A, UE-250, UE918S and the UE-330. All machines are complete with coolant systems, blade tension control and electrics 380V/3/60.

Features:

Model 330A: Capacity 90° round 330mm, rectangle 330mm x 480mm / 225mm x 530mm, capacity 45° round 255mm, rectangle 280mm x 255mm, blade size 34mm x 1.1mm x 4100mm, blade speeds (belt change) 28/40/56/78 mpm, motor 3 hp, net weight 600kg, tool box, material stopper, machine manual.

Model 250A: Capacity 90° round 250mm, rectangle 250mm x 415mm / 200mm x 450mm, capacity 45° round 190mm, rectangle 250mm x 190mm, blade size 27mm x 0.9mm x 3300mm, blade speeds step pulley 25-71 mpm, motor 2 hp, net weight 320kg, tool box, material stopper, blade speeds (belt) machine manual.

Model 918S: Capacity 90° round 225mm, rectangle 225mm x 430mm, capacity 45° round 225mm, rectangle 225mm x 295mm, blade size 27mm x 0.9mm x 3345mm, blade speeds (belt change) 82~259 mpm, motor 2 hp, net weight 420kg, swivelling saw-bow, variable speed, machine manual.

Model 916A: Capacity 90° round 225mm, rectangle 225mm x 340mm, capacity 45° round 165mm, rectangle 225mm x 165mm, blade size 27mm x 0.9mm x 3035mm, blade speeds (belt change) 25/40/51/71 mpm – motor 1½ hp, net weight 300kg, tool box, material stopper, machine manual.

Model 712A1: Capacity 90° round 180mm, rectangle 180mm x 280mm / 65mm x 300mm, capacity 45° round 110mm, rectangle 180mm x 110mm, blade size 19mm x 0.9mm x 2360mm, blade speeds (belt change) 23/33/45/65 mpm, motor 1 hp, net weight 130kg, tool box, material stopper, machine manual.

For more information, please contact Harp Machine Tools – Tel: (011) 918-5138.

Cutting-edge Bandsaw Technology – Amada

The history of Amada cutting-edge bandsaw technology dates back to 1946; ever since our goals have been to provide customers with increased productivity and reliability. While technology evolved, we embraced CNC automation as a core strength, thus improving throughput. Today we are uniquely positioned to help customers expand production capabilities and growing their business.

No two customers’ needs are exactly alike. Finding the right solution means thoroughly understanding objectives and configuring a solution that matches them precisely. Our engineers have decades of industry experience which promote achieving specified goals with a process that fits and enhances a customer’s work flow.

From the early beginnings of bandsaw machinery produced by Amada, (many of which are still running today), Amada has strived to offer machines that not only meet customers’ needs, but exceed them by offering features that were once considered impossible.

The technology of the bandsaw demonstrates the ability and limitations of the blade. As blades advance in technology, so do the machines utilizing them. Amada, as a proud manufacturer of both the machines and the blades, continues to research these developments and incorporates customer feedback to produce constantly evolving solutions.

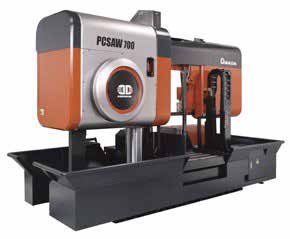
Amada supplies bandsaw machinery and blades, such as the HK / HD series for mitre cutting, the semi-automatic H series, fully automatic HA / HFA series and the VM vertical series. The latest bandsaw technology is reflected in models such as the Dynasaw 430, the PCSAW with pulse cutting technology and CMB high speed circular saws.

Some features include out of square cutting detection, motion detectors to monitor the blade for jamming or breakage while cutting and quick approach arms. Add to this no work limit switches and work lights, hydraulic blade tensioning, variable blade speed control, vice pressure control units and positively driven wire brushes. 9 times feed for cutting long lengths and cut-off counters ensure the correct number of cuts. All these features, assist semi-skilled workers in the operation of the machines.

Certain models can be left to run unmanned on larger batch runs, thus allowing staff to do other important jobs at the same time. Take-up conveyors and tripod stands are available making material handling simple during the loading and cutting process.

Models available start with the entry level of 250mm capacity, which are highly popular and favourably priced. With larger steel suppliers all utilizing Amada bandsaws daily, testimony is given to their accuracy, reliability and longevity. Cutting accuracies are obtained right down to 0,2mm. With such accuracies, the need for secondary machining processes is greatly reduced and in some cases eliminated.

The latest additions to the Amada bandsaw range is the PCSAW, with either single pulse cutting action or double pulse cutting action. The PCSAW series is designed to offer high cutting rates, high precision, low noise and long blade life.
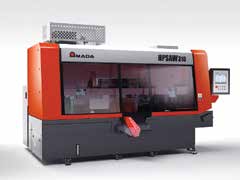
Vibration has always been an unwanted characteristic of metal sawing when cutting too fast. It leads to decreased blade life, noise and uneven or inaccurate cutting. By introducing a controlled pulsating motion to the blade through either an induction motor or a servo motor, all unwanted vibrations are eliminated and most efficient metal cutting is achieved. Blade temperature is reduced considerably during the process, and this together with positive chip removal through a twin wire brush system and a large area chip conveyor all enhance blade life and reduce running costs. All PCSAW bandsaws are operated through the on-board userfriendly CNC control.

The HPSaw (High Performance Saw) is possibly the fastest bandsaw in its class with the latest in cutting speed innovation and the ability to cut at up to 1.5 times faster than the high speed circular saws.
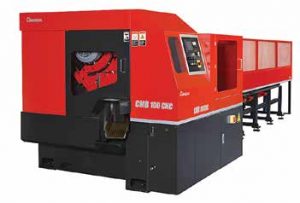
The specially designed AXCELA HP1 blade for this machine also reduces material wastage by up to 60% and guarantees accurate cutting.

Circular sawing machines are the optimal technology for realizing reduction in cycle time and high-precision cutting needed for steel bar cutting at high speed. An automatic loading table for continued cutting operation is supported by a CNC powered cut-in control for ease of operation. In perfecting functionality of these machines, Amada has developed a unique carbide tip circular blade that cuts cleanly, generating virtually no burrs.

A full range of bi-metal bandsaw blades are produced by Amada to compliment machine technology. As mentioned previously, a bandsaw demonstrates the ability and limitations of a blade. This means that a machine is only as good as the blade being used. Amada blades have earned the reputation of extreme reliability and longevity. All blades are manufactured in Japan to the most stringent quality standards and utilizing the latest in electron beam welding methods. These measures ensure that premature blade breakage is almost unheard of. The comprehensive range of blades available is tailormade for all types of cutting conditions on all types of steels and profiles.

Robustness of Amada machinery, combined with longevity of Amada blades and a highly dedicated backup policy provide Amada customers, with total peace of mind.

– By Barry Page

For more information, please contact Amada – Tel: 011 453-5459.

Everising Fully Automatic Bandsaws

Everising’s S-250HB – S 460HB range of bandsaws features full PLC control of all electrical and hydraulic functions.

Everising has four pivot-type bandsaws in its S-250HB – S 460HB range. The bandsaws feature full PLC control of all electrical and hydraulic functions. The raising and lowering of the cutting head is controlled by a single lifting cylinder which makes for quick, efficient operation. Workpieces are secured during cutting by a hydraulically controlled dual-vice clamping system.

Blade tension, a factor that can extend the life of a blade, on Everising’s S machines is controlled hydraulically for optimal blade life. Blade speed is controlled by an inverter giving infinitely variable speeds of between 20 to 100 m/min. The machines also feature automatic shuttletype feeding systems.

A pre-set counter shuts off the S Series bandsaws after a given number of items have been cut, while an idler-wheel motiondetector shuts down the machine should the blade stall or break. In addition, the saws detect when stock has run out and automatically shut down.

In its column type H Series bandsaw range, Everising offers 11 different models. These range from the H-250HA with a 250mm cutting capacity to the large H-1100HANC capable of cutting workpieces of 1000mm x 1100mm dimension. The machines at the larger end of the range have progressively more features, such as the ability to use tungsten-carbide tipped blades. However, all of the H series bandsaws are well-suited for heavy duty cutting applications as their column type design allows for maximum cutting stability.

Should the blade on an H series machine break, the machine will automatically shut down to protect both the operator and the machine. The bandsaws are fitted with automatic chip conveyors which keep the inside of the machine clean and save on operator time. In terms of the operator’s time, the H series are fitted with user-friendly NC touchscreen controls with a self-diagnostic control system. As with the S series, the H series’ hydraulic system and electrical devices are controlled by PLC.

Everising’s H series bandsaws are well-suited for heavy duty cutting applications as their column-type design allows for maximum cutting stability.

When there is need to cut bundles of steel rod, on the H series S-250B to the H-460 HB models, a hold-down device ensures that the material being cut stays secure in the machine thereby offering consistent quality. For larger workpieces, the bandsaws in the H series are equipped with a hydraulic full-stroke, dualvice clamping system.

For machines capable of cutting diameters greater than 700mm, the guide arm travels on linear guideways for greater stability during cutting. On the larger H Series models, an anti-vibration roller not only eliminates vibration but extends blade life as well. The antivibration roller and the saw blade clamp are automatically adjusted.

Optional H-Series devices feature an out-of-square detection system which automatically shuts the machine down while adjusting dual wire blade cleaning brushes which also serve to extend blade life. Everising’s automated functions allow for a minimum of skilled supervision allowing workers to be deployed to more productive activities.

For more information, please contact First Cut – Tel: 011 614-1112.

More Options for the Workshop

Depending on requirement, users can choose between manually operated, semi and fully automatic variants – and of late, also between different cutting ranges. To achieve this, KASTO is extending the range by three further models.

The KASTOmicut is designed for cutting tubes, sections and solid materials to length and for mitre cutting. Workshop operators benefit particularly from the high cutting accuracy and quality with different materials and the attractive price-performance ratio of the saws. In 2016, KASTO presented the first models of the new series with a cutting range of 260mm for round material and 310 x 260mm for flat material. Users can choose between the manually operated base model KASTOmicut P 2.6, the KASTOmicut E 2.6 with hydraulically controlled saw feed, the semi-automatic KASTOmicut U 2.6 with hydraulic material clamping and the fully automatic variant, the KASTOmicut A 2.6. With its intelligent accessories, this enables efficient, extensively unattended operation.

Newly incorporated into the portfolio, KASTO now has two models with a larger cutting range: Die KASTOmicut E 4.6 saws round material up to 335mm diameter and flat KASTO HIGHPERFORMANCE BAND SAW REDUCES CUTTING TIMES BY UP TO 50 PERCENT The fully automatic machine is optimised for bimetallic and carbide blades and can be applied in areas such as the steel trade, steel production, forging mills, machine manufacturing and the automotive industry. material with dimensions up to 460 x 335mm. It is specially designed for single-sided mitre angles and is suitable for cuts from 0 to +60 degrees. The saw has a hydraulically controlled feed. Blade and material tensioning is carried out mechanically. The cutting speed can be continuously adjusted between 20 and 110 metres per minute. This opens up a wide range of possibilities for the user with different material qualities.

With the KASTOmicut U 4.6, users can even process flat material up to 520mm wide. With this saw, the material is also clamped by means of a horizontal hydraulic vice. This simplifies handling and increases the output in the case of small batches. The continuously adjustable cutting speed lies between 12 and 150 metres per minute. Like the smaller models of the KASTOmicut range, mitre cuts from -45 to +60 degrees are possible. The mitre angle can also be continuously adjusted. A heavy and torsionally rigid welded structure for the saw frame provides extremely stable support for the saw blade, ensuring excellent cutting quality even with hard-to-machine materials.

KASTO has extended the range with the addition of the KASTOmicut P 1.8. The saw has a cutting range of up to 180mm and is likewise suitable for straight and mitre cuts from 0 to +45 degrees. It features manual material clamping by means of an easy-tooperate and easily adjustable clamping device. The saw blade is also tensioned manually. The feed rate is determined by manually guiding the saw frame and a cutting rail serves as material support. An efficient three-phase motor delivers a drive power of up to 1.5 kW and ensures high cutting quality. Like other models in the KASTOmicut range, the saw also scores with its small dimensions and excellent accessibility. It can be easily picked up by a lift truck or forklift and positioned as needed.

Depending on the design, the shortest possible cutting length is six to ten millimetres and with a remnant piece length of 15 to 30mm for individual cuts, users can make maximum use of the material to be sawn. A highly efficient worm gear mechanism provides top performance and the sophisticated design ensures a constant cutting force for excellent results with all materials.

For more information, please contact Retecon – Tel: 011 976-8600.

KASTO High-Performance Band Saw – Reduces Cutting Times by up to 50 Percent

The metal sawing and storage technology specialist KASTO offers a high-performance band saw, the KASTOwin pro AC 5.6.

Users will appreciate its short cutting times, long tool life and intuitive operation. The fully automatic machine is optimized for bimetallic and carbide blades and can be applied in areas such as the steel trade, steel production, forging mills, machine manufacturing and the automotive industry. Besides helping to reduce tool costs, it significantly increases production speed and efficiency. Depending on the type of blade, cutting times can be reduced by 50 percent and more.

TThe KASTOwin pro AC 5.6 is designed for a wide range of applications and delivers top performance with both carbide and bimetallic saw blades. An important feature is its innovative feed system, which is controlled by means of two ball screw spindles, each with a servo drive for precise, infinitely variable control. The KASTOwin pro also has a retraction unit on each side for lifting the band from the surface when the saw head moves back. This makes for particularly efficient, exact sawing with minimal tool wear.

The KASTOwin pro AC 5.6 is driven by an 11-kilowatt frequency-controlled motor, which provides plenty of capacity for use with carbide blades. The cutting range is 560mm and the smallest dimension to be cut is 25 x 25mm. The shortest residual length is ten millimetres for individual offcuts and 35mm for automatic operation, enabling operators to reduce waste to a minimum. Two electrically driven plastic brushes keep the band free of chips. They are easy to replace and are automatically adjusted throughout their service life. The sawing unit has a heavy, torsionally rigid welded structure with vibration-optimized ribbing, ensuring quiet operation with shorter cutting times and a long tool life.

The KASTOwin pro AC 5.6 also has a powerful coolant pump and a large coolant reservoir so that difficult-to-machine materials can be cut with minimal tool wear. In addition, this fully automatic saw comes with EasyControl, a high-performance control unit.

The fully automatic machine is optimised for bimetallic and carbide blades and can be applied in areas such as the steel trade, steel production, forging mills, machine manufacturing and the automotive industry.

It is easy to use and reduces idle times in automatic operation for maximum cutting performance. All parameters can be optimized to match the type of blade being used.

For more information, please contact Retecon – Tel: 011 976-8600.

The DTI Showcasing SA Companies at Africa Oil Week

The Minister of Trade and Industry, Rob Davies.

The Department of Trade and Industry (the dti) will for the first time be showcasing local companies in the South African National Pavillion at the prestigious Africa Oil Week event, which will take place in Cape Town, from 4-8 November 2019. As the leading event for Africa’s upstream oil and gas sector, the dti will be using Africa Oil Week as a platform to outline the department’s commitments to the energy sector and re-emphasize the need for sustainable and equitable growth for local businesses.

The businesses will also be exposed to more than 1 500 senior executives from the oil and gas value chain across the globe, including 15 ministers of energy, key decision-makers from national and international oil companies, oilfield service providers and the investment community.

The inclusion of the South African Pavilion is aligned with the country’s strategic goal of implementing an outward investment-led trade approach which aims to increase the country’s exporting capacity for diversified goods and services to international markets while promoting industrial development, job creation, foreign direct investment and economic growth to position South Africa as a globally competitive investment destination.

The Minister of Trade and Industry, Dr Rob Davies says the sub-Saharan Africa region is rapidly transforming into a natural gas jurisdiction given major recent natural gas discoveries in the region and the significant potential domestically in South Africa.

“Following the profound experience of reindustrialization of the United States of America on the back of major gas finds and the Qatari LNG development trajectory, the potential for the realization of significant long-term onshore value in South Africa and the region is substantial. Whether or not South Africa discovers its own commercially viable natural gas resources, it will play a major role in driving onshore demand and the development of the regional resources,” says Davies.

He adds that in the light of the opportunities presented in the regional and domestic natural gas sector, the dti continues to refine its long-term natural gas industrialization policy for SA, which would maximize the multiplier effects (both up and downstream) of the natural gas resources domestically and in the South East African region. Appropriate natural gas industrial policy will allow SA and the region to optimize the utilization of natural gas, maximize its multiplier effect potential and drive regional integration.